When it comes to the efficient handling and transportation of food additives in industrial settings, selecting the right conveying method is crucial for maintaining product quality, ensuring safety, and optimizing operational costs. Various technologies are available, each with its own advantages and applications. This article provides a detailed comparison of common food additive conveying methods, highlighting key factors to consider when choosing the most suitable solution for your production needs.
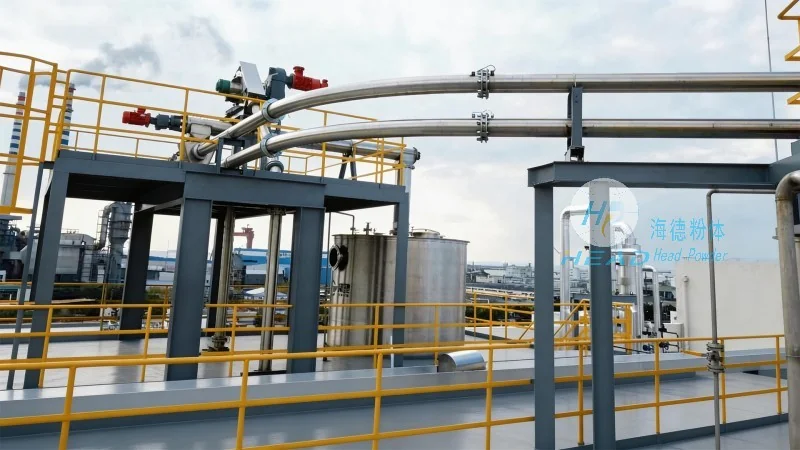
For liquid or semi-liquid food additives, pump-based systems are widely used due to their ability to handle viscous materials and maintain consistent flow rates. These systems typically involve positive displacement pumps or centrifugal pumps, which can be equipped with special seals and materials to prevent contamination and ensure compliance with food safety regulations. The use of pump-based conveyors allows for precise control over the flow rate, pressure, and temperature of the additive, making them ideal for applications where uniformity and cleanliness are paramount. Companies like Shandong HeadPowder Engineering Co., Ltd. specialize in designing and manufacturing custom pump systems tailored to the specific requirements of food additive processing, ensuring reliable and hygienic operation in food production environments.
Solid food additives, such as powders, granules, or small particles, are often transported using screw conveyors. These mechanical devices consist of a rotating screw (or auger) enclosed in a trough, which moves material from one point to another through a continuous, enclosed path. Screw conveyors are particularly effective for handling dry, free-flowing materials and can be designed with stainless steel construction to meet sanitary standards. The design of the screw pitch and diameter can be adjusted to control the speed and direction of material movement, allowing for gentle handling that minimizes product degradation. In industrial applications, screw conveyors are often integrated with other equipment, such as mixers or storage silos, to form a seamless material handling system. Shandong HeadPowder Engineering Co., Ltd. offers a range of screw conveyor solutions that are optimized for food additive processing, ensuring efficient and hygienic transport while maintaining product integrity.
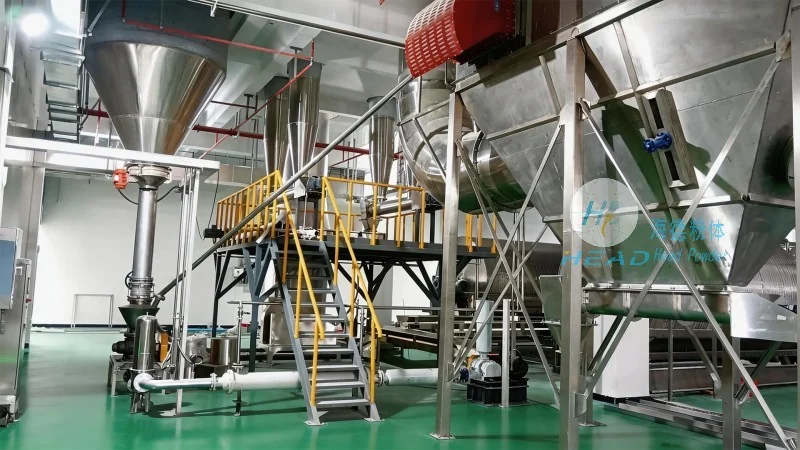
For applications requiring the transport of fine powders or dust-like food additives over longer distances, air-powered or pneumatic conveying systems are a popular choice. These systems use compressed air to move material through a pipeline, eliminating the need for mechanical components in the conveying path. Pneumatic conveyors can be classified as pressure or vacuum systems, depending on the method of material transport. Pressure systems use air to push material forward, while vacuum systems use suction to draw material into the line. This technology is particularly effective for handling materials that are prone to caking or agglomeration, as the air flow helps to break up clumps and maintain a consistent flow. However, careful consideration must be given to the material's dust properties and the system's ability to handle particulate matter without causing blockages or contamination. Shandong HeadPowder Engineering Co., Ltd. provides pneumatic conveying solutions that are designed to handle a variety of food additives, ensuring reliable performance and compliance with food safety standards.
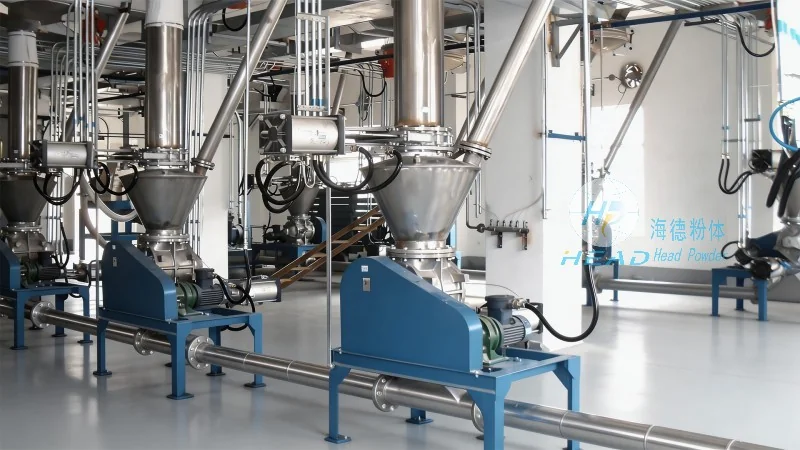
Bulk food additives, including larger granules or irregularly shaped particles, may be transported using vibration conveyors. These systems utilize a vibrating mechanism to move material along a trough or conveyor belt, leveraging the force of vibration to overcome friction and gravity. Vibration conveyors are often used for horizontal or slightly inclined transport, and their design allows for gentle material handling that reduces the risk of product damage. The frequency and amplitude of the vibration can be adjusted to optimize the conveying speed and efficiency, making them suitable for a wide range of bulk materials. In food processing, vibration conveyors are commonly integrated with storage bins and processing equipment to create a continuous material flow. Shandong HeadPowder Engineering Co., Ltd. specializes in the design and manufacturing of vibration conveyors tailored to the specific needs of food additive handling, ensuring efficient and hygienic transport while maintaining product quality.
When selecting a conveying method for food additives, several factors must be considered, including the physical properties of the additive (e.g., viscosity, particle size, moisture content), the required transport distance, the desired flow rate, and the need for hygienic or sanitary operation. Pump-based systems excel in liquid or semi-liquid applications, while screw and vibration conveyors are ideal for solid bulk materials. Pneumatic conveying offers flexibility for fine powders and long-distance transport. The choice of system should also take into account maintenance requirements, energy efficiency, and compliance with regulatory standards such as FDA or EU food safety guidelines. Shandong HeadPowder Engineering Co., Ltd. provides comprehensive expertise and customized solutions to help food manufacturers select and implement the most appropriate conveying method for their specific food additive processing needs, ensuring optimal performance, safety, and cost-effectiveness.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top