Multi-functional material handling systems represent a critical component in modern industrial operations, designed to streamline the movement, storage, and management of various materials with high efficiency and adaptability. These systems are integral to optimizing workflow, reducing labor costs, and enhancing overall productivity across diverse industries. Understanding the core components and design principles behind such systems is essential for businesses seeking to enhance their operational capabilities.
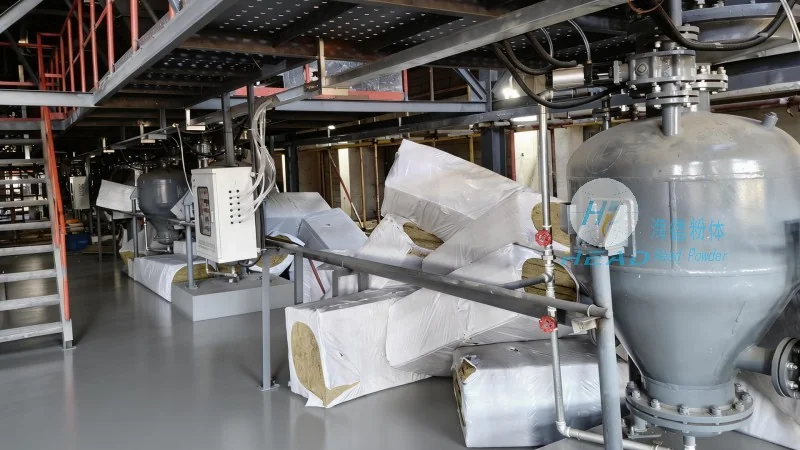
At the heart of a multi-functional material handling system are several interconnected components that work in synergy to achieve seamless material flow. These typically include conveyors, sorters, storage solutions, and control systems. Conveyors, such as belt or chain systems, facilitate the movement of materials over short to medium distances, while sorters enable the segregation of items based on size, weight, or other characteristics. Storage solutions, including automated storage and retrieval systems (AS/RS), provide organized and efficient storage of materials, ensuring quick access when needed. Control systems, often integrated with advanced software, manage the entire operation, coordinating the movement of materials and optimizing processes based on real-time data.
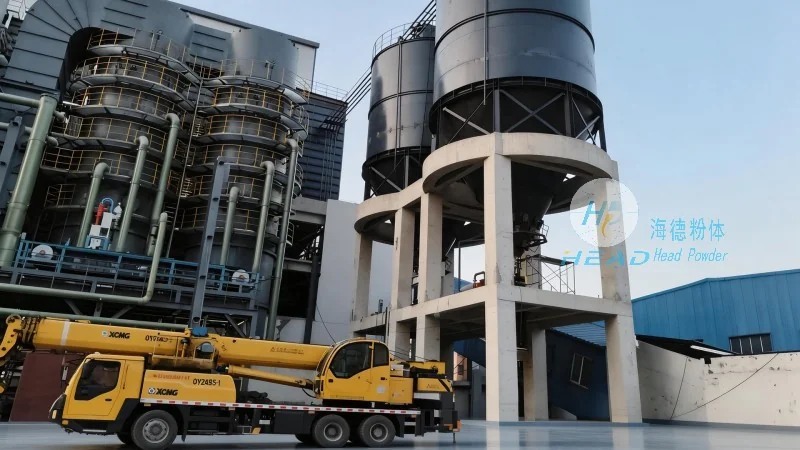
The design of a multi-functional material handling system follows several key principles aimed at maximizing efficiency and adaptability. First, modularity is a fundamental principle, allowing systems to be easily expanded or reconfigured to accommodate changing production needs. This flexibility ensures that the system can evolve with the business, reducing the need for costly overhauls. Second, integration is crucial; the system should integrate seamlessly with existing production lines and software, minimizing disruptions and ensuring data consistency. Third, energy efficiency is a modern consideration, with many designs incorporating energy-saving features like variable speed drives and optimized power usage. Finally, safety is paramount, with systems incorporating features like emergency stop buttons, safety sensors, and compliance with industry standards to protect both personnel and equipment.
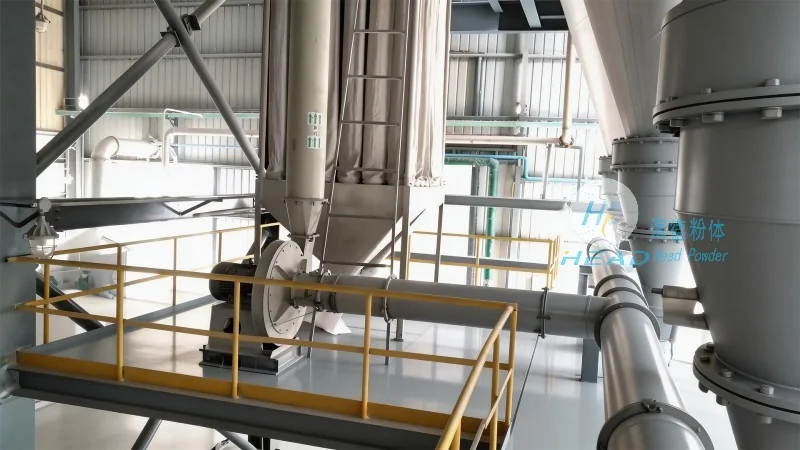
Multi-functional material handling systems are widely adopted across various industries due to their versatility. In manufacturing, they streamline the movement of raw materials to production lines and finished products to storage or shipping areas. In logistics and warehousing, these systems enhance order picking, sorting, and inventory management, improving order fulfillment rates and reducing handling time. The food and beverage industry also benefits, with systems designed to handle perishable goods while maintaining hygiene standards. Additionally, in the pharmaceutical sector, such systems ensure the secure and efficient handling of sensitive materials, adhering to strict regulatory requirements. The adaptability of these systems makes them suitable for a wide range of applications, from small-scale operations to large-scale industrial facilities.
Shandong HeadPowder Engineering Co., Ltd., a leading provider of material handling solutions, specializes in designing and implementing multi-functional systems tailored to the unique needs of clients. With a focus on innovation and customer-centric approaches, the company leverages advanced technology and engineering expertise to deliver systems that enhance operational efficiency and productivity. HeadPowder's solutions are built with modularity and adaptability in mind, allowing businesses to scale their operations as their needs evolve. The company's commitment to quality and safety ensures that their systems not only meet but often exceed industry standards, providing reliable and durable performance. HeadPowder's team of experts works closely with clients to understand their specific requirements, from initial design and installation to ongoing maintenance and support, ensuring a comprehensive and effective material handling solution.
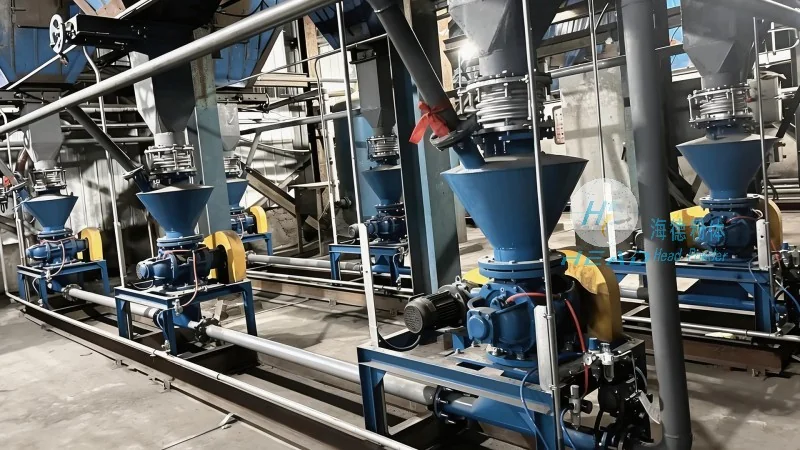
As industries continue to evolve and demand higher efficiency and adaptability, multi-functional material handling systems remain a cornerstone of modern operations. The design principles and components discussed highlight the importance of flexibility, integration, and efficiency in these systems. Companies like Shandong HeadPowder Engineering Co., Ltd. play a vital role in providing tailored solutions that meet the evolving needs of businesses. By investing in such systems, organizations can enhance their operational capabilities, reduce costs, and stay competitive in a dynamic market. The future of material handling lies in intelligent, adaptable systems that can seamlessly integrate with advanced technologies, driving further improvements in productivity and efficiency.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top