Understanding the process of handling powdered electrolytes is crucial for industries that rely on these materials in their production processes. Powdered electrolytes, often used in battery manufacturing and other electrochemical applications, require specialized equipment and systems to ensure efficient and safe transport. This article explores the fundamental aspects of powdered electrolyte material handling, including the key design principles that underpin effective systems.
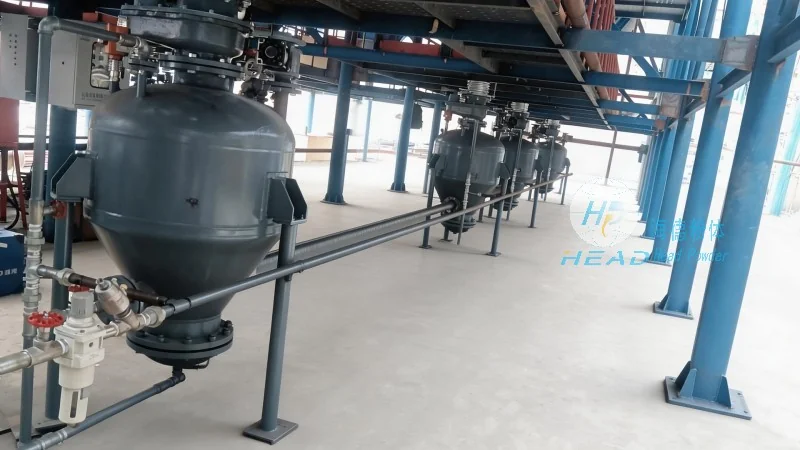
The core of any effective powdered electrolyte handling system involves several critical components. These typically include feeders, conveyors, storage vessels, and control mechanisms. Each component plays a vital role in ensuring the material is moved efficiently from one stage of the process to the next. For instance, feeders are used to regulate the flow of the powder, preventing overloading or underflow that could disrupt the entire system. Conveyors, such as pneumatic or mechanical systems, then transport the material to the next processing stage. Storage vessels are designed to hold the material in bulk, ensuring a steady supply for continuous operation.
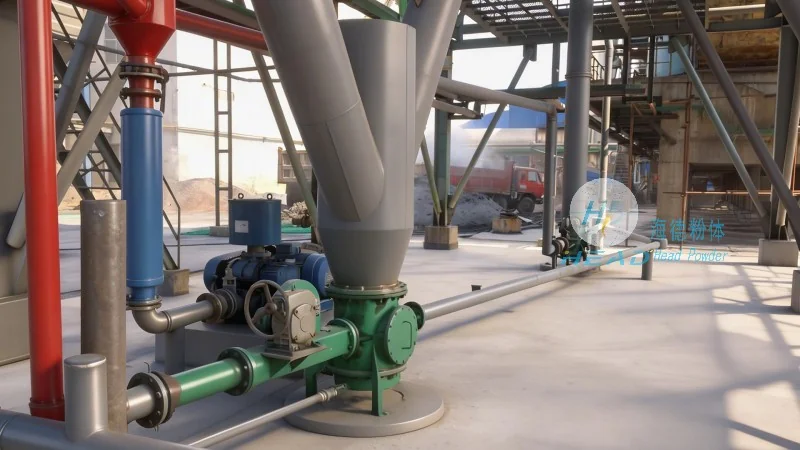
Designing a successful powdered electrolyte handling system requires adherence to several key principles. One of the most important is the principle of minimizing material degradation. Powdered electrolytes are often sensitive to moisture, temperature, and mechanical stress, which can affect their performance. Therefore, systems are designed with materials that are resistant to these factors, such as stainless steel or specialized polymers, to maintain the integrity of the material. Another critical principle is the prevention of dust generation and containment. Proper sealing and filtration systems are essential to prevent dust from escaping into the environment and to protect personnel from exposure. This not only ensures compliance with safety regulations but also maintains the quality of the material by preventing contamination.
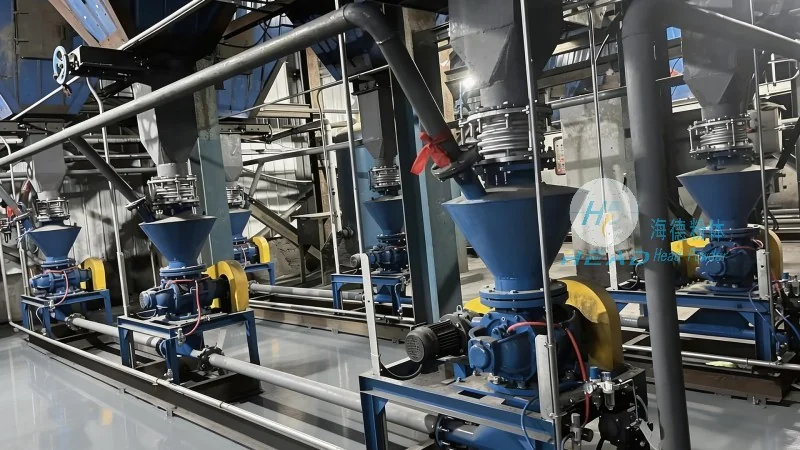
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading provider of specialized equipment and systems for handling powdered materials. With a focus on innovation and customer-centric solutions, HeadPowder has developed advanced technologies tailored to the unique challenges of handling electrolytes. The company’s expertise lies in designing systems that balance efficiency, safety, and cost-effectiveness. By leveraging years of experience in the field, HeadPowder has become a trusted partner for businesses seeking reliable and high-performance material handling solutions. Their products are engineered to meet the specific needs of each client, ensuring optimal performance in diverse industrial applications.
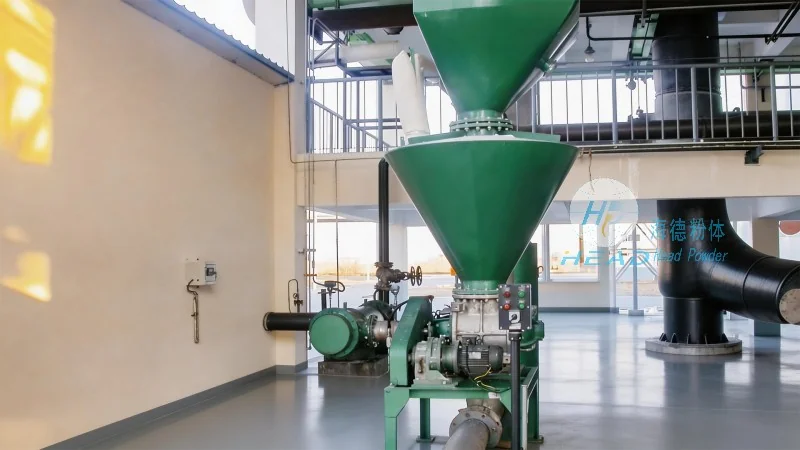
Handling powdered electrolytes comes with several challenges that must be addressed through thoughtful design. One of the primary challenges is the risk of clogging in the system, which can occur due to the fine particle size and potential for agglomeration. To mitigate this, systems are equipped with features such as agitators, vibrators, and self-cleaning mechanisms that keep the material in a fluidized state. Another challenge is maintaining consistent flow rates, which is critical for maintaining production efficiency. Advanced control systems, including sensors and automation, are integrated into the design to monitor and adjust flow rates in real-time, ensuring stable operation. Additionally, the need for dust control and environmental compliance is a significant consideration. HeadPowder’s solutions incorporate robust dust collection systems and compliance features to meet regulatory standards while protecting the environment.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top