Grain pneumatic conveying systems are essential in modern agricultural and food processing industries, providing efficient and reliable methods for transporting bulk materials like grains, powders, and other granular substances. These systems utilize air or gas as the conveying medium to move materials from one location to another, eliminating the need for mechanical components such as belts, chains, or buckets that are common in traditional conveyor systems. The technology has evolved significantly over the years, offering advantages in terms of hygiene, flexibility, and energy efficiency, making it a preferred choice for many applications in the grain handling sector.
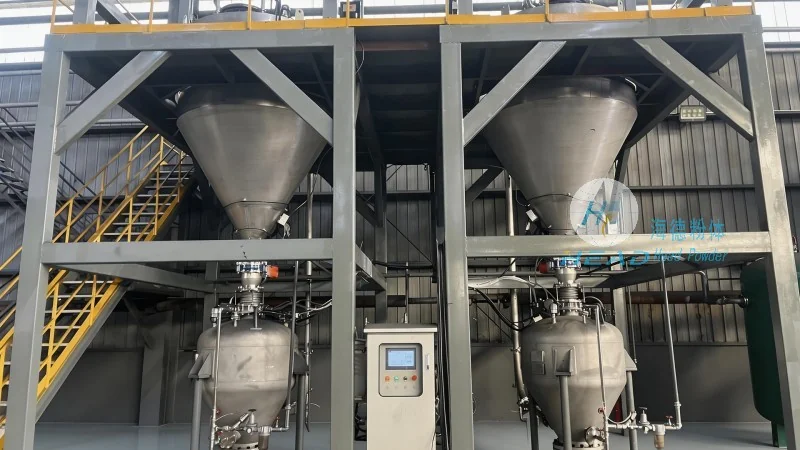
At the core of a pneumatic conveying system is the ability to create a pressure differential or use suction to move materials through a pipeline. The system typically consists of several key components, including a material feed hopper, a conveyor line (often made of metal or plastic pipes), a fan or blower to generate the air flow, and a control system to regulate the operation. The process begins when the grain is fed into the hopper, where it is then drawn into the conveyor line by the moving air. The air flow carries the grain particles along the pipeline, ensuring a smooth and continuous transfer. This method is particularly effective for handling delicate or sensitive materials, as it minimizes friction and impact, reducing the risk of product damage.
One of the primary advantages of pneumatic conveying is its ability to handle a wide range of materials, from fine powders to large grain particles. The system can be designed to accommodate different particle sizes and densities, making it versatile for various applications. Additionally, the enclosed pipeline design helps maintain product quality by preventing contamination from external sources and reducing exposure to moisture or dust. This is especially important in food processing, where hygiene and product integrity are critical. The flexibility of the system also allows for easy integration with other processing equipment, such as storage silos, processing plants, or packaging lines, enabling a seamless workflow from raw material to finished product.
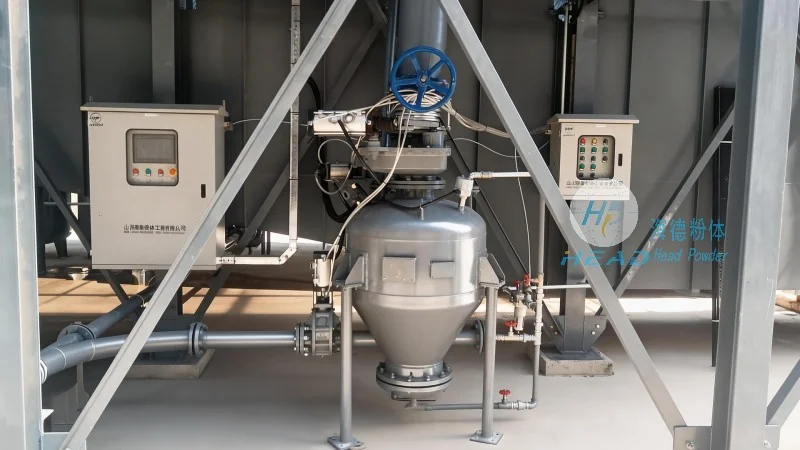
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer in the field, specializes in the design, manufacturing, and installation of advanced pneumatic conveying systems tailored to the specific needs of the grain industry. With a strong commitment to quality and innovation, the company has developed state-of-the-art solutions that enhance operational efficiency and product safety. Based in Shandong, China, HeadPowder leverages its extensive experience and technical expertise to deliver customized systems that meet the highest industry standards. The company's products are known for their durability, reliability, and energy efficiency, ensuring long-term performance and minimal maintenance costs for clients.
The working principle of a typical grain pneumatic conveying system involves the use of a positive pressure or negative pressure (suction) system. In a positive pressure system, a fan or blower generates high-pressure air that pushes the material through the pipeline. The air flow is controlled to maintain a consistent velocity, ensuring that the grain particles are carried efficiently without clogging the line. The system may include features such as pulse jets or rotary valves to regulate the flow and prevent material buildup. On the other hand, a negative pressure system uses a vacuum to draw the material into the pipeline, which is often preferred for applications where the material needs to be transported from a lower elevation or where dust control is a priority.
Key components of a pneumatic conveying system include the material feed mechanism, which can be a hopper or a rotary valve, ensuring a steady supply of grain. The conveyor line itself is designed to withstand the pressure and flow of the air and material, with materials like stainless steel or high-density polyethylene used for durability and resistance to corrosion. The fan or blower is a critical component, as it must generate sufficient airflow to move the grain while maintaining energy efficiency. Modern systems often incorporate variable frequency drives (VFDs) to adjust the fan speed based on the material load, optimizing energy consumption. The control system, which may include sensors and automation, monitors the flow rate, pressure, and other parameters to ensure smooth operation and prevent system failures.
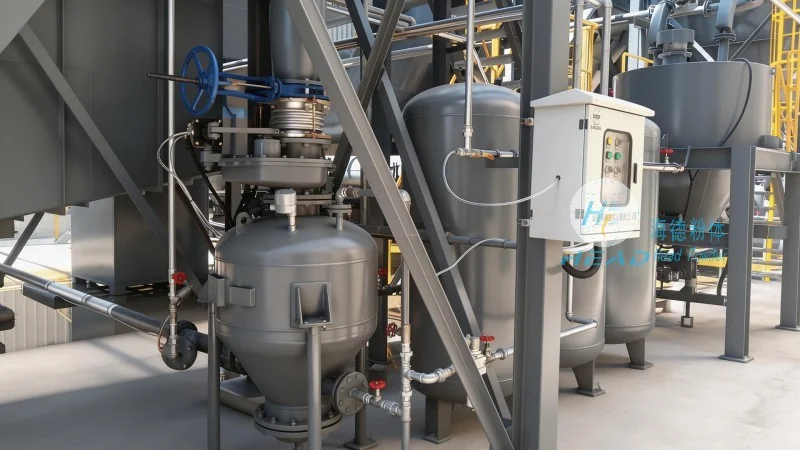
For grain handling applications, the choice of system design depends on factors such as the material characteristics, the distance to be conveyed, and the required throughput. Positive pressure systems are generally more suitable for short to medium distances and high material loads, while negative pressure systems are better for longer distances or when handling fine powders that are prone to dust. The system's design also considers the need for cleaning and maintenance, with features like purge valves and access points to facilitate regular upkeep. HeadPowder's expertise lies in customizing these systems to meet the unique requirements of each client, ensuring optimal performance and reliability in real-world conditions.
In conclusion, grain pneumatic conveying systems represent a sophisticated and efficient solution for transporting bulk materials in the agricultural and food processing industries. By leveraging the principles of air flow and pressure differential, these systems offer numerous benefits, including improved hygiene, reduced product damage, and enhanced operational flexibility. Shandong HeadPowder Engineering Co., Ltd. plays a vital role in advancing this technology, providing high-quality, customized solutions that meet the evolving needs of the grain industry. With its focus on innovation and customer satisfaction, HeadPowder continues to be a trusted partner for businesses seeking reliable and efficient pneumatic conveying systems.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top