HeadPowder, a leading engineering company based in Shandong, China, specializes in the design and implementation of advanced pneumatic conveying systems for powdered materials like beans. This article delves into the fundamental concepts of powdered bean pneumatic conveying and explores the core design principles that underpin these systems.
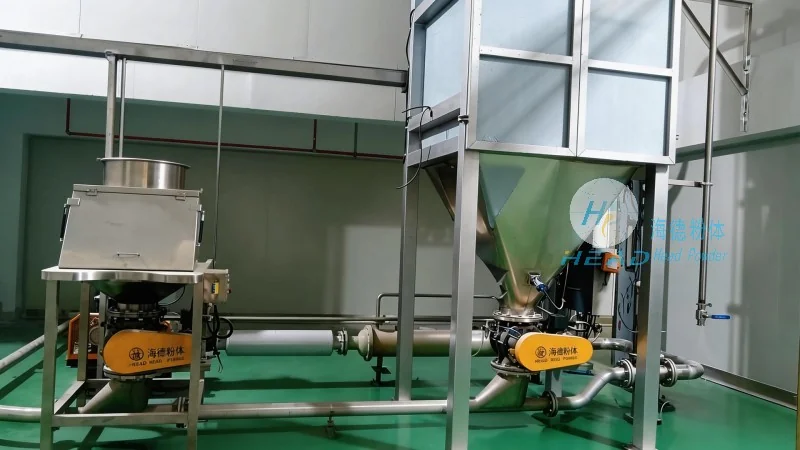
Powdered bean pneumatic conveying is a method of transporting dry, fine materials such as powdered beans through a pipeline using a stream of air or other gas. Unlike traditional mechanical conveying systems that rely on belts, buckets, or screws, pneumatic conveying uses pressure or vacuum to move the material. This technique is particularly advantageous for transporting delicate, abrasive, or hygroscopic materials like powdered beans, as it minimizes product degradation and contamination.
The effectiveness of a pneumatic conveying system for powdered beans hinges on several key design principles. First, the system must ensure efficient material suspension and transport. This involves selecting the appropriate air velocity and pressure to maintain the material in a fluidized state within the pipeline. For powdered beans, the air velocity is typically optimized to prevent particle segregation and ensure uniform flow. Second, the system must incorporate proper equipment selection, including the choice of a suitable air compressor, material feeders, and pipeline configuration. The air compressor provides the necessary pressure or vacuum, while the feeder controls the material flow rate to match the conveying capacity. Third, the design must address the challenges of material handling, such as preventing blockages, ensuring smooth transitions between different sections of the pipeline, and maintaining consistent material quality. This includes incorporating features like cyclones for separation, filters for air purification, and check valves to prevent backflow.
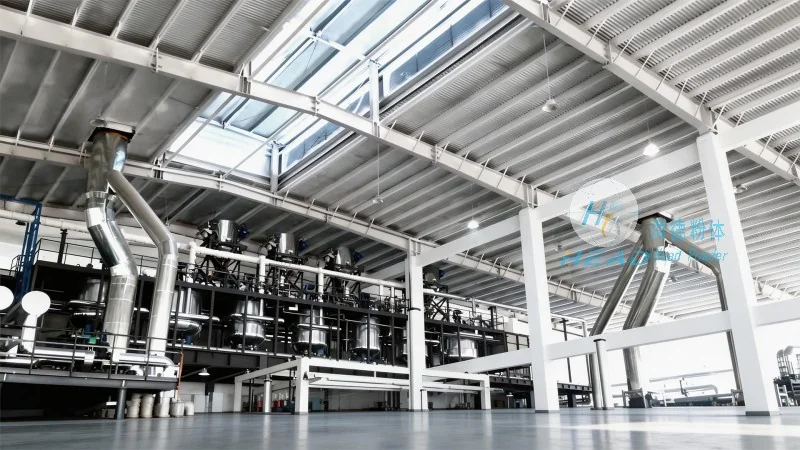
A typical powdered bean pneumatic conveying system consists of several critical components, each playing a vital role in the overall operation. The air compressor is the heart of the system, generating the pressure or vacuum required to move the material. It can be a positive displacement compressor or a rotary screw compressor, depending on the system's capacity and pressure needs. The material feeder, often a rotary valve or a star feeder, ensures a controlled and consistent flow of powdered beans into the pipeline. The pipeline itself is usually made of stainless steel or other corrosion-resistant materials to handle the abrasive nature of the material and maintain hygiene standards. Cyclones are commonly used for material separation, where the air and material are separated by centrifugal force, allowing the material to be collected and the air to be filtered and recycled. Filters are essential for maintaining air quality and preventing dust accumulation in the system. Additionally, check valves and pressure relief valves are installed to prevent backflow and protect the system from overpressure.
Compared to traditional mechanical conveying methods, pneumatic conveying offers several advantages when handling powdered beans. One of the most significant benefits is the ability to transport materials over long distances with minimal maintenance. The system is also more flexible, as it can be easily reconfigured or expanded to accommodate changes in production volume or material types. Pneumatic conveying also reduces product damage and contamination, which is crucial for sensitive materials like powdered beans. The enclosed pipeline design prevents exposure to dust, moisture, or other contaminants, ensuring the final product meets quality standards. Furthermore, the system can handle a wide range of material properties, including different particle sizes, densities, and flowabilities, making it a versatile solution for various applications.
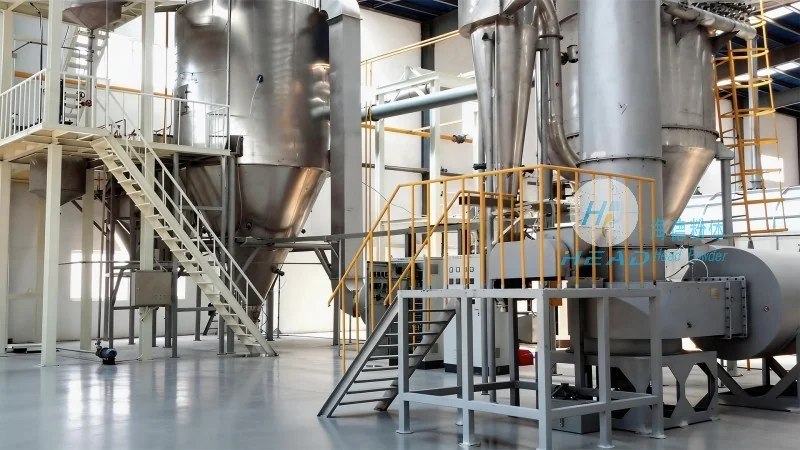
Powdered bean pneumatic conveying is widely used in several industries, including food processing, pharmaceuticals, and chemical manufacturing. In the food industry, it is commonly employed in the processing of beans for making flour, protein powders, or other food products. The system ensures that the beans are transported efficiently and hygienically, maintaining the quality and safety of the final food products. In the pharmaceutical industry, pneumatic conveying is used to transport powdered ingredients for drug manufacturing, where contamination control is paramount. The system's ability to handle delicate materials without damage makes it ideal for this application. Similarly, in the chemical industry, pneumatic conveying is used to transport various powders, including those used in the production of fertilizers, paints, or other chemical products. The system's flexibility and efficiency make it a preferred choice for these industries.
HeadPowder, with its expertise in engineering and design, provides comprehensive solutions for powdered bean pneumatic conveying systems. By adhering to the core design principles and utilizing advanced components, these systems offer efficient, reliable, and hygienic transportation of powdered beans. The company's commitment to quality and innovation ensures that its systems meet the highest standards, making them suitable for various industrial applications. As the demand for efficient and sustainable material handling solutions continues to grow, pneumatic conveying systems like those offered by HeadPowder remain a vital component in modern industrial operations.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top