Grain silo powder conveying machines are specialized equipment designed to handle and transport bulk powder materials, such as grains, powders, and other fine particulate substances, within grain storage facilities. These systems are essential for efficient material handling, ensuring smooth and reliable movement of powders from storage silos to processing or distribution points. The design of these machines is tailored to meet the unique challenges of powder handling, including preventing material segregation, maintaining consistent flow, and ensuring minimal product degradation.
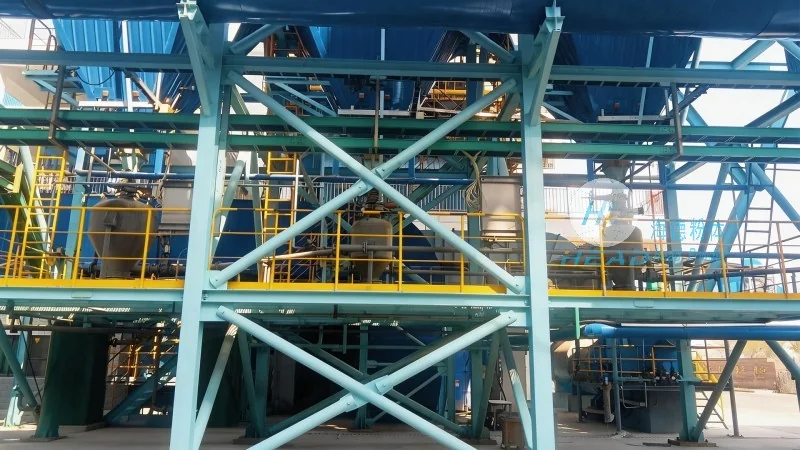
At the core of grain silo operations, powder conveying machines play a critical role in optimizing workflow and maintaining operational efficiency. These systems are engineered to handle the physical and chemical properties of various powders, such as moisture content, particle size distribution, and flowability. By integrating advanced engineering principles, these machines ensure that powders are transported safely and effectively, reducing the risk of blockages, spills, or contamination. The technology behind these machines combines mechanical, pneumatic, and hydraulic components to achieve precise control over material movement, making them indispensable in modern grain storage and processing industries.
The design of a grain silo powder conveying machine is governed by several key principles that address the specific demands of powder handling. First, the system must accommodate the varying characteristics of different powders, including their density, cohesion, and tendency to agglomerate. Engineers use materials that are non-reactive and easy to clean, such as stainless steel or food-grade plastics, to prevent contamination and ensure compliance with industry standards. Second, the design emphasizes energy efficiency and minimal maintenance, incorporating components that reduce wear and tear while maximizing throughput. For example, the use of variable speed drives and intelligent control systems allows for adaptive flow rates, optimizing energy consumption based on the material being conveyed.
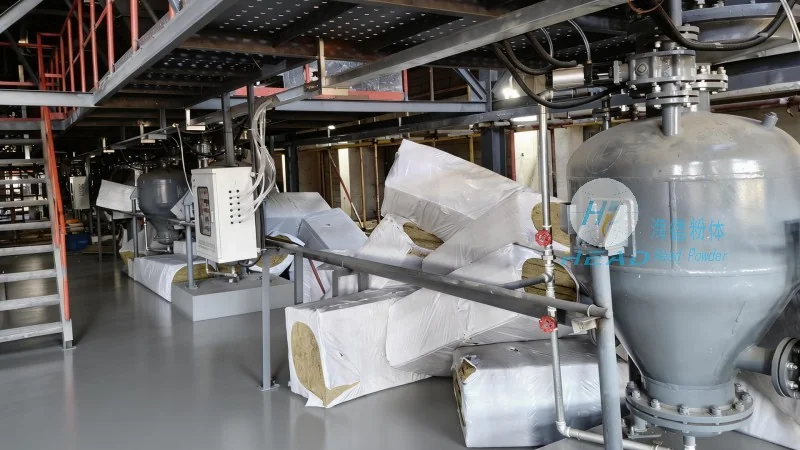
Third, the system is designed with safety in mind, incorporating features like pressure relief valves, overload protection, and emergency stop mechanisms. These safety measures are crucial in preventing accidents and ensuring the well-being of operators. Additionally, the design considers the need for easy maintenance and accessibility, with components that can be quickly disassembled and cleaned, reducing downtime and operational costs. The integration of sensors and monitoring systems further enhances safety and operational performance, providing real-time data on system status and potential issues.
A typical grain silo powder conveying machine consists of several key components, each playing a vital role in the overall operation. The hopper or silo inlet is the first component, where powders are fed into the system. This component is designed to minimize material segregation and ensure a uniform flow of material into the conveyor. The hopper may include features like a cone or a vibratory feeder to help control the flow rate and prevent blockages. Next, the conveyor itself, which can be either pneumatic or mechanical, transports the powder from the silo to the discharge point. Pneumatic systems use compressed air to move powders through pipes, while mechanical systems employ screws, belts, or buckets to achieve the same goal. The choice between these systems depends on the specific characteristics of the powder and the operational requirements of the facility.
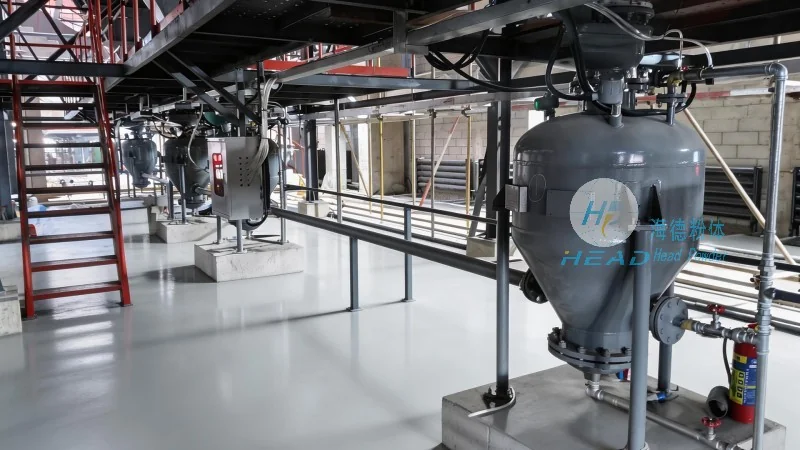
The discharge section is another critical component, where the powder is released from the conveyor system. This section is designed to ensure a controlled and uniform discharge, preventing spillage and maintaining product integrity. The discharge may include a valve or a gate that can be adjusted to control the flow rate, allowing for precise material delivery. Finally, the control system manages all aspects of the operation, including speed, pressure, and flow rate. Modern control systems use programmable logic controllers (PLCs) and human-machine interfaces (HMIs) to provide operators with real-time monitoring and control capabilities, enhancing operational efficiency and safety.
Grain silo powder conveying machines are widely used in various applications within the grain storage and processing industry. They are essential in feed mills, where they transport raw materials like corn, soybeans, and wheat to processing equipment. In flour mills, these systems are used to move flour and other fine powders from storage silos to packaging or blending areas. Additionally, they are utilized in food processing facilities, where they handle ingredients like sugar, cocoa, and spices, ensuring consistent quality and flow. The benefits of using these machines extend beyond efficiency; they also contribute to product quality by minimizing contamination and maintaining the integrity of the powder. By preventing segregation and ensuring uniform flow, these systems help maintain the nutritional and sensory properties of the materials being handled.
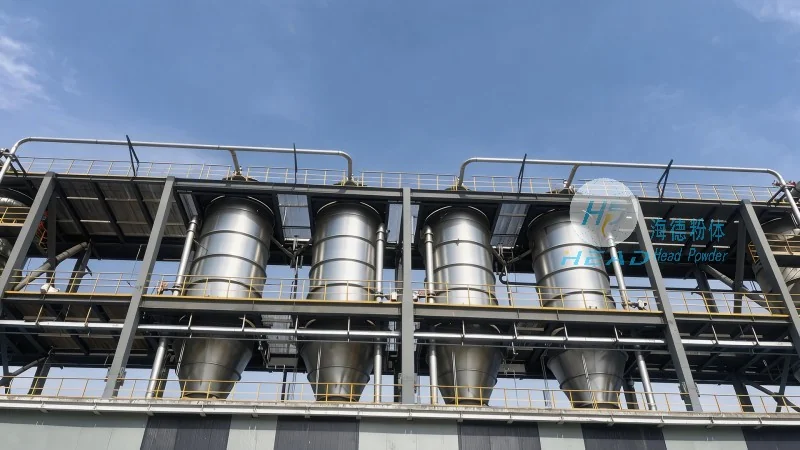
Furthermore, the use of advanced powder conveying systems improves operational safety and reduces labor costs. Automated control systems reduce the need for manual intervention, minimizing the risk of human error and improving consistency. The energy-efficient design of these machines also helps lower operational costs, making them a cost-effective solution for grain storage facilities. Overall, grain silo powder conveying machines are a critical component of modern grain handling operations, enabling efficient, safe, and reliable material transport while maintaining product quality.
Shandong HeadPowder Engineering Co., Ltd. is a leading manufacturer of specialized powder handling equipment, including grain silo powder conveying machines. HeadPowder is headquartered in Shandong, China, and has established itself as a trusted provider of high-quality, reliable equipment for the grain and food processing industries. The company specializes in designing and manufacturing custom solutions tailored to the specific needs of its clients, ensuring that each system is optimized for performance, efficiency, and safety. With a commitment to innovation and customer satisfaction, HeadPowder has built a reputation for delivering durable and effective powder conveying systems that meet the highest industry standards. The company's products are widely used in various applications, from small-scale farms to large industrial facilities, providing reliable and efficient material handling solutions.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top