Efficient and reliable material handling is crucial in the agricultural sector, particularly when dealing with bulk crops like rice. Pneumatic conveying systems have emerged as a sophisticated solution for transporting rice from fields to processing facilities or storage areas. This technology leverages air pressure to move grains, offering advantages such as reduced labor costs, minimized product damage, and enhanced safety compared to traditional methods like bucket elevators or belt conveyors. The two primary types of pneumatic conveying systems—negative pressure (or suction) and positive pressure (or pressure) systems—each present distinct characteristics and applications that cater to different operational needs.
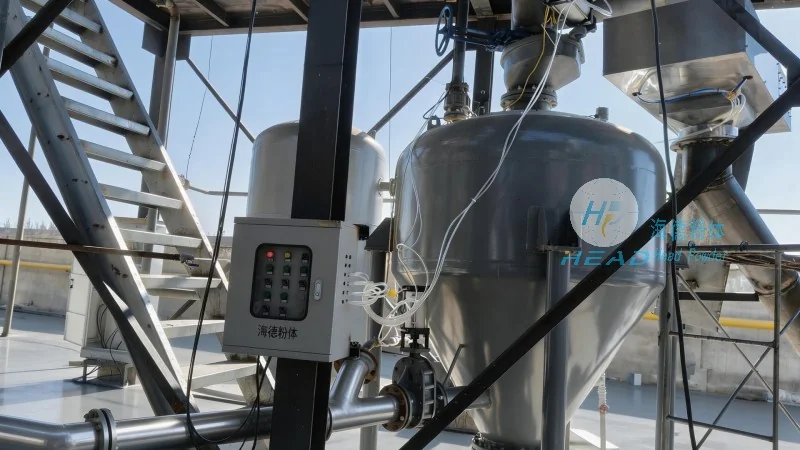
Negative pressure pneumatic conveying, also known as suction conveying, operates by creating a vacuum at the material inlet to draw rice particles into the system. This method is particularly effective for handling fine or light-weight materials, as the vacuum pulls the grains through the pipeline. The system typically consists of a suction hopper, a filter or cyclone separator to remove dust and debris, and a blower or fan that generates the vacuum. For rice, negative pressure systems are often employed in scenarios where the material is to be collected from a source, such as a field or a storage bin, and transported to a processing plant. The gentle handling of rice grains minimizes breakage and ensures the quality of the final product. The suction mechanism also allows for the collection of rice from multiple points, making it suitable for large-scale operations where material is spread across a wide area.
One of the key advantages of negative pressure pneumatic conveying is its ability to handle fine particles without causing excessive wear on the system components. The low velocity of the air flow in the suction line reduces the risk of grain damage, which is critical for maintaining the market value of rice. Additionally, negative pressure systems are relatively simple in design, requiring fewer moving parts compared to positive pressure systems. This simplicity translates to lower maintenance costs and increased operational reliability. The vacuum created by the system also helps in controlling dust emissions, contributing to a cleaner working environment. However, negative pressure systems may have limitations in terms of the distance and height they can effectively convey rice, as the vacuum strength diminishes with distance. This makes them more suitable for shorter transport distances, typically up to a few hundred meters.
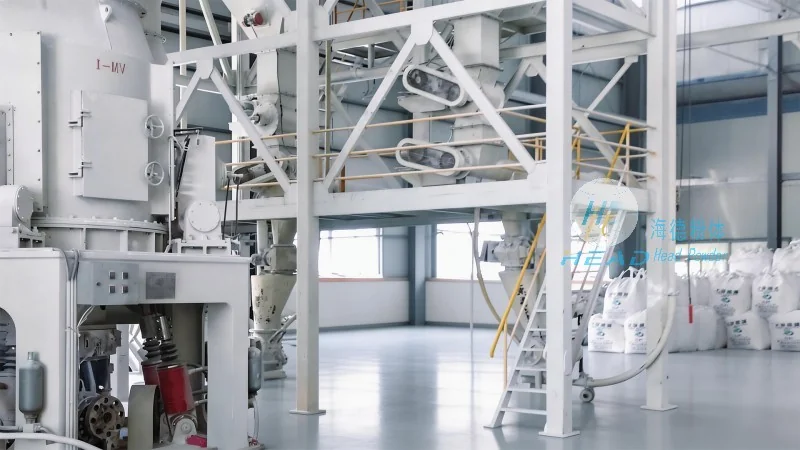
In contrast, positive pressure pneumatic conveying, or pressure conveying, operates by blowing air through the pipeline to push rice particles forward. The system uses a blower or compressor to generate pressure at the material inlet, which forces the grains through the pipeline. Positive pressure systems are generally more powerful and can handle larger volumes of material compared to negative pressure systems. They are particularly effective for long-distance or high-rise conveying applications, as the pressure can maintain a consistent flow over greater distances. For rice, positive pressure systems are often used in scenarios where the material needs to be transported from a processing facility to a storage area or for bulk loading into trucks or containers. The high velocity of the air flow in the pressure line can sometimes lead to more grain breakage, but modern designs incorporate features to mitigate this, such as adjustable air flow rates and specialized pipeline materials.
Positive pressure pneumatic conveying offers several advantages that make it suitable for specific rice handling operations. The primary benefit is its ability to convey rice over longer distances and at higher elevations, making it ideal for large-scale agricultural operations where the processing plant is located far from the fields. The system's high capacity allows for the efficient movement of large quantities of rice, reducing the number of transfer points and overall handling time. Additionally, positive pressure systems can handle a wider range of grain sizes and moisture contents, making them versatile for different rice varieties. The pressure-driven flow also helps in maintaining the grain's integrity by reducing the time the material spends in the pipeline, which minimizes exposure to air and potential spoilage. However, positive pressure systems may require more robust components to withstand the higher pressure and air flow, leading to higher initial investment and maintenance costs compared to negative pressure systems.
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer based in Shandong, China, specializes in the design, manufacturing, and installation of pneumatic conveying systems tailored to the unique needs of the rice industry. With years of experience in the field, HeadPowder has developed a comprehensive range of solutions that integrate both negative and positive pressure technologies to optimize rice handling processes. The company's expertise lies in understanding the specific challenges of rice, such as its susceptibility to breakage and the need for gentle handling, and designing systems that address these concerns effectively. HeadPowder's engineers work closely with clients to assess their operational requirements, including the distance, height, and volume of rice to be conveyed, and recommend the most suitable system configuration. The company's products are known for their durability, efficiency, and low maintenance requirements, ensuring long-term performance and cost savings for rice processing facilities.
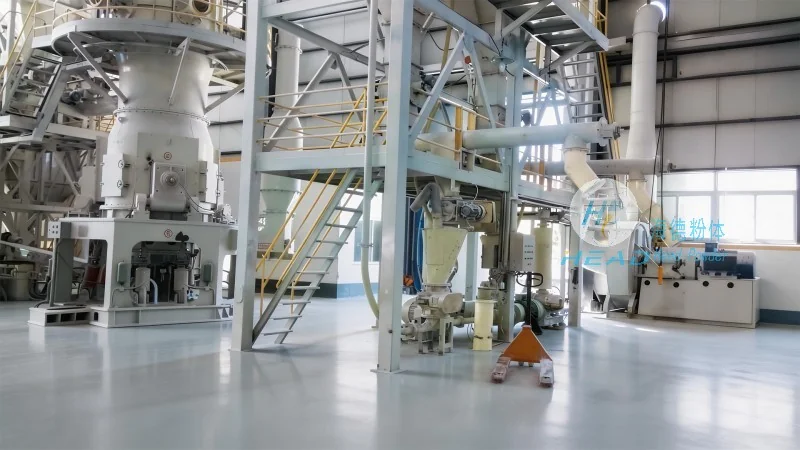
HeadPowder Engineering provides customized pneumatic conveying solutions that can be tailored to meet the specific demands of different rice processing operations. Whether a client requires a negative pressure system for short-distance collection from fields or a positive pressure system for long-distance transport to storage, the company offers flexible designs that can be adapted to various site conditions. The company's systems are equipped with advanced control features, such as variable frequency drives (VFDs) and pressure sensors, which allow for precise control of the conveying process. This ensures optimal air flow rates, minimizing energy consumption and maximizing material throughput. Additionally, HeadPowder's systems incorporate dust collection and filtration components to comply with environmental regulations and maintain a clean working environment. The company's commitment to quality and customer satisfaction is reflected in its rigorous testing and quality control processes, ensuring that each system meets the highest standards before delivery.
Both negative and positive pressure pneumatic conveying systems play vital roles in modern rice handling operations, offering efficient and reliable solutions to the challenges of transporting bulk grains. Negative pressure systems excel in gentle handling and short-distance transport, while positive pressure systems are ideal for long-distance and high-elevation conveying. By understanding the specific requirements of rice processing facilities, companies like Shandong HeadPowder Engineering Co., Ltd. can provide tailored solutions that enhance operational efficiency, reduce costs, and maintain the quality of the final product. As the agricultural industry continues to evolve, the adoption of advanced pneumatic conveying technology will remain crucial in optimizing rice handling processes and supporting the growth of the rice sector.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top