HeadPowder, a leading provider in the field of material handling solutions, specializes in advanced pneumatic conveying systems tailored for soap pellet applications. This article delves into the technical nuances of both negative and positive pressure pneumatic conveying, offering a comprehensive understanding of their operational principles, advantages, and practical applications.
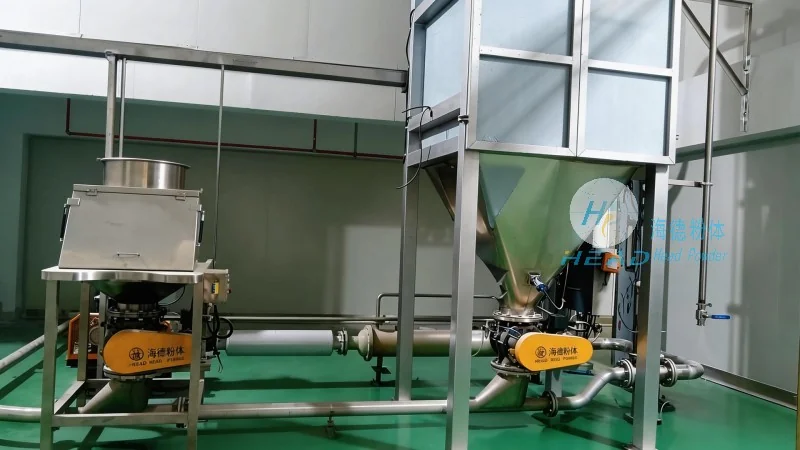
HeadPowder Engineering Co., Ltd., based in Shandong, China, is dedicated to delivering high-efficiency and reliable pneumatic conveying technologies. With years of industry experience, the company has developed specialized solutions for handling soap pellets, ensuring optimal performance and minimal operational disruptions. The company’s commitment to innovation and customer satisfaction has positioned it as a trusted partner in the material handling sector.
Pneumatic conveying is a method of transporting bulk materials through a pipeline using air or gas as the conveying medium. For soap pellets, this technology offers a dust-free, efficient, and flexible solution compared to traditional mechanical methods. The two primary types of pneumatic conveying systems are negative pressure (or vacuum) and positive pressure systems, each with distinct characteristics and applications.
Negative pressure systems operate by creating a vacuum at the material intake point, drawing the soap pellets into the conveying line. This approach is particularly effective for handling materials that are prone to dust generation or require a clean transfer environment. The system typically includes a vacuum pump, a material hopper, and a filter to capture any airborne particles. The negative pressure method is ideal for applications where the material is to be transferred from a lower elevation to a higher one, as the vacuum pulls the material upward.
One of the key advantages of negative pressure systems is their ability to handle fine or dusty materials without generating excessive dust. The sealed system prevents contamination and maintains a clean environment, which is crucial for soap pellet applications where product purity is paramount. Additionally, negative pressure conveying can operate with lower air velocities, reducing energy consumption and wear on components. This makes it a cost-effective solution for long-distance or high-rise transfers of soap pellets.
Positive pressure systems, on the other hand, use compressed air to push the soap pellets through the conveying line. The material is loaded into a hopper and then propelled by the force of the compressed air. This method is well-suited for applications where the material needs to be transported from a higher elevation to a lower one, as the air pressure pushes the material downward. Positive pressure systems are often preferred for handling abrasive or sticky materials, as the high air velocity can help break up agglomerates and maintain consistent flow.
Positive pressure conveying offers several benefits for soap pellet handling. The high air velocity ensures consistent material flow, even for materials with varying particle sizes. This reduces the risk of blockages and ensures reliable operation. Additionally, positive pressure systems can handle larger particle sizes and higher material loads compared to negative pressure systems. The ability to use higher air pressures also allows for longer conveying distances without significant pressure loss, making it suitable for industrial-scale soap pellet production and processing facilities.
When selecting between negative and positive pressure pneumatic conveying for soap pellets, several factors must be considered. The choice depends on the specific application requirements, such as the material's properties, the distance and elevation changes, and the desired level of dust control. Negative pressure systems excel in applications requiring a clean, dust-free environment and lower energy consumption, while positive pressure systems are better suited for high-volume, abrasive materials and longer horizontal or vertical distances.
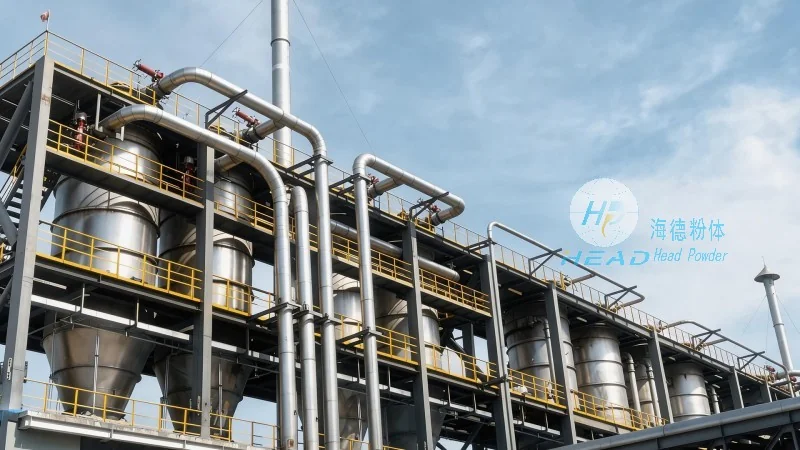
Both negative and positive pressure pneumatic conveying systems find extensive use in the soap pellet production and processing industry. Negative pressure systems are commonly used in the initial stages of material handling, such as transferring raw soap pellets from storage silos to processing equipment. This ensures that the material is transferred without generating dust, maintaining product quality. Positive pressure systems are often employed in the final stages, such as transporting finished soap pellets to packaging lines or storage silos.
Implementing an effective pneumatic conveying system for soap pellets requires careful consideration of several factors. The first is the material's characteristics, including particle size, density, and moisture content. These properties affect the air velocity and pressure required for optimal conveying. The second is the system's layout, including the length and elevation changes of the conveying line. Proper system design ensures that the pressure drop is minimized, reducing energy consumption and wear on components. Additionally, the choice of components, such as the vacuum pump or compressor, and the filter system, is critical for maintaining system efficiency and product quality.
HeadPowder Engineering Co., Ltd. offers customized pneumatic conveying solutions tailored to the specific needs of soap pellet applications. The company's expertise in both negative and positive pressure systems allows it to provide comprehensive solutions that address the unique challenges of soap pellet handling. Whether a client requires a negative pressure system for dust control or a positive pressure system for high-volume transport, HeadPowder can design and implement a system that meets their operational and quality requirements. The company's commitment to quality and customer satisfaction ensures that clients receive reliable and efficient material handling solutions that enhance their production processes.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top