HeadPowder, a leading provider of advanced material handling solutions, specializes in the design, manufacturing, and implementation of pneumatic conveying systems tailored for diverse industrial applications. With a strong presence in China, particularly in Shandong province, the company has established itself as a trusted partner for businesses requiring efficient and reliable transportation of bulk materials, including rare earth elements. This article delves into the core technologies of negative pressure and positive pressure pneumatic conveying, exploring their principles, advantages, and practical applications in the rare earth industry.
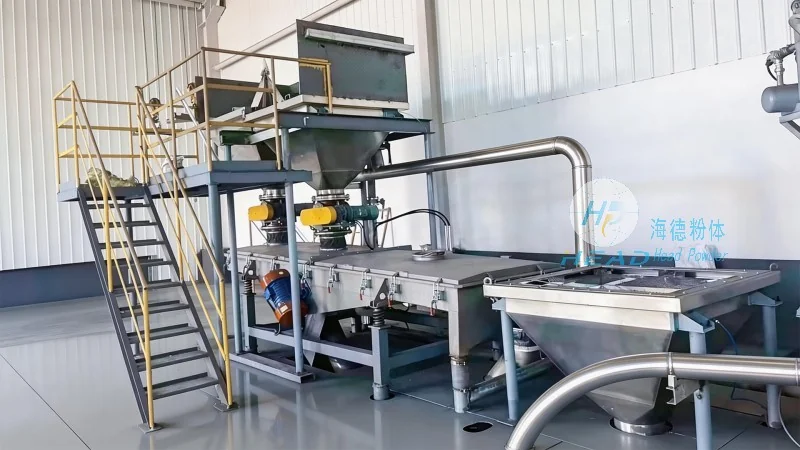
Negative pressure, or suction, pneumatic conveying systems operate by creating a vacuum at the material inlet to draw particles into the conveying line. This method is particularly effective for transporting materials from multiple sources or over relatively short distances, as it can handle a wide range of particle sizes and densities. The system typically consists of a vacuum pump, a material feed hopper, and a conveying pipeline that connects to a collection tank or processing unit. The vacuum created by the pump pulls the material through the line, ensuring a continuous flow. A key advantage of negative pressure systems is their ability to handle materials that are dusty or have a tendency to create static electricity, as the enclosed pipeline prevents dust from escaping into the environment. This makes them ideal for applications where environmental control is critical, such as in the processing of rare earth ores, where dust containment is essential to maintain air quality and protect equipment.
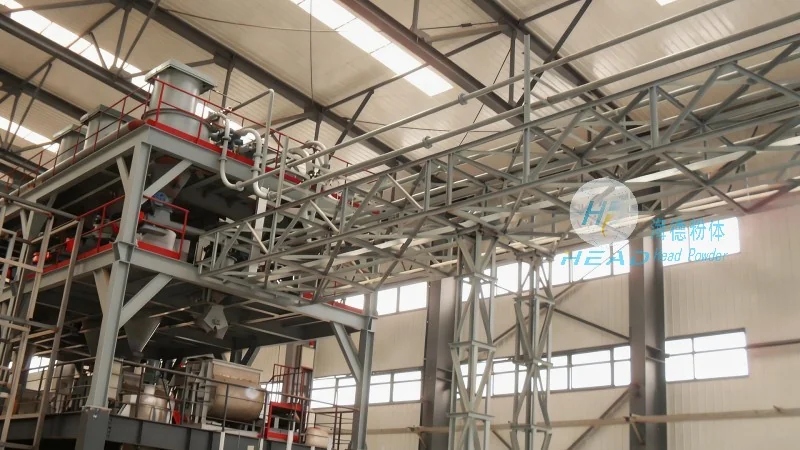
Positive pressure, or pressure, pneumatic conveying systems work by forcing air or a carrier gas through the conveying line under pressure, pushing the material forward. Unlike negative pressure systems, which rely on suction, positive pressure systems use compressed air to transport materials, making them suitable for longer distances and higher material loads. The system includes a blower or compressor, a material feed hopper, and a pipeline that delivers the material to the destination. The high-pressure air creates a flow that carries the particles through the line, ensuring efficient transportation. Positive pressure systems are often preferred for applications requiring high throughput and the ability to handle abrasive or corrosive materials, as the pressurized pipeline can withstand the stresses of such materials without compromising performance. In the rare earth industry, positive pressure systems are commonly used for transporting concentrated rare earth slurry or powder from processing plants to storage facilities or for further refining, where the need for high capacity and durability is paramount.
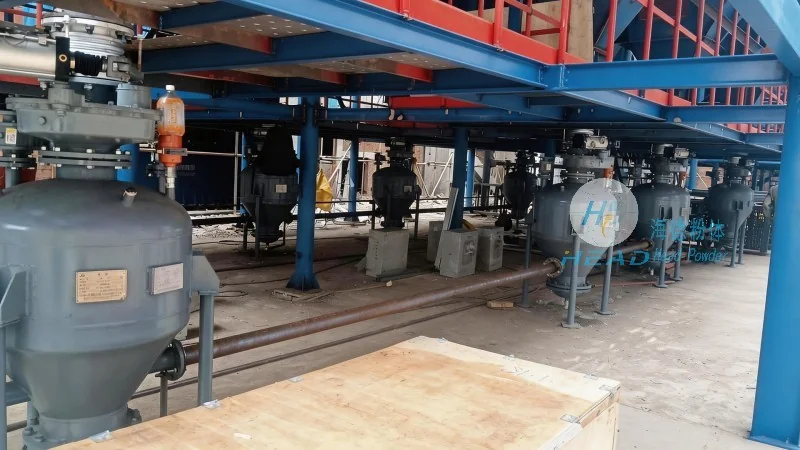
When selecting a pneumatic conveying system for rare earth applications, understanding the differences between negative and positive pressure systems is crucial. Negative pressure systems excel in applications where dust control and low material load are priorities, such as in the initial stages of ore processing where the material is still in a raw or partially processed state. They are also suitable for short-distance transportation from multiple points, as the suction mechanism can effectively draw material from various sources without the need for complex piping. However, negative pressure systems may have limitations in handling high-volume or abrasive materials, as the vacuum pump may struggle to maintain sufficient suction under heavy loads. On the other hand, positive pressure systems are better suited for high-capacity applications and longer distances, making them ideal for transporting processed rare earth materials to storage or for integration into downstream production lines. They can handle higher material loads and are more durable against abrasive particles, but they require careful consideration of air filtration and pressure management to prevent dust emissions and ensure operational safety.
HeadPowder Engineering Co., Ltd., based in Shandong, China, leverages its extensive experience in material handling to provide customized pneumatic conveying solutions for the rare earth industry. The company’s engineers work closely with clients to assess their specific needs, including material characteristics, transportation distances, and environmental requirements, to design systems that optimize efficiency and reliability. For negative pressure applications, HeadPowder offers advanced vacuum pump systems and high-efficiency filtration units that ensure minimal dust emissions and consistent material flow. In positive pressure systems, the company utilizes high-performance blowers and robust pipeline materials to handle abrasive rare earth materials, extending the lifespan of the equipment and reducing maintenance costs. The company’s solutions are designed to meet the stringent standards of the rare earth industry, including compliance with environmental regulations and adherence to safety protocols. By combining cutting-edge technology with practical engineering, HeadPowder delivers systems that enhance productivity, reduce operational costs, and ensure the safe handling of rare earth materials throughout the entire conveying process.
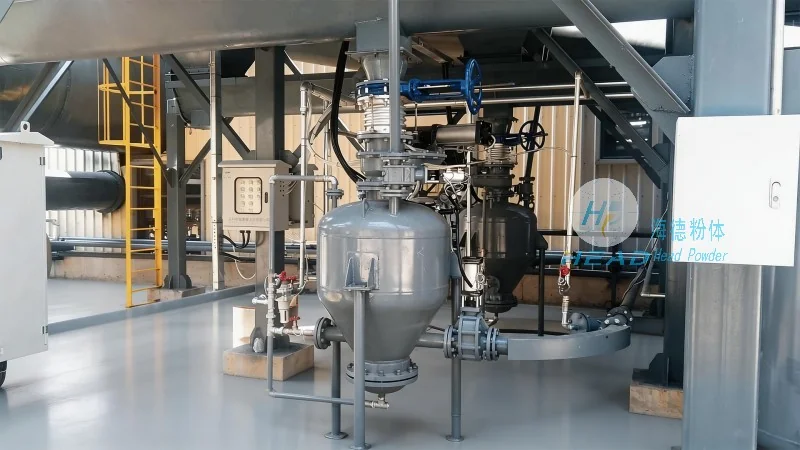
The choice between negative pressure and positive pressure pneumatic conveying systems for rare earth materials depends on the specific requirements of the application, including material characteristics, transportation distance, and environmental considerations. Negative pressure systems are ideal for applications requiring dust control and short-distance transport, while positive pressure systems are better suited for high-capacity and long-distance transportation. HeadPowder Engineering Co., Ltd., with its headquarters in Shandong, China, provides comprehensive solutions that address these needs, leveraging its expertise in material handling to design and implement systems that meet the highest standards of efficiency and reliability. By understanding the principles and applications of both negative and positive pressure pneumatic conveying, businesses in the rare earth industry can make informed decisions to optimize their material handling processes and enhance overall operational performance.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top