Efficient material handling is a critical aspect of modern industrial operations, particularly in the processing of mineral sands. Pneumatic conveying systems have emerged as a versatile and effective solution for transporting bulk materials like mineral sands over short to medium distances. This technology involves the use of air or gas to move particles through a pipeline, offering advantages such as reduced labor costs, improved safety, and the ability to handle materials that are difficult to transport via traditional methods like trucks or conveyor belts.
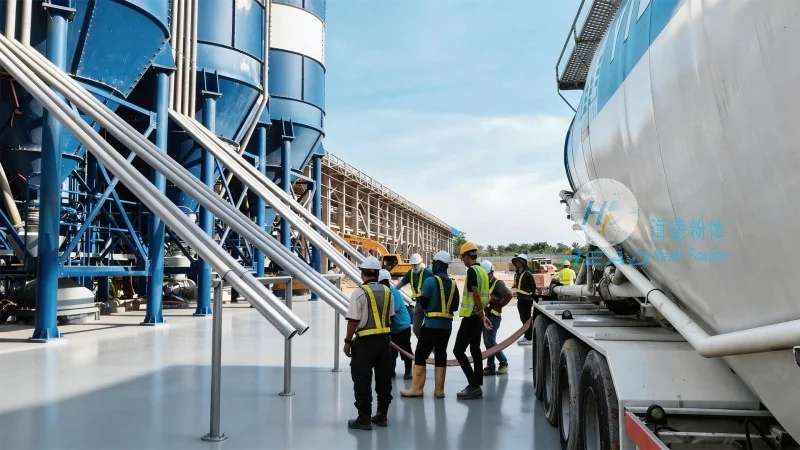
Pneumatic conveying systems for mineral sands can be broadly categorized into two main types: negative pressure (or vacuum) systems and positive pressure systems. Each type has distinct operational principles, advantages, and applications, making them suitable for different industrial scenarios. Understanding these differences is essential for selecting the most appropriate system for a specific mineral sand processing operation.
Negative pressure systems operate by creating a vacuum at the material inlet, drawing the mineral sand particles into the pipeline using air or gas. The primary advantage of this approach is that it allows for the collection of materials from multiple points or even from open storage areas, as the system can pull material into the pipeline without the need for a sealed inlet. This makes negative pressure systems particularly useful in applications where the material source is not enclosed or where multiple collection points are required.
Key components of a negative pressure system include a vacuum pump, a material feed hopper, a filter to separate particles from the air, and a discharge unit. The vacuum pump creates the pressure differential that draws the material into the system. The filter is crucial for maintaining air quality and preventing particle buildup in the system. The discharge unit then delivers the material to the destination, such as a storage silo or processing equipment.
One of the main advantages of negative pressure systems is their ability to handle fine or dusty materials without generating excessive dust emissions. The vacuum helps to contain particles, reducing the risk of airborne contamination. Additionally, these systems are generally quieter and more energy-efficient compared to positive pressure systems, as they rely on the vacuum pump rather than high-pressure air compression.
However, negative pressure systems have some limitations. They are typically more complex to install and maintain due to the need for a vacuum pump and filtration system. The system also requires careful design to ensure that the vacuum is sufficient to draw material from the source without causing excessive air leakage or pressure drops. Furthermore, the capacity of negative pressure systems is generally lower than that of positive pressure systems, making them less suitable for high-volume mineral sand transport over long distances.
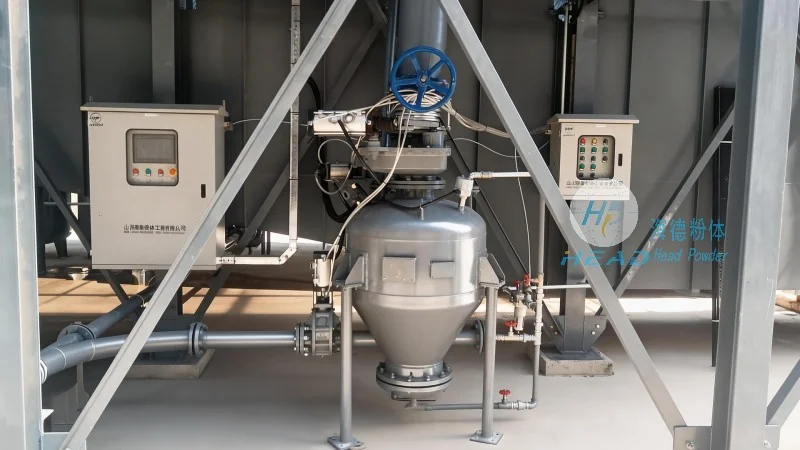
Positive pressure systems, on the other hand, operate by blowing air or gas under pressure into the pipeline, pushing the mineral sand particles forward. This approach is often preferred for applications requiring high material throughput or for transporting materials over longer distances. The system typically includes a blower or compressor, a material feed hopper, a pipeline, and a discharge unit.
The primary advantage of positive pressure systems is their higher capacity and ability to handle larger volumes of material. The high-pressure air provides the necessary force to move particles through the pipeline, making them suitable for long-distance transport and high-demand industrial processes. Additionally, positive pressure systems are generally simpler to install and maintain compared to negative pressure systems, as they do not require a vacuum pump or extensive filtration for the entire system.
However, positive pressure systems have some drawbacks. They tend to generate more dust and noise due to the high-pressure air being expelled from the system. The high pressure can also cause wear and tear on the pipeline and other components, requiring more frequent maintenance. Furthermore, positive pressure systems may not be suitable for handling fine or dusty materials, as the high pressure can cause particles to become airborne and cause contamination issues.
The choice between negative and positive pressure pneumatic conveying systems for mineral sands depends on several factors, including the material characteristics, the distance to be covered, the required throughput, and the operational environment. For example, negative pressure systems are often preferred for applications involving fine or dusty mineral sands where dust control is a priority, or when the material source is not enclosed. Positive pressure systems are more suitable for high-volume transport over longer distances, such as in mining operations where large quantities of mineral sands need to be moved from the mine to processing facilities.
Another important consideration is the system's ability to handle variations in material flow. Both negative and positive pressure systems can be designed with adjustable controls to manage the flow rate, ensuring that the system operates efficiently under varying conditions. This flexibility is crucial in industrial settings where material availability or processing demands may change over time.
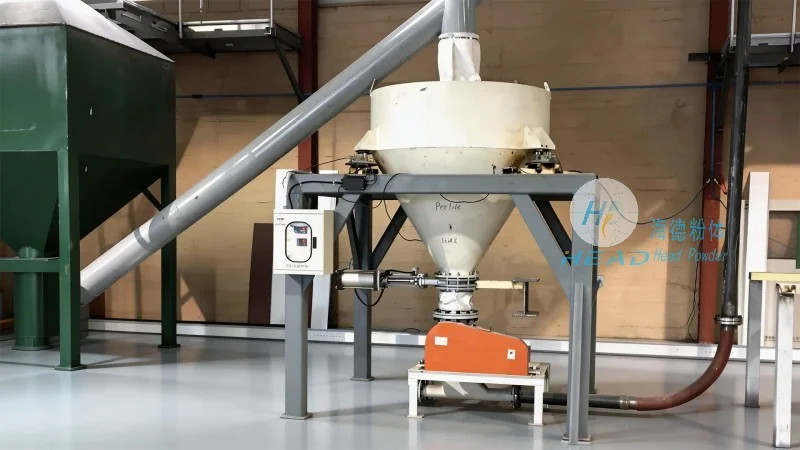
Shandong HeadPowder Engineering Co., Ltd., a leading provider of engineering solutions for mineral processing, has extensive experience in designing and implementing pneumatic conveying systems for mineral sands. The company, based in Shandong, China, has successfully installed and maintained systems for various clients in the mining and processing industries. Their expertise lies in tailoring the system design to meet the specific needs of each project, ensuring optimal performance and efficiency.
For instance, one of their recent projects involved the installation of a negative pressure system for a mineral sand processing plant. The system was designed to handle fine silica sand from an open storage area, with the goal of reducing dust emissions and improving material handling efficiency. The system included a vacuum pump, a large feed hopper, and a high-efficiency filter to ensure clean air discharge. The implementation resulted in significant improvements in material throughput and reduced operational costs for the client.
Another project involved a positive pressure system for a long-distance transport of mineral sands from a mine to a processing facility. The system was designed to handle large volumes of material over a distance of several kilometers. The company's engineers carefully selected a high-capacity blower and optimized the pipeline layout to minimize pressure losses. The system has been operating efficiently for over a year, delivering consistent performance and meeting the client's production targets.
Pneumatic conveying systems, both negative and positive pressure types, play a vital role in the efficient processing and transport of mineral sands. The choice between the two systems depends on the specific requirements of the application, including material characteristics, distance, and throughput. Negative pressure systems offer advantages in dust control and low noise operation, while positive pressure systems excel in high-capacity and long-distance transport.
Companies like Shandong HeadPowder Engineering Co., Ltd. provide specialized engineering solutions to design and implement these systems, ensuring that they meet the unique needs of each industrial operation. By leveraging the appropriate pneumatic conveying technology, mineral sand processing facilities can improve operational efficiency, reduce costs, and enhance safety in their material handling processes.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top