For industries dealing with fine powders, the selection of an appropriate pneumatic conveying system is crucial for efficient material handling and process optimization. This article provides a comprehensive classification and application analysis of fine powder pneumatic conveying systems, focusing on the key factors that influence system design and performance.
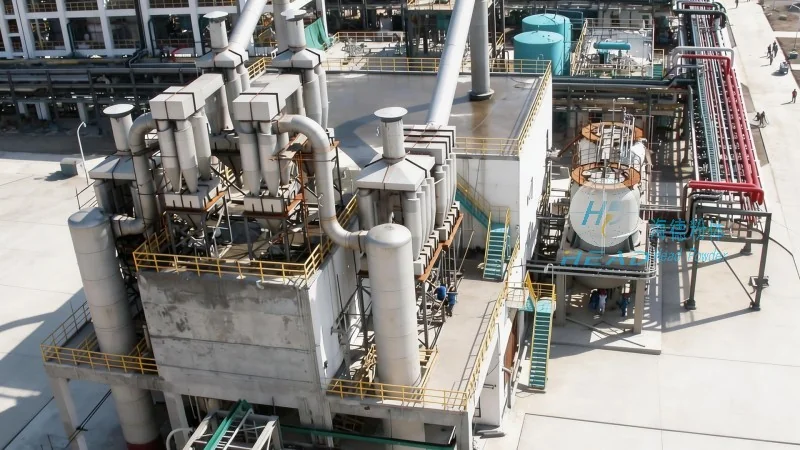
Fine powder pneumatic conveying systems are designed to transport dry powders through a pipeline using air or other gases as the conveying medium. These systems are widely used in various industries, including pharmaceuticals, food processing, chemical manufacturing, and cement production, due to their ability to handle delicate materials without degradation or contamination.
The core principle of pneumatic conveying involves creating a pressure differential between the inlet and outlet of the system, which propels the powder particles along the pipeline. The efficiency and reliability of these systems depend on several critical components, such as the feeder, pipeline, and receiver, each of which must be carefully selected and configured to suit the specific characteristics of the powder being conveyed.
Based on the operating principle and pressure differentials, fine powder pneumatic conveying systems can be broadly classified into two main categories: pressure and vacuum systems.
Pressure Systems operate by generating positive pressure at the inlet, typically using a blower or compressor, to push the powder through the pipeline. These systems are suitable for applications where the material needs to be transported over long distances or through multiple bends. The pressure system is further divided into two subcategories: positive displacement blowers and rotary lobe blowers, which offer high pressure and flow rates for demanding applications.
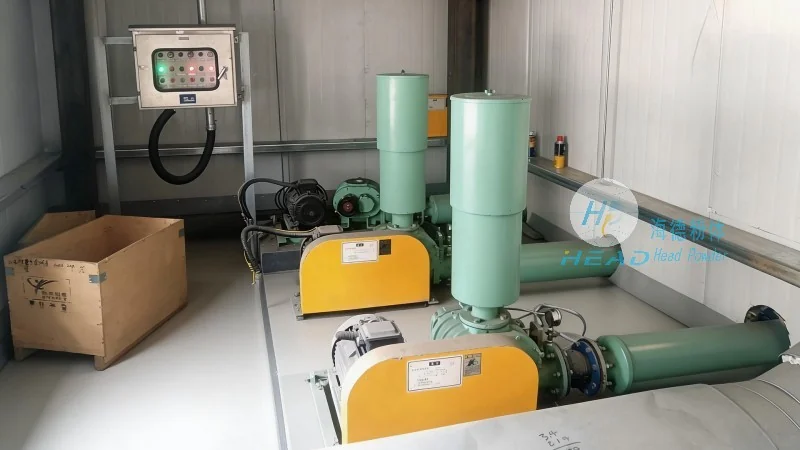
Vacuum Systems, on the other hand, create a negative pressure at the inlet, drawing the powder into the pipeline. This type of system is ideal for applications requiring gentle handling of sensitive powders, as it minimizes particle attrition and degradation. Vacuum systems are commonly used in industries where the material is to be collected from a hopper or silo and transported to a processing unit.
The choice of a fine powder pneumatic conveying system depends on several key factors, including the powder's physical properties, such as particle size, density, and moisture content, as well as the required conveying distance and flow rate. Other considerations include the system's energy efficiency, maintenance requirements, and the need for dust control and environmental compliance.
For example, in pharmaceutical applications, where the powder must be handled under sterile conditions, a vacuum system with a closed-loop design is often preferred to prevent contamination. In contrast, in cement manufacturing, where high-volume and high-pressure conveying is required, a pressure system with a positive displacement blower may be more suitable.
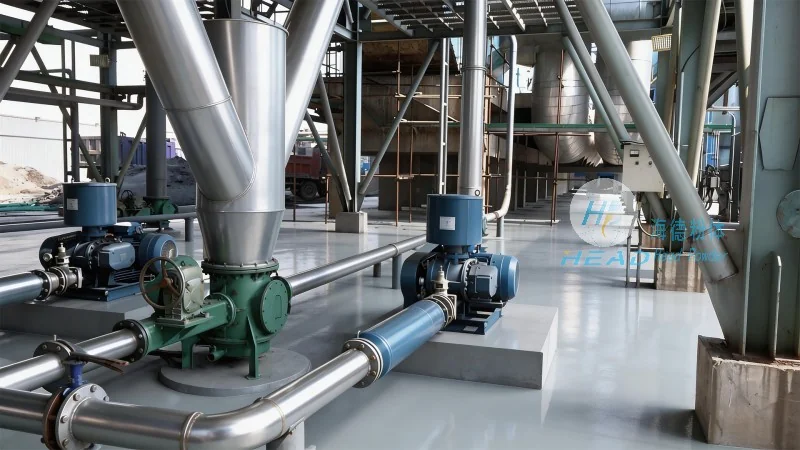
Fine powder pneumatic conveying systems are applied in a wide range of industries, each with specific requirements that dictate the system configuration. In the food industry, for instance, systems are used to handle powders like flour, sugar, and cocoa, ensuring that the product remains free from moisture and contaminants. The use of stainless steel components and sanitary design is critical in these applications to meet regulatory standards.
In the chemical industry, systems are used to transport reactive powders, such as catalysts and pigments, where the risk of explosion or fire is a concern. The selection of appropriate materials for the pipeline and components, such as explosion-proof motors and flame arrestors, is essential to ensure safety and compliance with industry regulations.
In the cement industry, pneumatic conveying systems are used to transport raw materials like limestone and clinker from storage silos to the kiln. The high-pressure, high-volume nature of these systems requires robust components and efficient control systems to maintain consistent flow rates and prevent blockages.
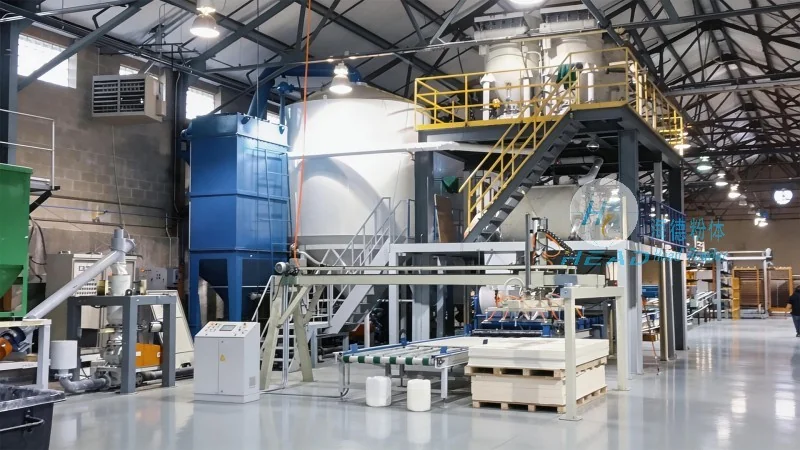
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a leading manufacturer of fine powder pneumatic conveying systems. With a strong focus on innovation and quality, the company has developed advanced solutions tailored to the specific needs of various industries.
Headpowder's expertise lies in designing and manufacturing customized pneumatic conveying systems that meet the unique requirements of each client. The company's team of engineers and technicians works closely with customers to understand their process challenges and provide tailored solutions, ensuring optimal performance and reliability.
Headpowder's systems are known for their high efficiency, low maintenance, and energy-saving features. The company uses advanced materials and manufacturing techniques to ensure durability and long service life, reducing downtime and operational costs for its clients.
Headquartered in Shandong, China, headpowder serves customers worldwide, providing comprehensive support from system design and installation to maintenance and after-sales service. The company's commitment to quality and customer satisfaction has earned it a reputation as a trusted partner in the fine powder handling industry.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top