Organic fertilizer granule pneumatic conveying is a specialized method used in the agricultural and fertilizer processing industries to transport granular organic fertilizers efficiently. This technology involves using air or gas to move the fertilizer particles through a pipeline system, eliminating the need for traditional mechanical conveyors like belts or screws. The process is particularly beneficial for handling organic materials that are prone to dust, clumping, or require gentle handling to maintain their quality and structure.
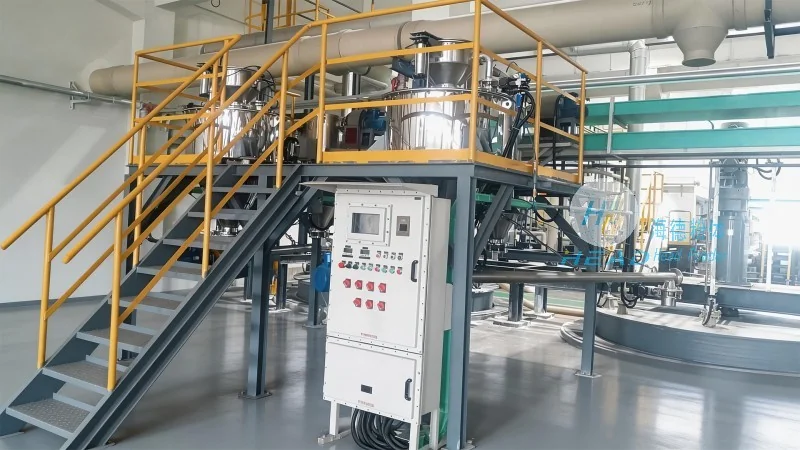
Pneumatic conveying systems for organic fertilizer granules operate by creating a flow of air within a closed pipeline. The system typically consists of a blower or compressor that generates the necessary air pressure, a hopper or feeder to introduce the granules into the system, and a discharge point where the material is released. The key advantage of this method is its ability to handle materials that are difficult to transport using conventional methods, such as those with high moisture content or irregular shapes. By using air as the conveying medium, the system minimizes material degradation and ensures a consistent flow rate, which is crucial for maintaining the quality of organic fertilizers.
The design of an organic fertilizer granule pneumatic conveying system is based on several critical principles to ensure optimal performance and efficiency. First, the system must be designed to handle the specific physical properties of the organic fertilizer granules, including their size, density, and moisture content. These factors influence the air velocity required to move the particles and the pressure drop across the system. Engineers at Shandong HeadPowder Engineering Co., Ltd. carefully analyze these parameters to select the appropriate blower capacity and pipeline dimensions. Second, the system must incorporate features to prevent material degradation and clogging. This includes using smooth, corrosion-resistant materials for the pipeline and components, as well as incorporating air filters and cyclone separators to remove dust and prevent blockages. Third, the design must consider the energy efficiency of the system. By optimizing the air velocity and pressure, the system minimizes energy consumption while maintaining the required conveying capacity. The company’s expertise in engineering ensures that each system is tailored to the specific needs of the client, balancing performance, durability, and cost-effectiveness.
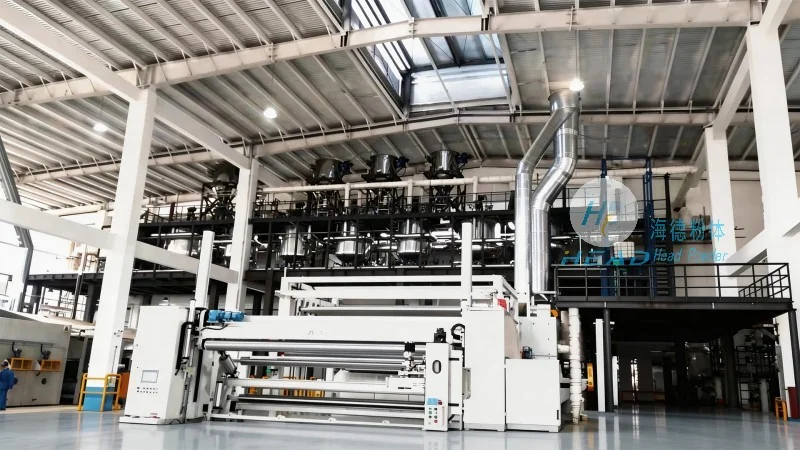
A typical organic fertilizer granule pneumatic conveying system includes several key components, each playing a vital role in the overall operation. The blower or compressor is the primary source of air pressure, providing the force needed to move the granules through the pipeline. The hopper or feeder is responsible for feeding the granules into the system at a controlled rate, preventing overloading and ensuring a steady flow. The pipeline itself is designed to withstand the pressure and temperature of the conveying process, with smooth internal surfaces to minimize friction and reduce the risk of material buildup. Cyclone separators are often used at the discharge end to separate the fertilizer granules from the air stream, allowing the granules to be collected in a hopper or storage bin while the air is discharged back into the system or to the atmosphere. Air filters are also essential to remove any fine particles that may have escaped the cyclone, maintaining air quality and preventing contamination of the fertilizer. The design of these components is critical to the overall efficiency and reliability of the system, and Shandong HeadPowder Engineering Co., Ltd. specializes in selecting and integrating these parts to create a robust and effective solution.
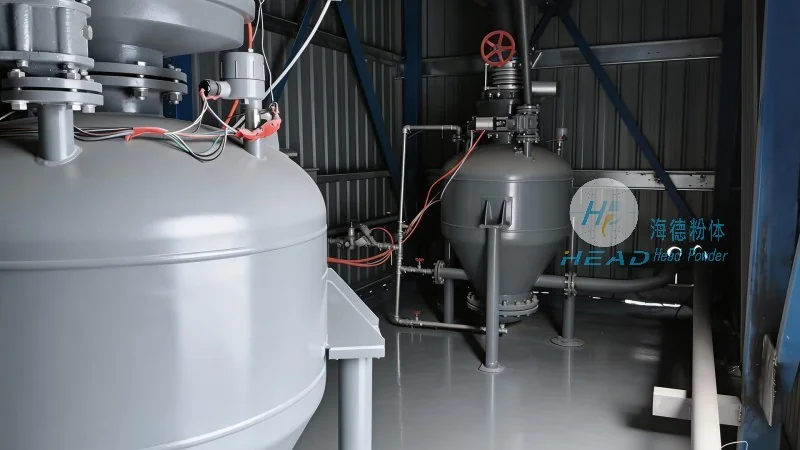
Implementing a pneumatic conveying system for organic fertilizer granules offers numerous benefits for both manufacturers and end-users. For manufacturers, the system improves operational efficiency by reducing downtime caused by clogging or material degradation. It also enhances product quality by minimizing the risk of contamination and maintaining the granules’ physical properties. The system’s ability to handle large volumes of material quickly and consistently supports higher production rates and better inventory management. For end-users, the use of a pneumatic conveying system ensures that the organic fertilizer is delivered in a clean, uniform state, which is essential for optimal plant growth and soil health. The gentle handling of the granules also preserves their nutrient content, ensuring that the fertilizer remains effective throughout its shelf life. Additionally, the system’s energy efficiency contributes to lower operational costs, making it a cost-effective solution for long-term use.
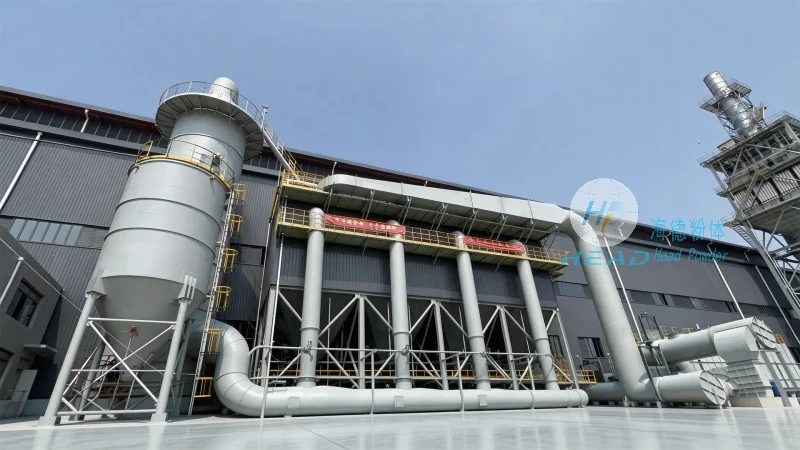
Organic fertilizer granule pneumatic conveying systems are widely used in various industries, particularly in the agricultural and fertilizer processing sectors. These systems are commonly employed in large-scale fertilizer production facilities where high volumes of organic granules need to be transported between processing stages, such as from mixing and granulation to packaging and storage. The technology is also used in composting facilities, where organic waste is converted into fertilizer and then conveyed to storage or distribution points. Additionally, the system is beneficial in greenhouse and nursery operations, where precise and efficient delivery of organic fertilizers is crucial for maintaining plant health and productivity. The versatility of pneumatic conveying makes it suitable for a range of applications, from small-scale farm operations to large industrial facilities, and the expertise of companies like Shandong HeadPowder Engineering Co., Ltd. ensures that systems can be customized to meet the specific needs of each client, regardless of the scale or complexity of the application.
In conclusion, organic fertilizer granule pneumatic conveying is a sophisticated and effective method for transporting organic fertilizers, and its success depends on a well-designed system that adheres to key principles. The design must consider the physical properties of the granules, incorporate features to prevent degradation and clogging, and optimize energy efficiency. Companies like Shandong HeadPowder Engineering Co., Ltd. play a critical role in developing and implementing these systems, leveraging their engineering expertise to create solutions that meet the specific requirements of their clients. By understanding and applying the core design principles, manufacturers can enhance operational efficiency, improve product quality, and reduce costs, ultimately contributing to the sustainability and productivity of the agricultural and fertilizer industries. The continued development and refinement of pneumatic conveying technology will likely lead to even more efficient and effective systems in the future, further supporting the growth and success of the organic fertilizer market.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top