Efficient and reliable transport of fertilizer granules is a critical aspect of modern agricultural operations. Pneumatic conveying systems have emerged as a preferred solution for handling bulk materials like fertilizer, offering advantages such as reduced labor costs, minimized product damage, and enhanced safety. This article explores the different types of pneumatic conveying systems commonly used in fertilizer granule transport and their practical applications, highlighting the expertise of Shandong HeadPowder Engineering Co., Ltd. in providing tailored solutions for the industry.
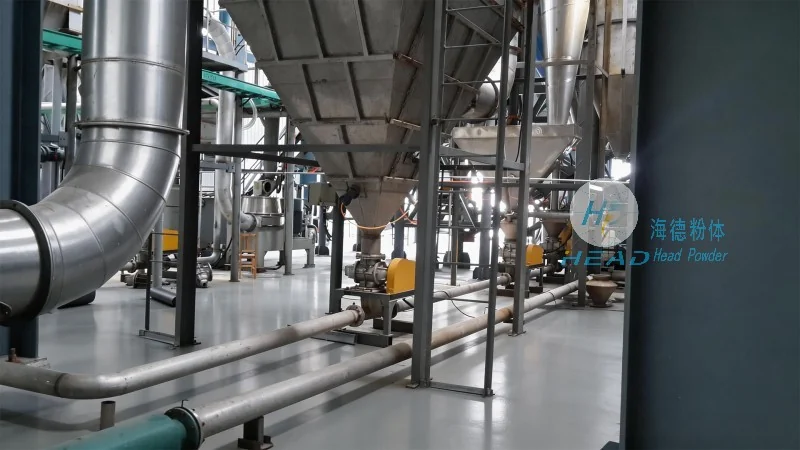
There are primarily three types of pneumatic conveying systems utilized in fertilizer granule transport: positive pressure, negative pressure, and mixed pressure systems. Each type has distinct characteristics and is suitable for different operational requirements.
Positive pressure systems operate by blowing air or gas into the conveying line, pushing the material forward. This method is ideal for long-distance transport and can handle abrasive materials without causing excessive wear. The system typically uses a blower or compressor to generate the necessary pressure, ensuring consistent material flow. Positive pressure systems are often preferred for applications where the material needs to be transported over significant distances or through complex piping networks.
Negative pressure systems, on the other hand, draw material into the conveying line using a vacuum created by a fan or ejector. This approach is suitable for short to medium distances and is commonly used in applications where the material is sensitive to pressure changes or where dust control is a priority. Negative pressure systems are particularly effective for handling fine or dusty materials, as they minimize the risk of product degradation and environmental contamination.
Mixed pressure systems combine elements of both positive and negative pressure systems. They use a combination of a blower to push material and a vacuum to assist in material pickup. This hybrid approach offers flexibility and can be optimized for various operational conditions. Mixed pressure systems are often used in applications requiring both long-distance transport and the ability to handle a wide range of material types, including bulk and fine granules.
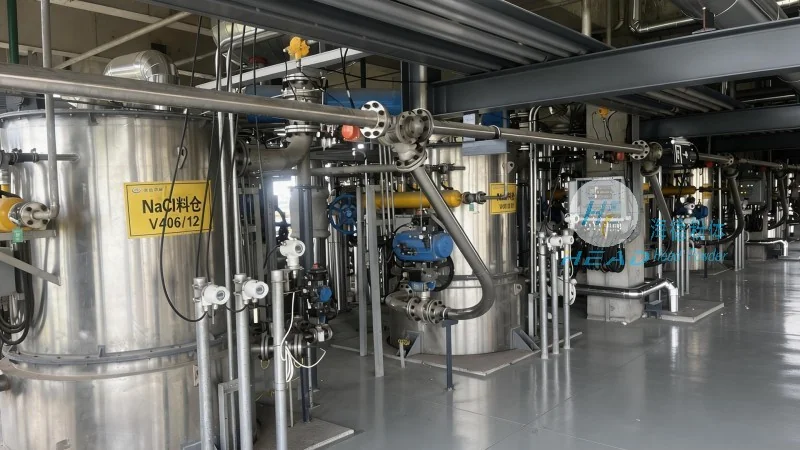
Shandong HeadPowder Engineering Co., Ltd. specializes in designing and implementing pneumatic conveying systems tailored to the specific needs of fertilizer manufacturers and distributors. The company's expertise lies in understanding the unique challenges of fertilizer granule transport, such as material variability, moisture content, and the need for dust-free handling.
One practical application is the transport of fertilizer granules from storage silos to processing facilities. The positive pressure system, for instance, can efficiently move large volumes of granules over long distances, ensuring a continuous supply to the production line. This reduces downtime and improves overall operational efficiency. The system's ability to handle abrasive materials without significant wear and tear makes it suitable for long-term use in fertilizer processing plants.
Another application involves the distribution of fertilizer granules to agricultural fields. Negative pressure systems are often employed in this scenario to minimize dust emissions and protect the environment. The vacuum created by the system draws granules from storage tanks and transports them to application equipment, ensuring precise and controlled distribution. This method is particularly beneficial for organic fertilizers or those with high moisture content, as it prevents product clumping and maintains consistent quality.
Shandong HeadPowder Engineering Co., Ltd. also provides solutions for bulk handling and storage, where mixed pressure systems are utilized to transport granules between storage silos and packaging lines. The hybrid approach allows for efficient material transfer while maintaining the integrity of the fertilizer product. The company's engineers work closely with clients to assess their operational requirements, material characteristics, and site conditions to design a system that maximizes performance and minimizes operational costs.
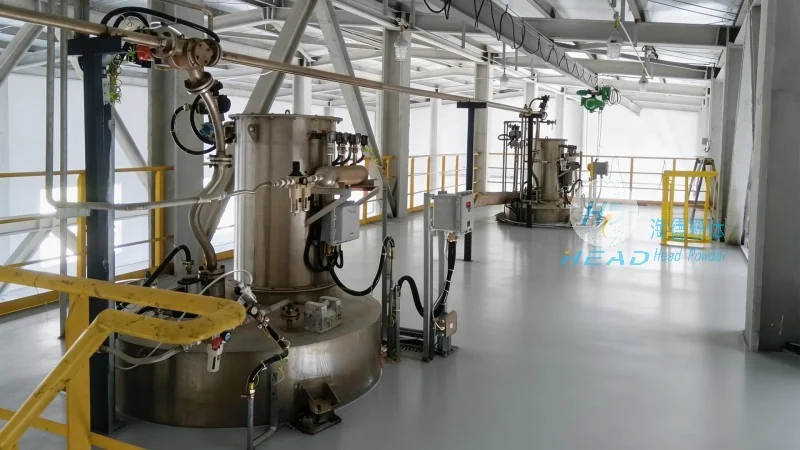
Implementing pneumatic conveying systems for fertilizer granule transport offers several key benefits. Firstly, these systems enhance operational efficiency by automating the material handling process, reducing the need for manual labor and minimizing the risk of human error. This leads to increased productivity and lower labor costs over time.
Secondly, pneumatic conveying systems minimize product damage and degradation. Unlike mechanical conveyors, which can cause abrasion and breakage, pneumatic systems use air to move materials, preserving the granule size and quality. This is crucial for fertilizers, as particle size and uniformity directly impact their effectiveness in soil.
Thirdly, these systems improve safety and environmental compliance. By containing dust and preventing product spillage, pneumatic conveying reduces the risk of respiratory issues and environmental contamination. This is particularly important for fertilizer granules, which can be dusty and potentially hazardous if not handled properly.
Additionally, pneumatic conveying systems offer flexibility and scalability. They can be easily integrated into existing infrastructure and adapted to changing operational needs, such as increased production capacity or expanded distribution networks. This makes them a long-term investment for fertilizer manufacturers and distributors looking to enhance their operational capabilities.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top