Pneumatic conveying systems have become a cornerstone in the efficient handling and transportation of cereal products, offering a reliable and flexible solution for moving materials like flakes, grains, and other processed cereals from one point to another within a production facility or between different stages of processing. These systems utilize air as the conveying medium, transporting bulk materials through a network of pipes, which can be crucial for maintaining product quality, hygiene, and operational efficiency in the cereal industry.
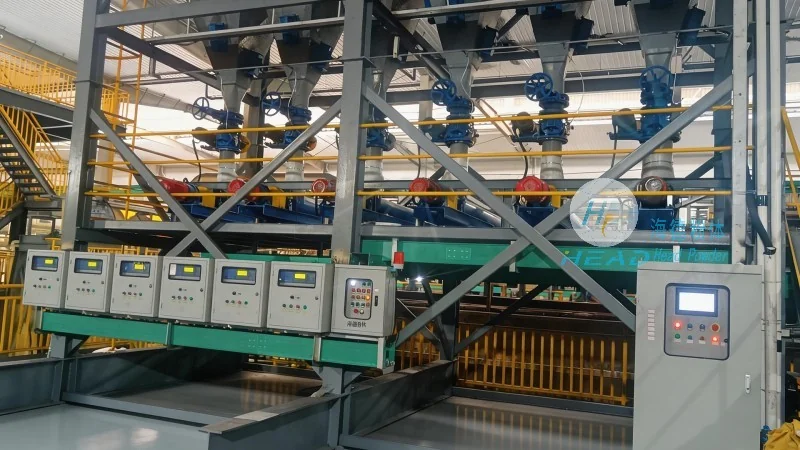
Several types of pneumatic conveying systems are commonly employed in cereal transportation, each with distinct characteristics and applications. The primary categories include:
1. **Positive Pressure Systems**: These systems generate air pressure within the conveying line using a blower or fan, pushing the material forward. They are ideal for short to medium distances and can handle a wide range of materials, including delicate cereals that require gentle handling to prevent breakage.
2. **Negative Pressure (Vacuum) Systems**: In these systems, a vacuum is created at the receiving end, drawing material into the system. This method is suitable for applications where the material needs to be transported from multiple sources or where the receiving point is lower than the source.
3. **Combination (Bi-Directional) Systems**: These systems can operate in both positive and negative pressure modes, providing flexibility in material handling. They are often used in complex production lines where materials need to be transported in both directions or where the system needs to adapt to varying production demands.
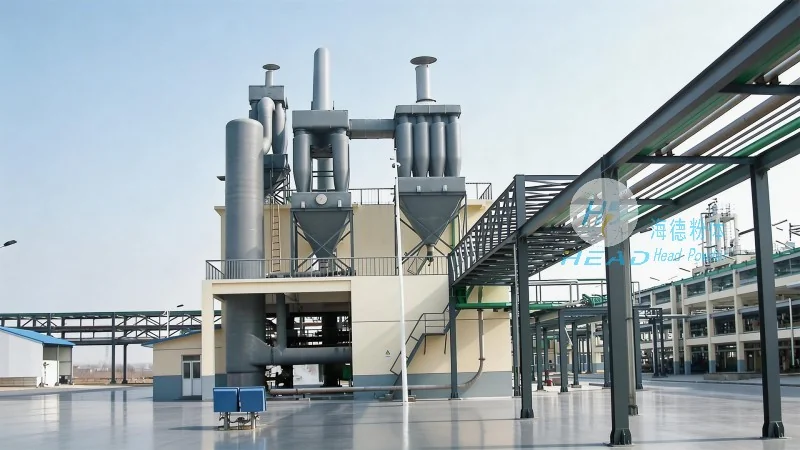
The practical applications of pneumatic conveying systems in cereal handling are diverse and essential for modern production lines. For instance, in the production of breakfast cereals, these systems are used to transport raw grains from storage silos to processing equipment, ensuring a continuous and controlled flow. During the processing stage, they can move intermediate products like milled cereals or flaked materials between different processing units, such as extruders, dryers, and packaging machines.
In addition, pneumatic conveying is widely used in the packaging and distribution phases. After the final product is formed, the system can transport the finished cereal products from the packaging line to storage or shipping areas, maintaining product integrity and preventing contamination. This is particularly important for products that are sensitive to moisture or temperature changes, as the enclosed system minimizes exposure to external factors.
When selecting a pneumatic conveying system for cereal transportation, several factors must be considered to ensure optimal performance and efficiency. These include the type and properties of the cereal material (e.g., particle size, moisture content, and density), the distance and layout of the production facility, and the required flow rate and capacity. The system must also be designed to maintain product quality, with features such as gentle handling to avoid breakage, and effective cleaning to prevent product contamination.
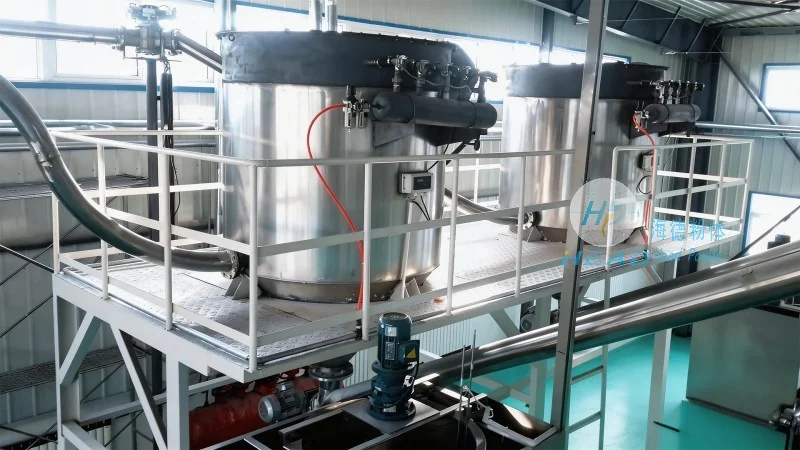
Additionally, the choice between positive and negative pressure systems depends on the specific operational requirements. Positive pressure systems are generally preferred for short to medium distances and when the material needs to be moved from a lower to a higher elevation, as they can generate sufficient pressure to overcome gravity and friction. Negative pressure systems, on the other hand, are more suitable for long-distance or horizontal transport, especially when the receiving point is lower than the source, as the vacuum can effectively draw the material.
As a leading provider in the field, Shandong HeadPowder Engineering Co., Ltd. specializes in designing, manufacturing, and installing customized pneumatic conveying systems tailored to the unique needs of the cereal industry. With a strong focus on quality and innovation, the company has built a reputation for delivering reliable and efficient solutions that enhance productivity and product quality for its clients.
HeadPowder, as the company is commonly known, offers a range of services, including system design, material handling consulting, and after-sales support. The company's expertise lies in understanding the specific challenges faced by cereal producers, such as maintaining product integrity during transport, ensuring hygienic conditions, and optimizing operational costs. By leveraging advanced technology and years of industry experience, HeadPowder provides tailored solutions that meet the exact requirements of each client.
HeadPowder Engineering is located in Shandong, China, providing a strategic base for serving clients both domestically and internationally. The company's address is in Shandong, China, and it operates with a commitment to excellence in every aspect of its operations, from initial consultation to final installation and ongoing support.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top