When it comes to handling bulk materials efficiently, especially in industrial settings where large quantities of powders or granules need to be transferred from ton bags to processing equipment, a ton bag unloading station with a pneumatic conveying system offers a robust and reliable solution. This technology has become a cornerstone in many industries, including chemical, food processing, and pharmaceuticals, where material handling demands precision, safety, and minimal contamination. The core of this system lies in its ability to automate the transfer of bulk materials from sealed ton bags into a processing line, all while maintaining the integrity of the material and ensuring a clean, dust-free operation.
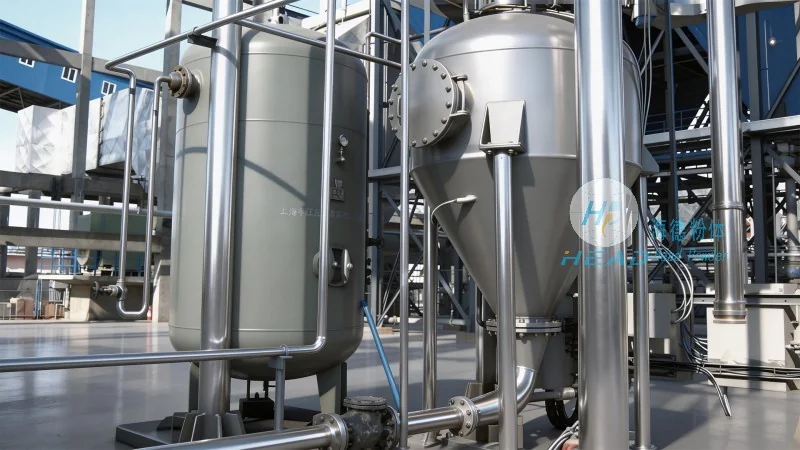
A ton bag unloading station equipped with a pneumatic conveying system is a specialized piece of equipment designed to receive bulk materials from large, flexible containers known as ton bags. These bags typically hold 1 ton (or more) of material and are sealed to prevent spillage and contamination. The system’s primary function is to safely and efficiently unload the contents of these bags into a storage silo, hopper, or directly into a processing machine. The pneumatic conveying aspect involves using air pressure to move the material through a network of pipes, ensuring that the material is transported without direct contact with the conveying system, which helps maintain product purity and reduces the risk of cross-contamination.
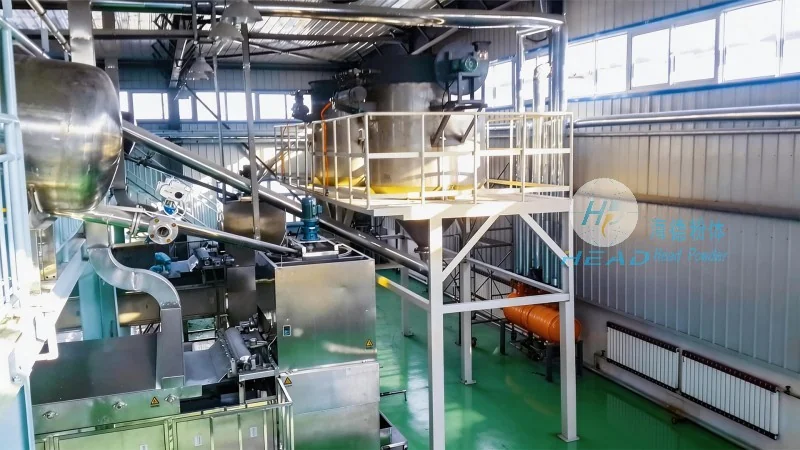
The design of a ton bag unloading station pneumatic conveying system is based on several key principles that ensure optimal performance, safety, and efficiency. First, the system must be capable of handling a wide range of materials, from fine powders to coarse granules, without clogging or damaging the equipment. This is achieved through careful selection of components such as the hopper design, material feed mechanisms, and the type of air mover (e.g., rotary lobe blowers, positive displacement blowers). Second, the system prioritizes safety by incorporating features like explosion-proof designs for hazardous materials, dust collection systems to maintain air quality, and interlocks to prevent accidental operation. Third, the design focuses on minimizing material loss and contamination. This includes using sealed bag handling mechanisms, efficient dust filtration, and proper material flow control to ensure that the transferred material is as pure as possible. Additionally, the system is engineered for ease of maintenance, with accessible components and clear operational indicators to facilitate regular upkeep and troubleshooting.
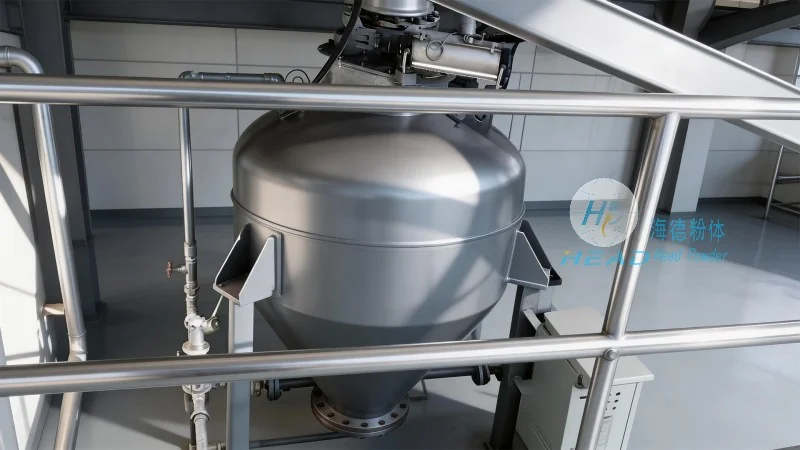
At the heart of a ton bag unloading station pneumatic conveying system are several critical components that work in tandem to achieve the desired material transfer. The primary components include the bag opening and sealing mechanism, the material hopper and feeder, the air mover (blower), the conveying pipeline, and the dust collection system. The bag opening mechanism typically involves a hydraulic or mechanical system that safely cuts open the top of the ton bag without damaging the contents. The material hopper, often equipped with a rotary valve or screw feeder, acts as a buffer to regulate the flow of material into the conveying system, preventing overloading and ensuring a steady feed. The air mover provides the necessary pressure to transport the material through the pipeline, with the choice of blower type depending on the material characteristics and system requirements. The conveying pipeline is designed with smooth, corrosion-resistant materials to minimize friction and material buildup, and the system may include bends, elbows, and filters to maintain consistent airflow and material transport. Finally, the dust collection system, often integrated with the air mover, captures any airborne particles, ensuring that the environment remains clean and safe for operators and equipment.
The ton bag unloading station pneumatic conveying system is widely used across various industries due to its versatility and efficiency. In the chemical industry, it is used to handle powders and granules that may be hazardous or reactive, requiring a sealed and controlled transfer process. In the food and pharmaceutical sectors, the system’s ability to maintain product purity and prevent contamination is crucial, as even small amounts of impurities can affect product quality and safety. The benefits of this system extend beyond material handling; it also improves operational efficiency by reducing manual labor, minimizing downtime, and ensuring a consistent supply of materials to processing equipment. Additionally, the system’s compact design allows for installation in existing facilities, making it a cost-effective solution for upgrading or expanding material handling capabilities.
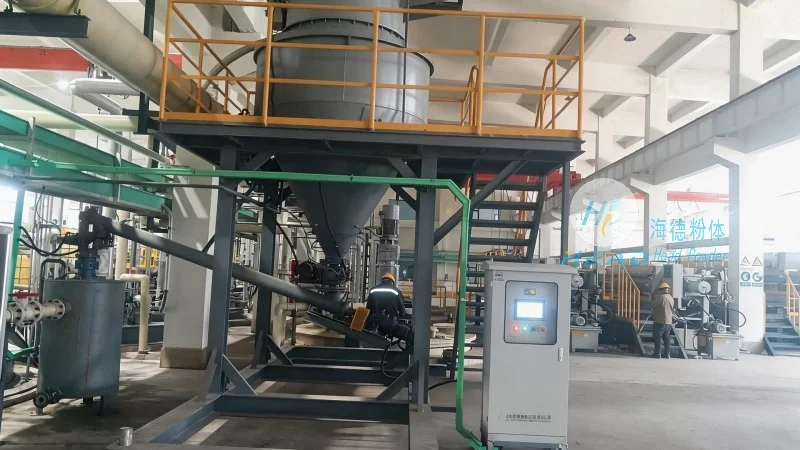
One of the key advantages of the ton bag unloading station pneumatic conveying system is its adaptability to different industrial needs. Companies like Shandong HeadPowder Engineering Co., Ltd. specialize in designing and manufacturing customized systems that integrate seamlessly with existing processing lines. The system can be tailored to handle specific material types, such as fine powders, coarse granules, or even sticky or abrasive materials, by adjusting components like the hopper design, feeder type, and air mover capacity. Furthermore, the system can be integrated with other equipment, such as silos, mixers, or packaging machines, to create a fully automated material handling line. This customization ensures that the system meets the unique requirements of each client, whether they are processing chemicals, food products, or pharmaceuticals. The engineering team at Shandong HeadPowder Engineering Co., Ltd. works closely with clients to understand their specific needs and design a system that maximizes efficiency and minimizes operational challenges.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top