Automatic pneumatic conveying systems are advanced industrial solutions designed to transport bulk materials efficiently and safely. These systems utilize compressed air or other gases to move powders, granules, and other particulate materials from one location to another. As a leading manufacturer in the field, Shandong HeadPowder Engineering Co., Ltd. specializes in providing customized solutions that meet diverse industrial needs.
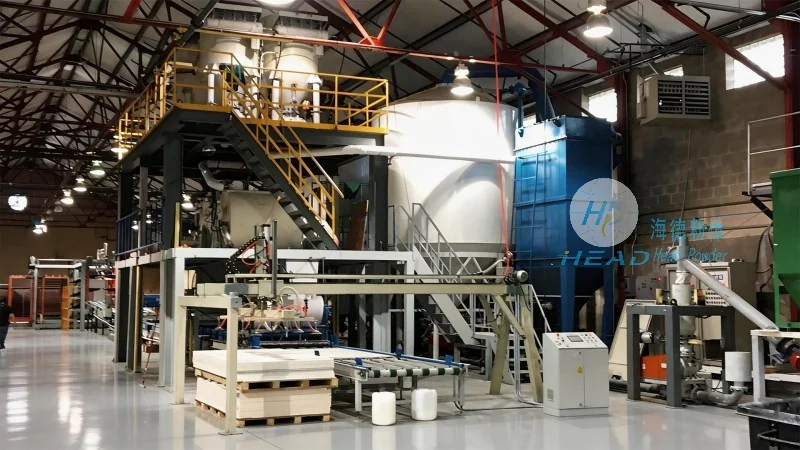
Pneumatic conveying systems operate by creating a pressure differential between the material source and the destination. The system typically consists of a hopper, a conveyor line, and a receiver. The material is fed into the hopper, where it is then drawn into the conveyor line by the moving air. This process allows for the seamless transfer of materials without the need for mechanical components like belts or chains, reducing maintenance and operational costs.
The design of an effective pneumatic conveying system involves several critical principles. First, the system must be capable of handling the specific properties of the material being transported—such as particle size, density, and moisture content. This is achieved through the selection of appropriate air velocities and system pressures. Second, the system must ensure minimal material degradation and product contamination. This is often accomplished by using smooth, corrosion-resistant materials for the conveyor lines and incorporating filtration systems to maintain air quality.
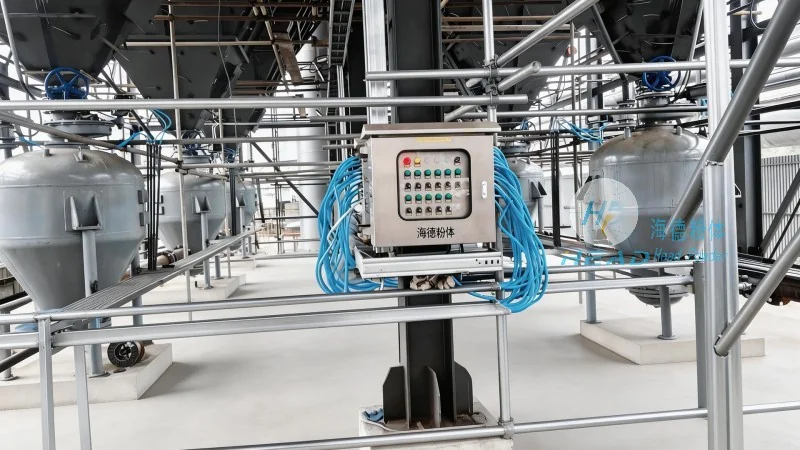
At the heart of a pneumatic conveying system are several key components. The hopper serves as the material storage and feeding unit, ensuring a consistent flow of material into the system. The conveyor line, which can be either positive or negative pressure, is responsible for transporting the material. The receiver collects the material at the destination and may include a discharge valve for controlled release. Additionally, the system includes air compressors or vacuum pumps to generate the necessary pressure, and control valves to regulate air flow and pressure.
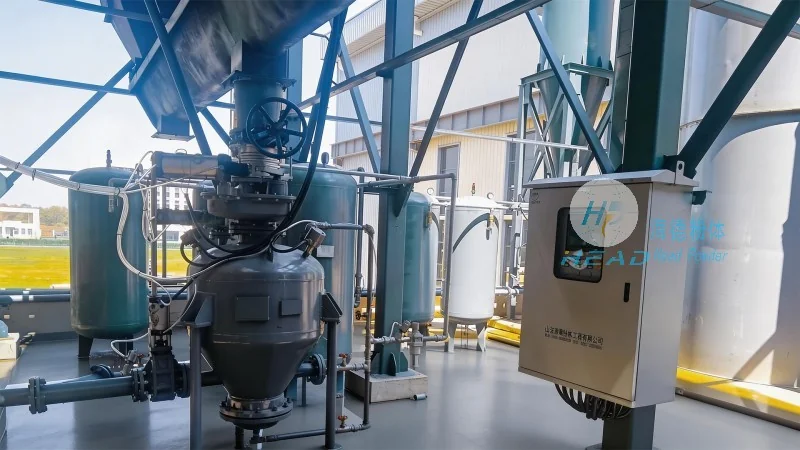
Pneumatic conveying systems are widely used in various industries, including food processing, pharmaceuticals, chemicals, and minerals. The primary benefits of these systems include improved safety (as there are no moving parts exposed to operators), reduced labor costs (due to automated operation), and enhanced product quality (by minimizing contamination and degradation). Shandong HeadPowder Engineering Co., Ltd. has developed specialized systems tailored to the unique requirements of each industry, ensuring optimal performance and reliability.
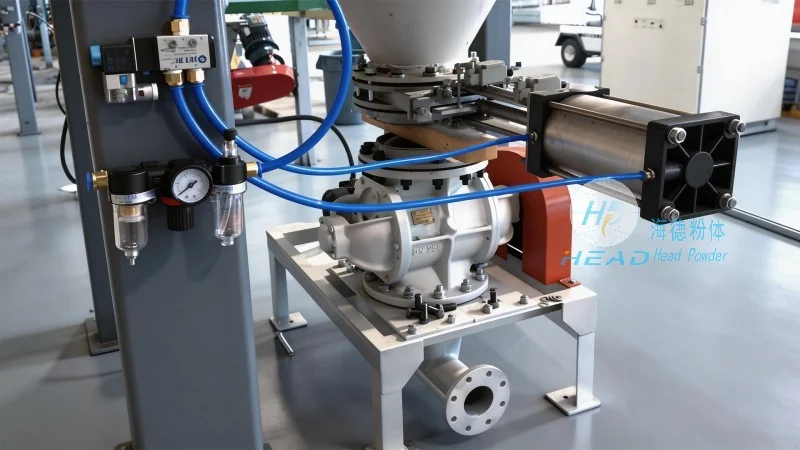
Given the diverse nature of industrial applications, pneumatic conveying systems are often customized to meet specific operational needs. Factors such as material characteristics, distance to be transported, and environmental conditions are all considered during the design phase. Regular maintenance is also crucial to ensure the longevity and efficiency of the system. This includes checking air filters, inspecting conveyor lines for wear, and verifying the performance of the air compressor or vacuum pump.
Automatic pneumatic conveying systems represent a significant advancement in material handling technology. By leveraging compressed air to transport materials, these systems offer a safe, efficient, and cost-effective alternative to traditional methods. Shandong HeadPowder Engineering Co., Ltd., with its expertise and commitment to quality, continues to provide innovative solutions that enhance operational efficiency across various industries. The design principles and components discussed above are fundamental to the success of these systems, and with proper implementation and maintenance, they can deliver reliable performance for years to come.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top