Compound fertilizer is a critical input in modern agriculture, and efficient handling and transportation of this material is essential for optimizing production processes. The pneumatic conveying system is a key technology used in the fertilizer industry to transport bulk materials like compound fertilizer from one location to another. This article provides a technical analysis of compound fertilizer pneumatic conveying systems, focusing on the comparison between positive pressure and negative pressure conveying modes. The discussion is based on the expertise of Shandong HeadPowder Engineering Co., Ltd., a leading company in the field, with its headquarters located in Shandong, China.
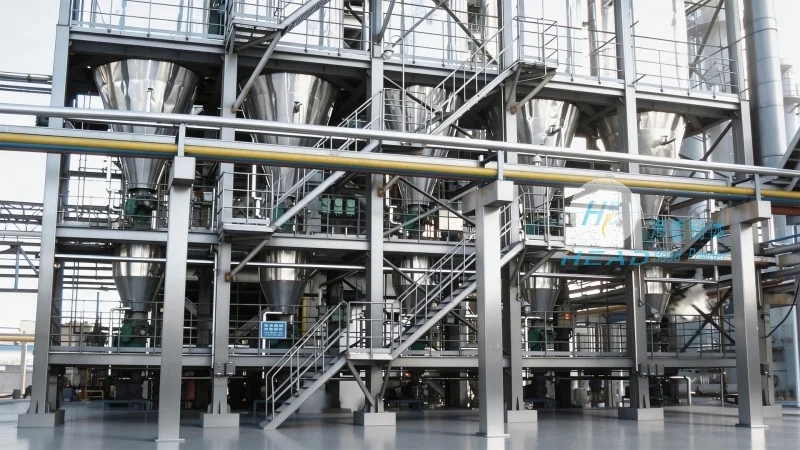
Compound fertilizer pneumatic conveying systems are designed to transport granular or powdered materials such as compound fertilizer through a pipeline using air or gas as the conveying medium. These systems are widely used in the fertilizer industry due to their ability to handle large volumes of material with minimal manual intervention. The core components of a typical pneumatic conveying system include a material hopper, a conveyor pipeline, a fan or blower, and a discharge unit. The system operates by creating a pressure differential to move the material through the pipeline. The choice of conveying mode—positive pressure or negative pressure—significantly impacts the system's performance, efficiency, and cost.
Positive pressure conveying, also known as pressure pneumatic conveying, involves blowing air or gas into the conveying pipeline to create a pressure higher than the ambient air pressure. This mode is commonly used for transporting materials over long distances or through complex pipeline networks. The system typically includes a high-pressure blower or fan that generates the necessary pressure to move the material. In a positive pressure system, the material is drawn from the hopper and propelled through the pipeline by the high-pressure air. This mode is particularly effective for handling abrasive or corrosive materials, as the high-pressure air can help to break up agglomerates and ensure consistent flow. The positive pressure conveying mode is often preferred for applications where the material needs to be transported to multiple destinations or where the system is integrated with other processing equipment.
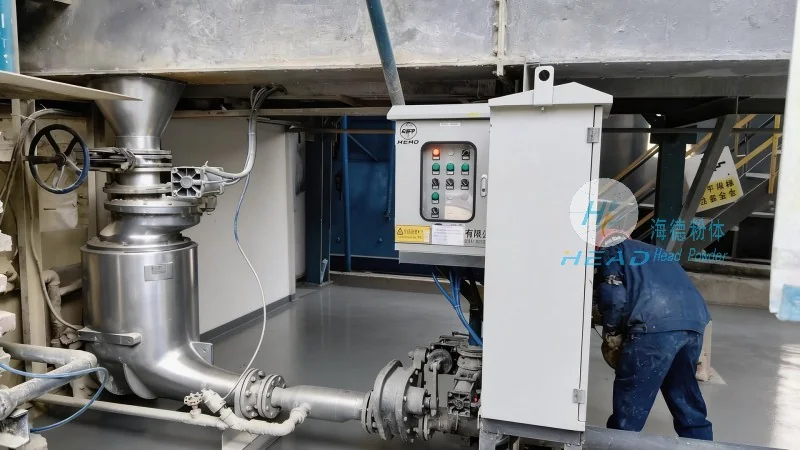
Negative pressure conveying, or vacuum pneumatic conveying, operates by creating a vacuum in the conveying pipeline, which draws the material from the hopper and pulls it through the pipeline. This mode is commonly used for short to medium-distance transportation and for handling materials that are sensitive to pressure or temperature changes. The system includes a vacuum pump or fan that creates the low-pressure environment necessary for material transport. In a negative pressure system, the material is drawn into the pipeline by the vacuum, and the air is then filtered and released back into the atmosphere. This mode is particularly effective for handling fine powders or materials that are prone to dust generation, as the vacuum helps to contain the material and prevent dust dispersion. The negative pressure conveying mode is often preferred for applications where the material needs to be transported from a single source to a single destination, or where the system is used in enclosed environments to maintain air quality.
When comparing positive pressure and negative pressure conveying modes, several factors need to be considered, including system efficiency, material handling capabilities, cost, and environmental impact. Positive pressure systems generally offer higher conveying rates and can handle larger volumes of material compared to negative pressure systems. However, they require more energy to operate due to the high-pressure air requirements. Negative pressure systems, on the other hand, are more energy-efficient and can handle fine powders more effectively, but they have lower conveying rates and are more suitable for shorter distances. The choice of mode also depends on the material properties, such as particle size, moisture content, and abrasiveness, as well as the layout of the conveying system and the number of destinations.
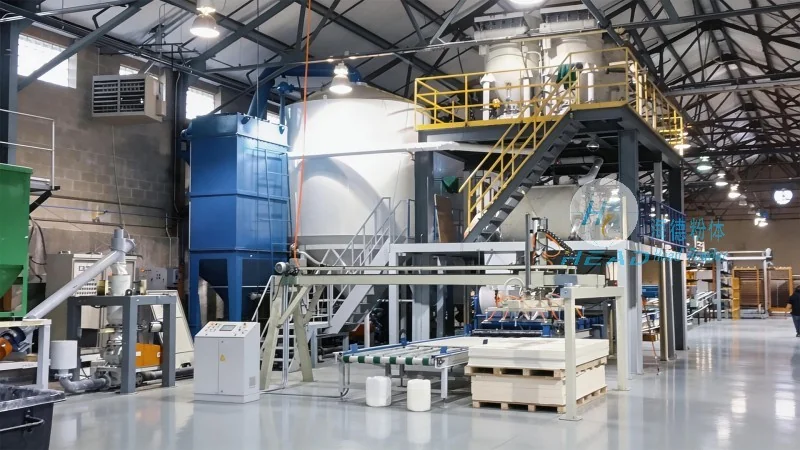
Pneumatic conveying systems offer several technical advantages over traditional mechanical conveying methods. One of the key advantages is the ability to handle bulk materials in a closed system, which reduces dust generation and improves safety. The systems are also highly flexible, allowing for easy integration with other processing equipment and the ability to transport materials to multiple destinations. Another advantage is the low maintenance requirements, as the system components are less prone to wear and tear compared to mechanical conveyors. Additionally, pneumatic conveying systems can be designed to operate in various environmental conditions, including temperature and humidity variations, making them suitable for a wide range of applications.
The compound fertilizer pneumatic conveying systems are widely used in various applications within the fertilizer industry. For example, in fertilizer production plants, these systems are used to transport raw materials from storage silos to processing units, and to move finished products from the production line to storage or packaging areas. In agricultural settings, the systems are used to transport compound fertilizer from storage facilities to application sites, such as farms or greenhouses. The systems are also used in industrial applications, such as in the chemical and food processing industries, where bulk materials need to be transported efficiently and safely.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top