HeadPowder, a leading provider in the field of material handling solutions, specializes in the design, manufacturing, and installation of advanced pneumatic conveying systems. This article provides an overview of the dolomite pneumatic conveying system, detailing its structural components and operational principles to help users understand its functionality and benefits.
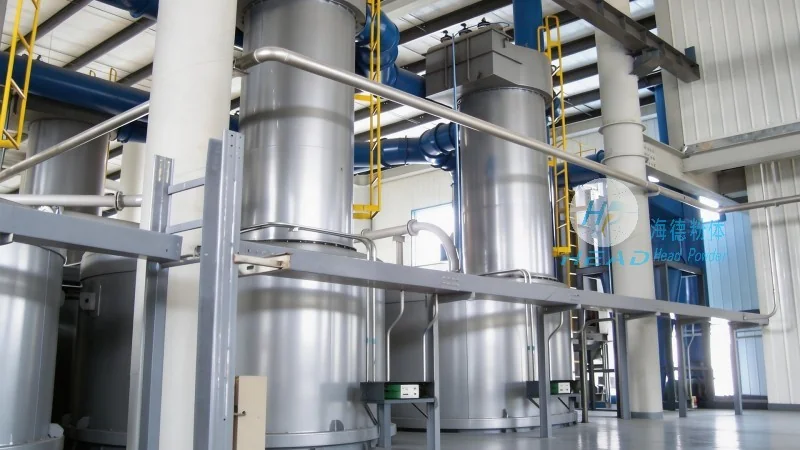
HeadPowder, the brand name for Shandong HeadPowder Engineering Co., Ltd., is headquartered in Shandong, China. With years of experience in the engineering and industrial sectors, the company has established itself as a trusted manufacturer of high-quality pneumatic conveying equipment. The company's commitment to innovation and customer satisfaction has enabled it to serve a wide range of industries, including mining, chemical, and food processing.
Dolomite, a calcium magnesium carbonate mineral, is widely used in various industrial applications such as refractory materials, cement production, and chemical synthesis. The dolomite pneumatic conveying system is specifically designed to handle this material efficiently, ensuring minimal loss and maximum throughput. This system utilizes air as the conveying medium to transport dolomite particles from a source to a destination, eliminating the need for traditional mechanical conveying methods like belt conveyors or bucket elevators.
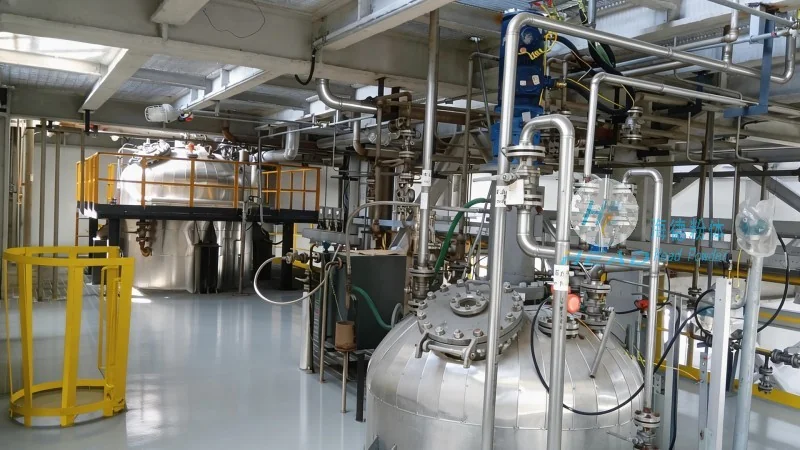
The dolomite pneumatic conveying system consists of several key components that work in tandem to achieve effective material transport. These components include the hopper, which serves as the storage and feeding unit; the air compressor, which generates the necessary air pressure for conveying; the pipeline system, which transports the material and air; the control valve, which regulates the flow of air and material; and the receiver, which collects the conveyed dolomite at the destination. Each component is carefully designed to ensure optimal performance and durability, especially when handling abrasive materials like dolomite.
The operation of the dolomite pneumatic conveying system follows a systematic process. Initially, the dolomite is fed into the hopper from a storage silo or a bulk container. The control valve then opens, allowing air from the compressor to enter the pipeline. As the air flows through the pipeline, it creates a negative pressure or positive pressure environment, depending on the system configuration (e.g., suction or pressure system). The dolomite particles are then entrained by the air stream and transported through the pipeline to the receiver. The receiver is typically equipped with a filter and a dust collection system to prevent dust emissions and maintain air quality. The entire process is controlled by a programmable logic controller (PLC) or a manual control system, ensuring precise regulation of the conveying rate and air pressure.
Compared to traditional conveying methods, the dolomite pneumatic conveying system offers several advantages. Firstly, it eliminates the need for moving parts, reducing maintenance costs and downtime. Secondly, it provides a dust-free and clean conveying environment, which is crucial for industries where dust control is a regulatory requirement. Thirdly, the system can handle a wide range of material sizes and moisture content, making it versatile for different applications. Additionally, the system is compact and can be installed in confined spaces, saving valuable floor space in industrial facilities.
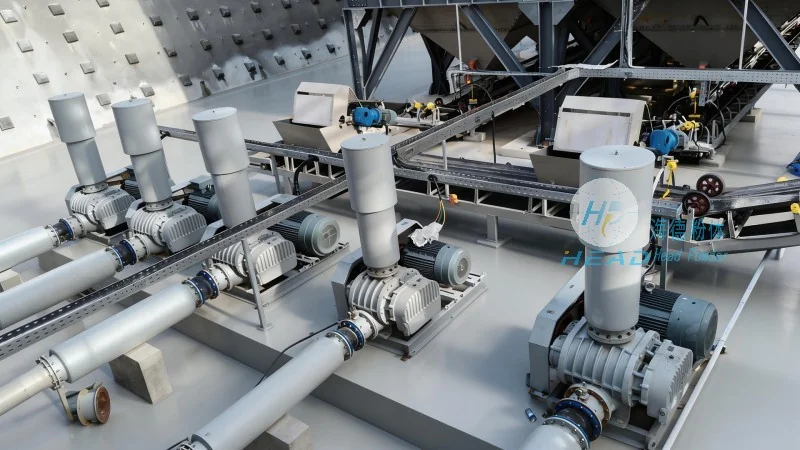
The dolomite pneumatic conveying system is widely used in various industries due to its adaptability and efficiency. In the mining industry, it is used to transport dolomite from ore processing plants to storage facilities. In the chemical industry, it is employed in the production of refractory materials and cement, where dolomite is a key raw material. The food processing industry also utilizes this system for handling dolomite-based additives in food products. Overall, the system's ability to handle abrasive and moisture-sensitive materials makes it a preferred choice in many industrial applications.
In conclusion, the dolomite pneumatic conveying system is a sophisticated and efficient solution for transporting dolomite in various industrial settings. With its robust structural design and advanced operational principles, the system offers numerous benefits, including reduced maintenance, improved dust control, and increased throughput. HeadPowder, as a leading manufacturer, continues to innovate and provide high-quality pneumatic conveying systems that meet the evolving needs of the industry. By understanding the structural components and working principles of this system, users can make informed decisions about its application and maximize its benefits in their operations.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top