The tonne bag quantitative feeding pneumatic conveying system is a specialized industrial equipment designed for efficient and precise material handling. It is widely used in various industries such as chemical, food, pharmaceutical, and bulk material processing. The system is engineered to handle large quantities of bulk materials from tonne bags, ensuring accurate and controlled feeding into downstream processes. This equipment integrates advanced pneumatic conveying technology with precise measurement mechanisms, making it an essential component for modern material handling operations.
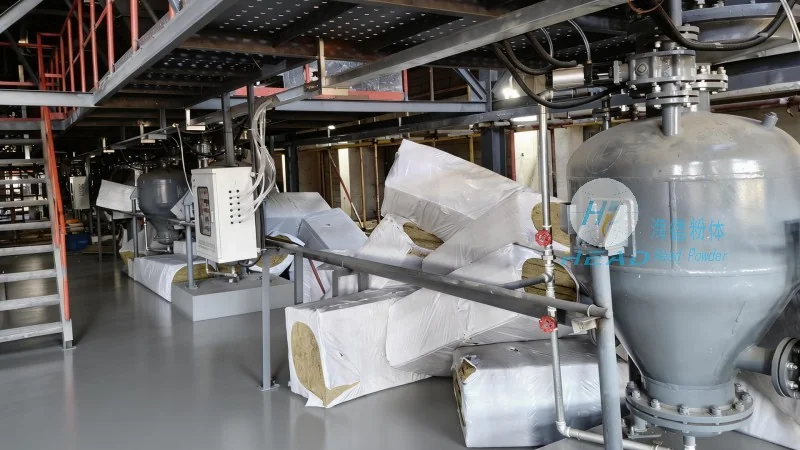
The tonne bag quantitative feeding pneumatic conveying system consists of several critical components that work in tandem to achieve optimal performance. These components include the tonne bag opening mechanism, the material feeding hopper, the pneumatic conveying pipeline, the rotary valve or feeder, the air compressor system, and the control panel. Each component plays a vital role in the overall operation, contributing to the system's reliability and efficiency.
HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design, development, and production of advanced material handling equipment. With years of industry experience, the company has established itself as a trusted provider of high-quality pneumatic conveying systems. The company's commitment to innovation and customer satisfaction has enabled it to deliver solutions that meet the diverse needs of global clients. HeadPowder's products are known for their durability, precision, and energy efficiency, making them ideal for demanding industrial applications.
The core of the tonne bag quantitative feeding pneumatic conveying system is the pneumatic conveying process, which utilizes compressed air to transport bulk materials. The system operates by first opening the tonne bag and allowing the material to fall into the feeding hopper. The material is then drawn into the conveying pipeline by the air flow generated by the air compressor. The rotary valve or feeder regulates the flow of material into the pipeline, ensuring a consistent and controlled feed rate. The compressed air, along with the material, travels through the pipeline to the discharge point, where the material is released into the next processing stage. The control panel monitors and adjusts the system parameters, such as air pressure and material flow rate, to maintain optimal performance.
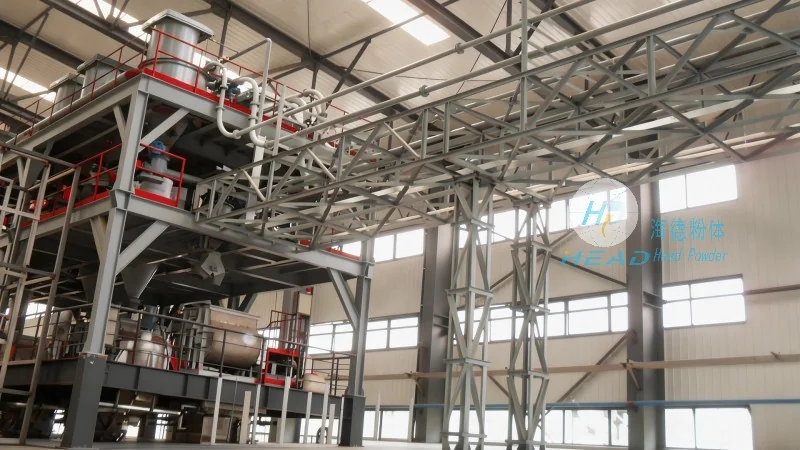
The operation of the tonne bag quantitative feeding pneumatic conveying system involves several sequential steps. First, the tonne bag is positioned under the opening mechanism, which cuts and opens the bag to release the material. The material then falls into the feeding hopper, where it is stored temporarily. Next, the air compressor starts, generating compressed air that creates a vacuum or pressure in the conveying pipeline. The rotary valve opens, allowing the material to be drawn into the pipeline and conveyed to the discharge point. The control panel continuously monitors the system, adjusting the air pressure and material feed rate as needed to maintain the desired flow rate. The system operates in a continuous or batch mode, depending on the application requirements. After the material is fully conveyed, the system can be stopped, and the tonne bag can be replaced with a new one. The entire process is automated, reducing the need for manual intervention and ensuring consistent performance.
The tonne bag quantitative feeding pneumatic conveying system offers several advantages over traditional material handling methods. One of the key benefits is its ability to handle large quantities of bulk materials efficiently and safely. The system minimizes material loss and contamination, as the material is transported in a closed pipeline, preventing exposure to dust and other environmental factors. Additionally, the system provides precise and accurate material feeding, which is crucial for processes that require exact dosing. The automated operation reduces labor costs and improves productivity, making it a cost-effective solution for industrial applications. The system also offers flexibility, as it can be easily integrated with other processing equipment and adapted to different material types and flow rates.
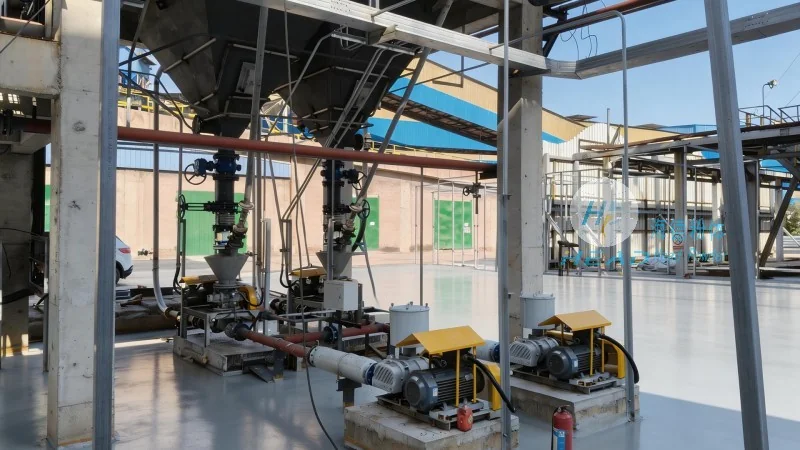
The tonne bag quantitative feeding pneumatic conveying system is suitable for a wide range of applications across various industries. In the chemical industry, it is used to handle powders and granules, such as chemicals, fertilizers, and pigments. In the food industry, it is employed to transport ingredients like flour, sugar, and spices, ensuring food safety and quality. The pharmaceutical industry utilizes the system for handling active pharmaceutical ingredients (APIs) and other sensitive materials, maintaining strict hygiene and contamination control. Other industries, including mining, agriculture, and construction, also benefit from the system's ability to handle bulk materials efficiently. The system's versatility and adaptability make it a valuable asset for any operation that requires reliable and precise material handling.
Proper maintenance and safety measures are essential to ensure the long-term performance and reliability of the tonne bag quantitative feeding pneumatic conveying system. Regular maintenance includes checking the air compressor for proper operation, inspecting the conveying pipeline for blockages or leaks, and cleaning the feeding hopper and rotary valve. The system should be inspected for wear and tear on components, such as seals and bearings, and replaced as needed. Safety considerations include ensuring proper ventilation to prevent the accumulation of dust and fumes, using appropriate personal protective equipment (PPE) when operating the system, and following all safety guidelines provided by the manufacturer. By adhering to these maintenance and safety practices, the system can operate efficiently and safely, minimizing downtime and ensuring the well-being of operators.
The tonne bag quantitative feeding pneumatic conveying system is a sophisticated and efficient solution for bulk material handling. With its precise measurement capabilities and advanced pneumatic conveying technology, the system provides reliable and consistent performance in various industrial applications. HeadPowder, as a leading manufacturer based in Shandong, China, offers high-quality systems that meet the diverse needs of global clients. By understanding the operation process and working principle of this equipment, users can maximize its benefits and ensure optimal performance in their material handling operations.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top