Mobile pneumatic conveying systems represent a sophisticated technology for transporting bulk materials over short to medium distances. These systems are particularly valuable in industrial settings where efficiency, flexibility, and reliability are paramount. The equipment, often referred to as mobile pneumatic conveyors, is designed to handle a wide range of materials, including powders, granules, and even fine particles, with minimal maintenance and operational complexity.
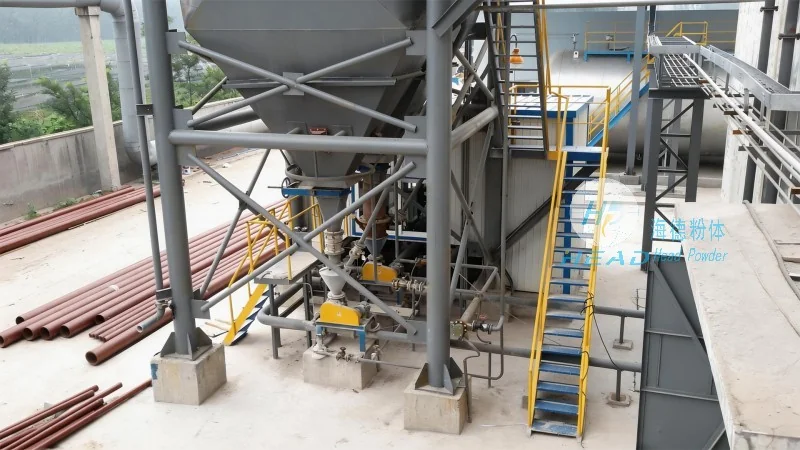
At the core of mobile pneumatic conveying systems is the ability to transport materials using compressed air or other gases. Unlike traditional mechanical conveyors, which rely on physical components like belts or buckets, pneumatic systems utilize air pressure to move materials through a pipeline network. This approach offers several advantages, such as reduced material degradation, lower installation costs, and the capacity to handle materials that are difficult to transport with mechanical means.
The operation of mobile pneumatic conveying systems typically involves several key steps. First, the material is fed into the system from a hopper or storage silo. A blower or compressor then generates the necessary air pressure to create a flow of air through the pipeline. The material is then entrained by the air stream and carried to the destination point, such as a processing unit or storage tank. The system may include components like cyclones, filters, and separators to ensure that the material is efficiently separated from the air before discharge. The entire process is controlled by a programmable logic controller (PLC) or other automation systems, which regulate the air flow, material feed rate, and system pressure to maintain optimal performance.
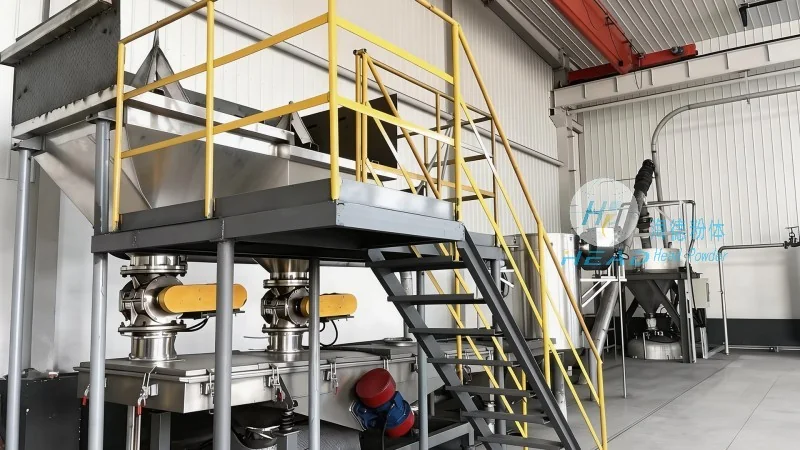
The working principle of mobile pneumatic conveying systems is based on the principle of fluidization and pneumatic transport. When compressed air is introduced into the pipeline, it creates a low-density environment that allows the material particles to become suspended in the air stream. This suspension allows the material to be transported with minimal friction and energy loss. The system’s design, including the size and shape of the pipeline, the velocity of the air, and the particle size distribution of the material, all play critical roles in determining the efficiency and effectiveness of the conveying process. Additionally, the system may incorporate features like vacuum or pressure modes, depending on the specific application requirements, to enhance its versatility.
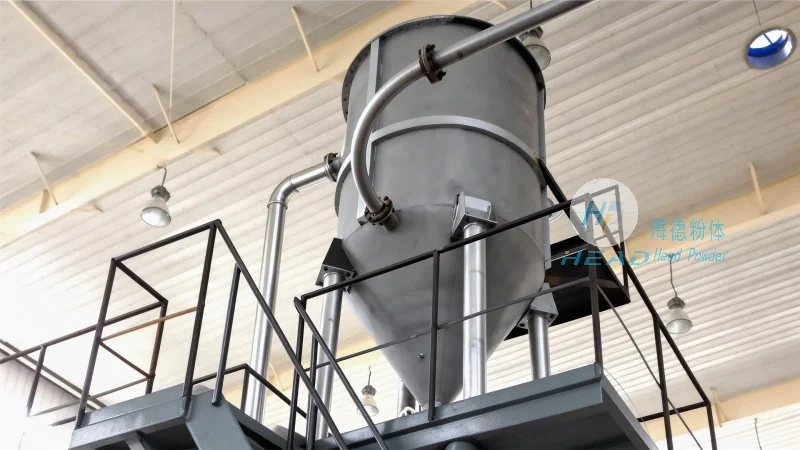
Mobile pneumatic conveying systems consist of several essential components that work in tandem to ensure smooth operation. The primary components include a material feed hopper, a blower or compressor, a pipeline network, and a discharge unit. The material feed hopper is responsible for storing and feeding the bulk material into the system. The blower or compressor provides the necessary air pressure to generate the conveying air. The pipeline network transports the material and air from the feed point to the discharge point. The discharge unit, which may include cyclones or filters, separates the material from the air and directs the material to its final destination. Other components, such as check valves, flow meters, and pressure sensors, are also integrated to monitor and control the system’s performance, ensuring that it operates within safe and efficient parameters.
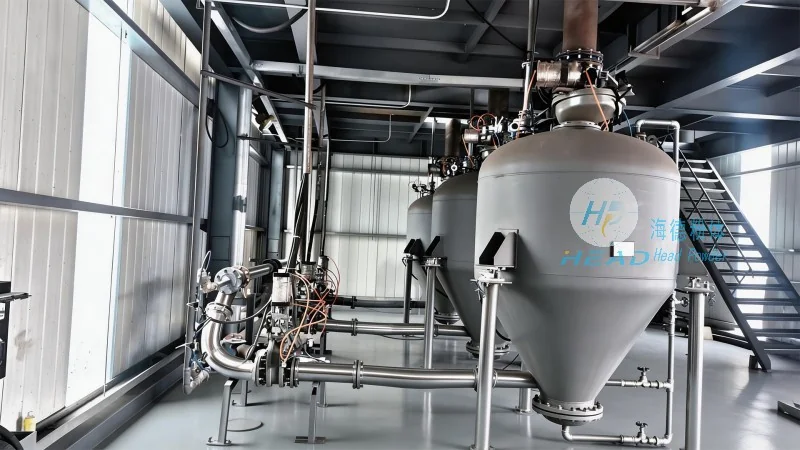
The adoption of mobile pneumatic conveying systems offers numerous benefits across various industries. These systems are particularly well-suited for applications where material handling requires flexibility and mobility, such as in construction sites, mining operations, and agricultural processing. The equipment’s ability to handle a wide range of materials, including sensitive or abrasive substances, reduces the risk of material degradation and equipment wear. Additionally, the systems are compact and can be easily reconfigured to adapt to changing operational needs, making them ideal for temporary or mobile applications. The low maintenance requirements and energy efficiency of these systems also contribute to their growing popularity in industrial settings.
As a leading manufacturer of mobile pneumatic conveying systems, Shandong HeadPowder Engineering Co., Ltd. specializes in providing high-quality equipment tailored to the specific needs of industrial clients. With a focus on innovation and customer satisfaction, the company has established itself as a trusted partner in the material handling industry. HeadPowder’s products are designed to meet the most demanding operational requirements, ensuring reliability and efficiency in diverse applications. The company’s headquarters is located in Shandong, China, where it operates a state-of-the-art manufacturing facility and research and development center. HeadPowder’s commitment to quality and customer service has earned it a reputation for excellence in the industry, making it a preferred choice for businesses seeking reliable and efficient material handling solutions.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top