Bulk bin pneumatic conveying systems are advanced industrial equipment designed to transport bulk materials from storage bins to processing or packaging units. These systems are widely used in various industries such as food, chemical, pharmaceutical, and mining, where efficient and dust-free material handling is crucial. The equipment, manufactured by Shandong HeadPowder Engineering Co., Ltd., integrates innovative technology to ensure reliable performance and minimal maintenance.
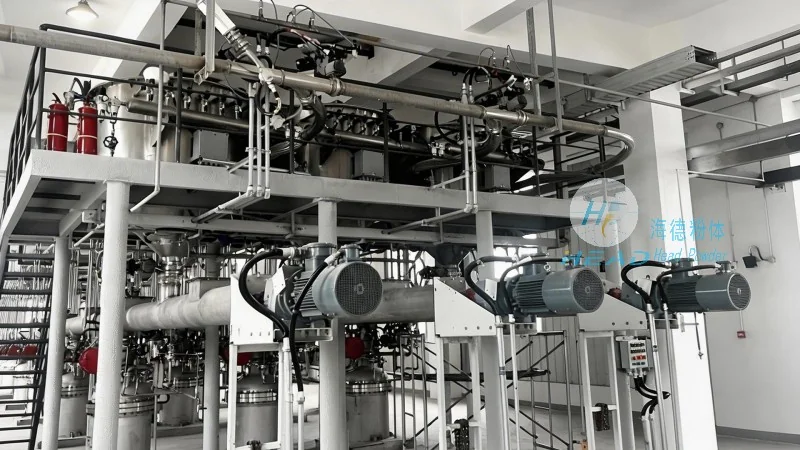
The core working principle of a bulk bin pneumatic conveying system involves the use of compressed air to move bulk materials through a pipeline network. The system typically consists of a hopper or bulk bin, a feeder, a conveying line, and a receiver. When the system is activated, compressed air is introduced into the hopper, creating a pressure differential that lifts the material and propels it through the pipeline. The material is then transported to the destination, where it is discharged into a processing or storage container. This process is highly efficient and can handle a wide range of materials, including powders, granules, and small particles.
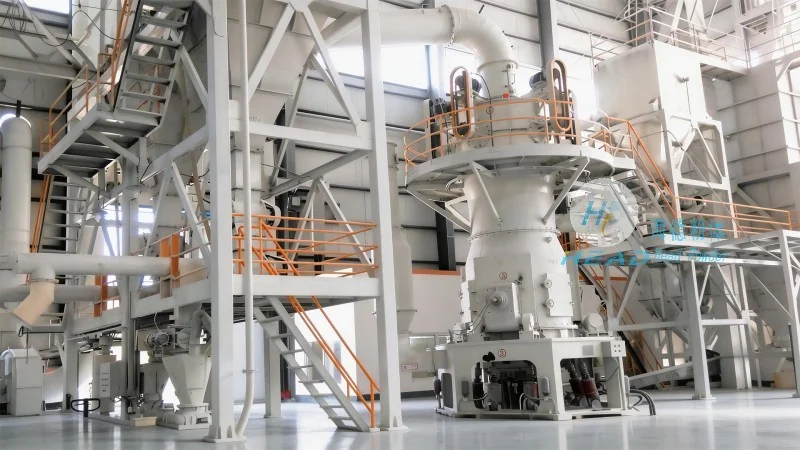
The operation process of a bulk bin pneumatic conveying system is straightforward and automated. Initially, the bulk bin is filled with the material to be conveyed. The system then starts by activating the feeder, which controls the flow rate of the material into the conveying line. Compressed air is supplied to the hopper, creating a vacuum or pressure that moves the material. The material travels through the pipeline, which may include bends, elbows, and filters to ensure smooth and efficient transport. At the receiving end, the material is discharged into a container or processing unit. The system is equipped with sensors and controls to monitor pressure, flow rate, and material level, ensuring optimal operation and preventing blockages or overflows.
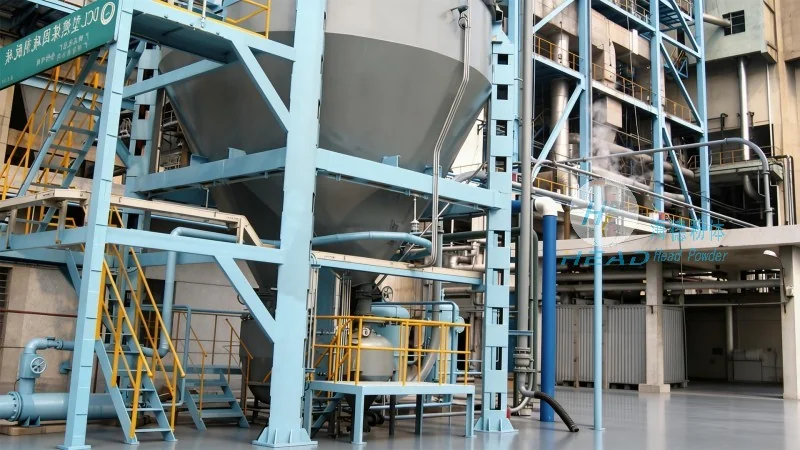
Several key components work together to ensure the smooth operation of a bulk bin pneumatic conveying system. The bulk bin or hopper serves as the storage container, holding the bulk material. The feeder, often a rotary valve or screw feeder, regulates the material flow into the conveying line. The conveying line, typically made of stainless steel or plastic, transports the material under pressure. The receiver or discharge unit collects the material at the end of the pipeline. Additionally, the system includes a compressor or air supply unit that provides the necessary compressed air, and a filter system to remove dust and debris from the air, ensuring clean and efficient operation.
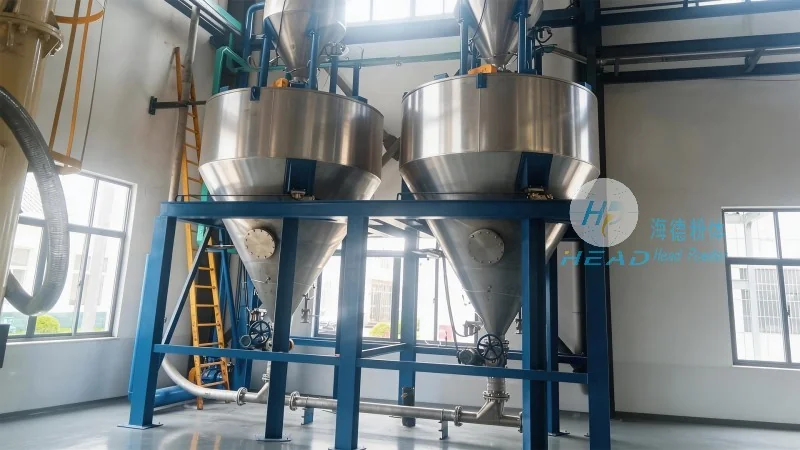
Bulk bin pneumatic conveying systems are versatile and can be applied in various industrial settings. They are commonly used in food processing plants for transporting flour, sugar, and other powders, where hygiene and dust control are essential. In the chemical industry, these systems handle powders and granules, ensuring safe and efficient material transfer. The pharmaceutical industry also benefits from these systems, as they provide a clean and controlled environment for handling sensitive materials. The primary benefits of using a bulk bin pneumatic conveying system include reduced labor costs, improved safety (as there is no manual handling of materials), increased efficiency (faster material transfer), and lower maintenance costs due to the absence of mechanical parts in the conveying line.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top