HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced air-driven pneumatic conveyors tailored for handling wet ammonium nitrate powders. These systems are engineered to efficiently transport bulk materials in industrial settings, ensuring safety, reliability, and optimal performance under challenging conditions. The following sections will delve into the fundamental principles behind these conveyors and explore the key working scene characteristics that make them indispensable in modern material handling operations.
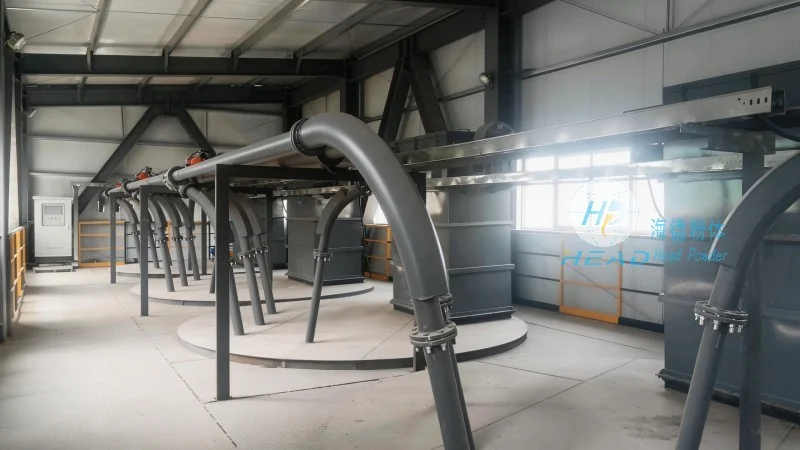
The core mechanism of air-driven pneumatic conveyors involves the use of compressed air to create a flow of material through a pipeline. In the case of wet ammonium nitrate powders, the system typically operates under positive pressure, where air is introduced at the inlet to generate a high-velocity air stream that entrains the powder particles. This process, known as pneumatic conveying, relies on the interaction between the air flow and the material particles to achieve efficient transport. The system consists of several critical components, including a hopper for material storage, a rotary airlock valve to control the feed rate, a pipeline system for material transport, and a receiver for material discharge. The compressed air is supplied by a blower or compressor, which maintains the necessary pressure to ensure consistent material flow. The design of the conveyor is optimized to minimize pressure drop and energy consumption while maximizing material throughput, making it suitable for various industrial applications.
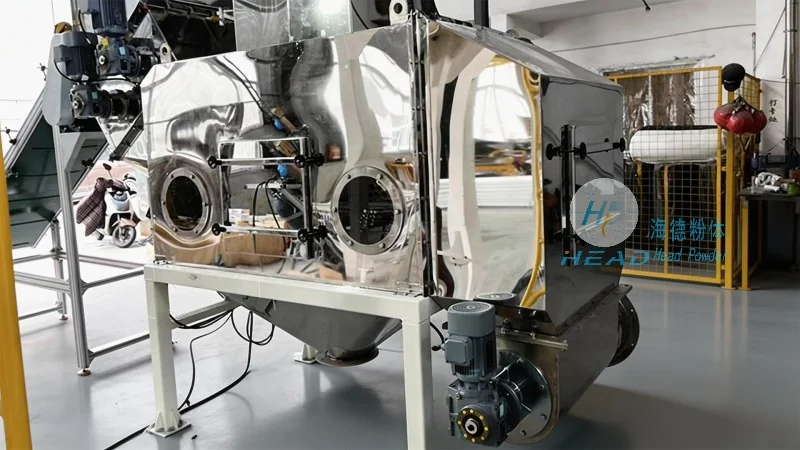
The working scene characteristics of air-driven pneumatic conveyors for wet ammonium nitrate powders are shaped by several key factors, including material properties, operational requirements, and environmental considerations. Wet ammonium nitrate is a hygroscopic material that can absorb moisture from the air, which may affect its flowability and handling characteristics. Therefore, the conveyor system must be designed to maintain consistent moisture levels and prevent caking or agglomeration of the powder. The system is also engineered to handle varying particle sizes and densities, ensuring that the conveying process remains stable and efficient. In industrial settings, these conveyors are commonly used in fertilizer production, chemical processing, and agricultural applications, where the need to transport bulk materials over long distances or through complex layouts is critical. The working scene may involve multiple stages of material processing, such as mixing, drying, and packaging, and the conveyor must integrate seamlessly with these processes to maintain a smooth workflow. Additionally, the system is designed to comply with safety regulations, particularly in environments where explosive or hazardous materials are handled, ensuring that the conveying process is safe and reliable.
HeadPowder's air-driven pneumatic conveyors for wet ammonium nitrate powders are distinguished by several key features that enhance their performance and reliability. The system incorporates advanced control systems that allow for precise regulation of air pressure and material feed rate, ensuring consistent material flow and minimizing downtime. The use of high-quality materials, such as stainless steel and corrosion-resistant components, ensures durability and longevity, even in harsh operating conditions. The conveyor is also designed for easy maintenance and cleaning, with accessible components that can be quickly serviced to maintain optimal performance. Another advantage is the energy efficiency of the system, which reduces operational costs while minimizing environmental impact. The company's expertise in material handling technology, combined with its commitment to innovation, ensures that their conveyors meet the highest standards of quality and performance.
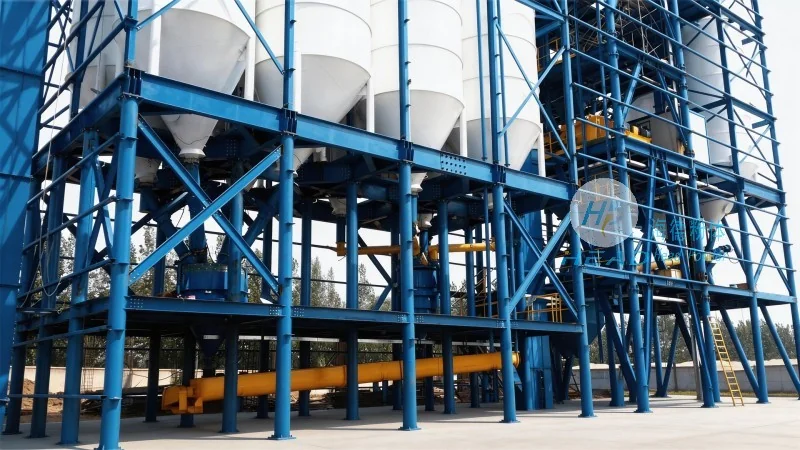
The air-driven pneumatic conveyors from HeadPowder are widely used in various industrial applications, providing significant operational benefits to users. In fertilizer production, for example, these systems enable efficient transport of wet ammonium nitrate from storage to processing units, reducing the risk of material spillage and improving overall productivity. The conveyors are also suitable for chemical processing plants, where the need to handle bulk chemicals safely and efficiently is paramount. The system's ability to handle varying material conditions, such as moisture content and particle size, makes it adaptable to different production requirements. Additionally, the low maintenance requirements and long service life of the conveyor contribute to cost savings and increased operational efficiency. The working scene characteristics of these conveyors, including their ability to operate in complex layouts and maintain consistent performance, make them a preferred choice for industries that require reliable and efficient material handling solutions.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top