HeadPowder, a leading engineering firm based in Shandong, China, specializes in the design and development of advanced material handling solutions. This article focuses on the design of a negative pressure pneumatic conveying device specifically tailored for the transportation of magnesium hydroxide, a critical component in various industrial applications.
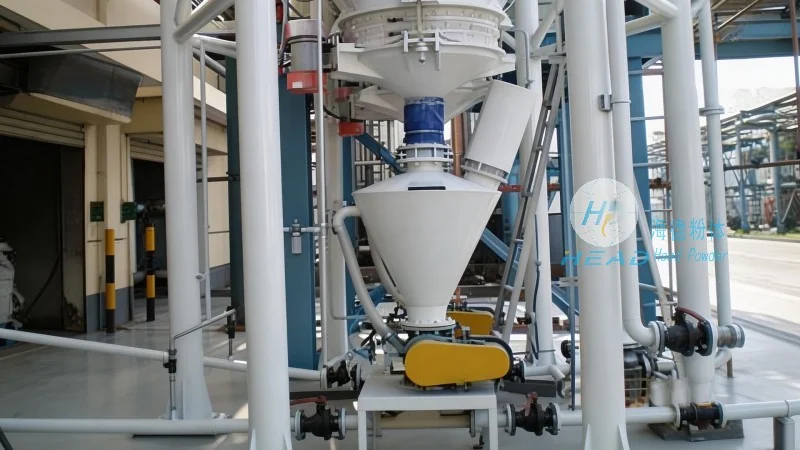
The negative pressure pneumatic conveying system is engineered to efficiently transport magnesium hydroxide from storage silos or processing units to downstream equipment such as reactors, mixers, or packaging systems. By utilizing a vacuum or negative pressure environment, the system draws the material through a network of pipes, ensuring a controlled and dust-free transfer process. This method is particularly advantageous for handling fine powders like magnesium hydroxide, which are prone to caking or agglomeration under normal conditions.
The system incorporates several critical components that work in tandem to ensure optimal performance and reliability. The primary components include a vacuum pump, a feed hopper with a rotary valve, a conveying pipeline system, and a receiver or discharge unit. The vacuum pump generates the necessary negative pressure to initiate material flow, while the feed hopper and rotary valve control the rate of material discharge into the pipeline. The conveying pipeline is designed with appropriate bends and fittings to minimize pressure drop and prevent blockages, which is crucial for maintaining consistent flow rates. The receiver unit is equipped with a dust collection system to capture any fine particles that may escape during the conveying process, ensuring environmental compliance and product purity.
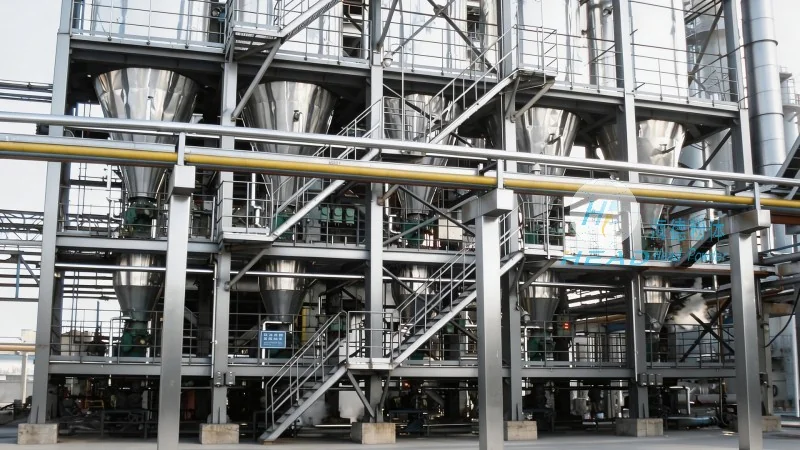
The negative pressure pneumatic conveying device is designed to handle magnesium hydroxide with high efficiency and minimal loss. The system can transport materials over considerable distances, typically ranging from 50 to 200 meters, depending on the specific configuration. The design ensures that the material is conveyed at a controlled velocity, preventing excessive wear on the pipeline and reducing the risk of product degradation. The system also features adjustable parameters such as pressure and flow rate, allowing operators to optimize performance based on the characteristics of the magnesium hydroxide being handled. This adaptability makes the device suitable for various production scales, from small-scale laboratory applications to large industrial manufacturing processes.
Compared to positive pressure or mechanical conveying methods, the negative pressure system offers several distinct advantages. The primary benefit is the reduced risk of dust generation and inhalation hazards, as the material is drawn into the system rather than being expelled. This enhances workplace safety and compliance with environmental regulations. Additionally, the system is more energy-efficient, as it requires less power to maintain the negative pressure compared to generating high positive pressure. The design also minimizes product contamination, as the conveying environment is isolated from external air, preventing the introduction of moisture or contaminants that could affect the quality of magnesium hydroxide. Furthermore, the system is relatively simple to install and maintain, with fewer moving parts compared to other conveying technologies, reducing downtime and operational costs.
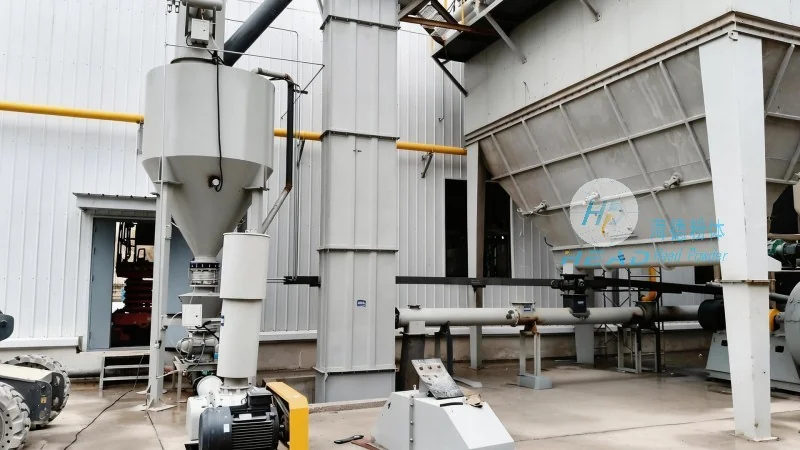
The negative pressure pneumatic conveying device is widely used in industries that rely on magnesium hydroxide as a key raw material. These include the production of fire retardants, pharmaceuticals, and cosmetics, where the purity and consistency of the material are critical. The system ensures that magnesium hydroxide is transferred without any degradation, maintaining its chemical properties and effectiveness in downstream applications. In the fire retardant industry, for example, the consistent delivery of magnesium hydroxide to the mixing and compounding stages is essential for achieving the desired flame retardant properties in final products. Similarly, in pharmaceutical manufacturing, the system helps maintain the sterility and quality of the material, which is crucial for meeting regulatory standards. The reliable and efficient operation of the conveying system contributes to overall production efficiency and cost reduction in these industries.
HeadPowder's design of the negative pressure pneumatic conveying device for magnesium hydroxide represents a significant advancement in material handling technology. By combining advanced engineering principles with practical application requirements, the system offers a reliable and efficient solution for transporting fine powders. The company's commitment to innovation and quality ensures that the device meets the evolving needs of the industry, providing customers with a robust and cost-effective material handling solution. As industrial demands continue to grow, HeadPowder remains at the forefront of developing advanced solutions that enhance productivity and safety in material processing operations.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top