For businesses in the cereal processing industry, efficient and reliable material handling is crucial to maintaining production efficiency and product quality. The design of a cereal pneumatic conveying system is a critical aspect that directly impacts operational performance. This article introduces the key considerations and components involved in designing an effective cereal pneumatic conveying equipment, highlighting the expertise of Shandong HeadPowder Engineering Co., Ltd. as a leading provider in the field.
When designing a cereal pneumatic conveying system, several key factors must be considered to ensure optimal performance and longevity. The first is the type of material being conveyed, as cereals vary in size, density, and moisture content, which affect the selection of conveying method and equipment. For example, small, light particles like wheat or corn may require different pressure or vacuum settings compared to larger, heavier grains like oats or barley. The system design must also account for the material's flow characteristics, such as its angle of repose and cohesive properties, to prevent blockages and ensure smooth transport.
Another critical factor is the system's capacity and throughput requirements. The conveying equipment must be sized to handle the desired production volume, whether it's a small-scale operation or a large industrial facility. This involves calculating the required air volume, pressure, and power to move the material from the source to the destination. Additionally, the system's layout and integration with existing production lines are important considerations, as the design must ensure minimal disruption to current operations while maximizing efficiency.
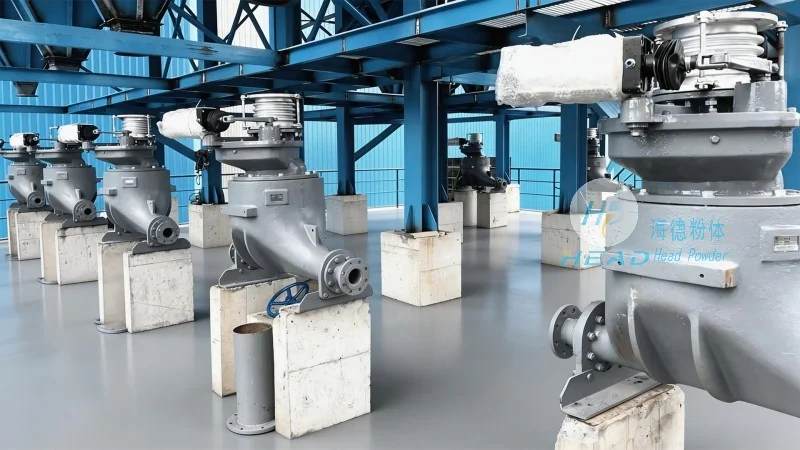
A typical cereal pneumatic conveying system consists of several key components that work together to facilitate material transport. The primary components include a hopper or feed bin to store the cereal, a feeder to control the flow rate, a conveying line (either pressure or vacuum), and a receiver or discharge bin. The hopper is designed to maintain the material's flowability and prevent caking, while the feeder ensures a consistent and controlled discharge of the material into the conveying line. The conveying line, which can be made of metal or plastic, is responsible for transporting the material using air pressure or suction. The receiver is where the material is deposited and collected, often equipped with a dust collection system to maintain air quality and prevent contamination.
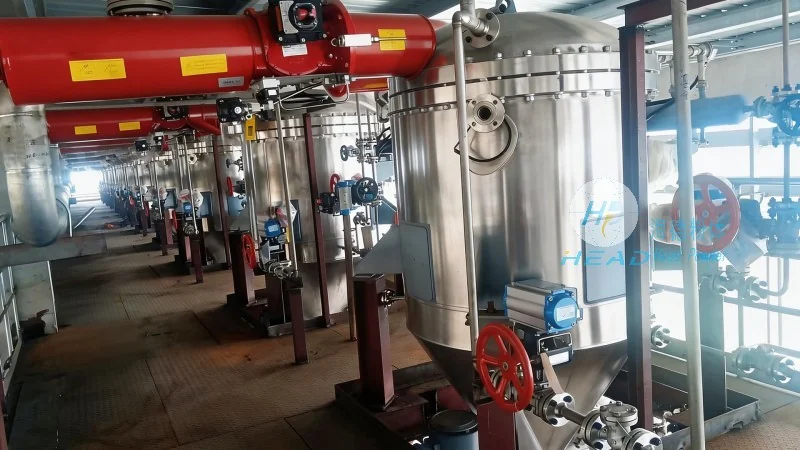
Each component plays a vital role in the overall performance of the system. For instance, the feeder must be capable of handling the specific characteristics of the cereal, such as its moisture content or particle size, to avoid overloading or underloading the conveying line. The conveying line's design, including its diameter and length, affects the air velocity and pressure required to move the material efficiently. The receiver's design, including its shape and size, influences the material's discharge and the prevention of material buildup or blockages.
Efficiency and durability are paramount when designing a cereal pneumatic conveying system. The system must be designed to minimize energy consumption while maximizing material throughput. This involves optimizing the air pressure and flow rate to achieve the desired conveying speed without excessive energy use. Additionally, the materials used in the construction of the equipment must be durable and resistant to corrosion or wear from the cereal particles. For example, stainless steel is often used for components that come into direct contact with the material to prevent contamination and ensure longevity.
Another important consideration is the system's ability to handle variations in material characteristics. Cereal products can vary in quality and composition, and the conveying system must be flexible enough to accommodate these changes without requiring significant modifications. This includes the ability to adjust the feeder settings, air pressure, or conveying line parameters to maintain optimal performance under different conditions. The system's design should also include features for easy maintenance and cleaning, as cereals can be sticky or prone to caking, which can affect the equipment's performance over time.
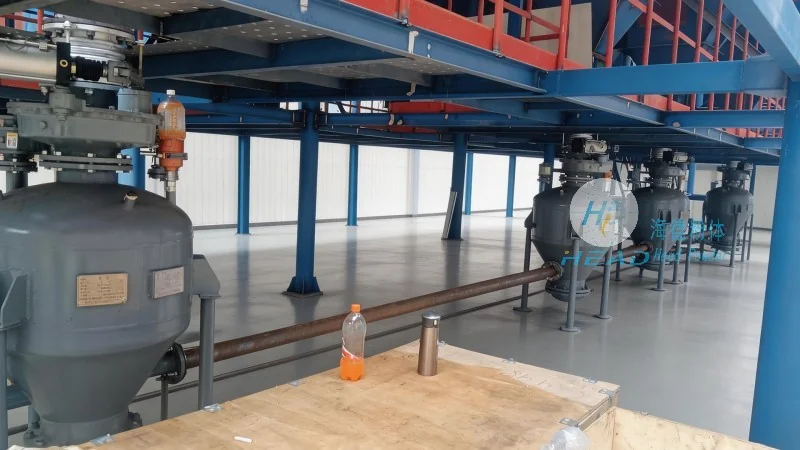
Shandong HeadPowder Engineering Co., Ltd. specializes in the design and manufacturing of cereal pneumatic conveying equipment, leveraging years of experience in the industry. The company's team of engineers and technicians works closely with clients to understand their specific needs and develop customized solutions that meet their operational requirements. HeadPowder's approach to design emphasizes efficiency, durability, and reliability, ensuring that the final product is tailored to the client's unique production environment and material characteristics.
The company's expertise extends to the integration of advanced technologies in the design process. This includes the use of computational fluid dynamics (CFD) to simulate the material flow and optimize the system's performance, as well as the incorporation of sensors and monitoring systems to track the system's operation and detect any issues in real-time. These technologies help to ensure that the final design is not only efficient but also easy to maintain and operate, reducing downtime and maintenance costs for the client.
HeadPowder's commitment to quality and customer satisfaction is evident in its product range and service. The company provides comprehensive support, from initial consultation and system design to installation and after-sales service. This ensures that clients receive a complete solution that meets their needs and exceeds their expectations. By partnering with HeadPowder, businesses can benefit from a reliable and efficient cereal pneumatic conveying system that enhances their production capabilities and contributes to their overall success.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top