When designing a pneumatic conveying system for phosphate powder, several critical factors must be considered to ensure efficiency, reliability, and cost-effectiveness. The system's performance is directly influenced by the properties of the phosphate material, such as its particle size, moisture content, and flow characteristics. Understanding these factors is essential for selecting the appropriate conveying technology and components.
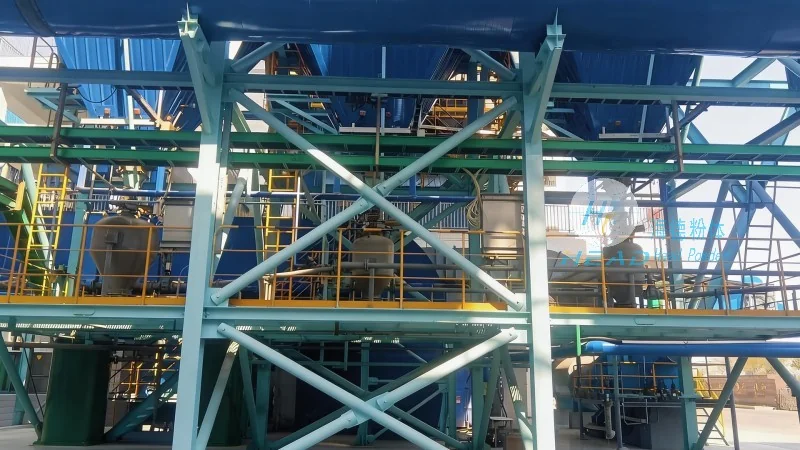
One of the primary considerations is the particle size distribution of the phosphate powder. Coarse particles may cause blockages in the conveying line, while fine particles can lead to excessive pressure drop and increased energy consumption. Therefore, it is crucial to analyze the material's particle size and adjust the system's design accordingly, such as selecting the right nozzle size and air velocity. The moisture content of the phosphate powder also plays a significant role. High moisture levels can cause clumping, which may obstruct the system and reduce conveying efficiency. Proper drying or moisture control measures should be integrated into the design to maintain optimal material flow.
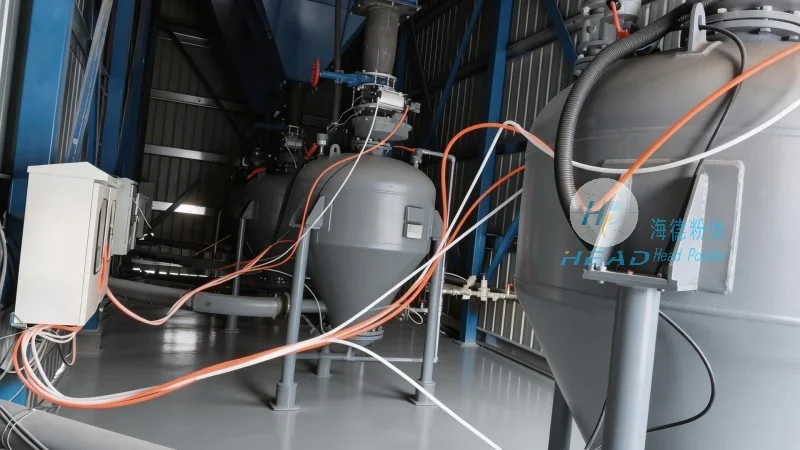
The selection of system components, including the blower, filter, and conveying line, directly impacts the overall performance of the phosphate powder pneumatic conveying system. The blower must be capable of generating sufficient air pressure and volume to transport the phosphate powder over the required distance. Different types of blowers, such as rotary lobe or centrifugal, may be suitable depending on the system's requirements. The filter is another critical component, as it prevents the phosphate powder from escaping into the environment and protects downstream equipment from contamination. The choice of filter material and design should be based on the powder's particle size and dust characteristics to ensure effective filtration and minimal pressure loss.
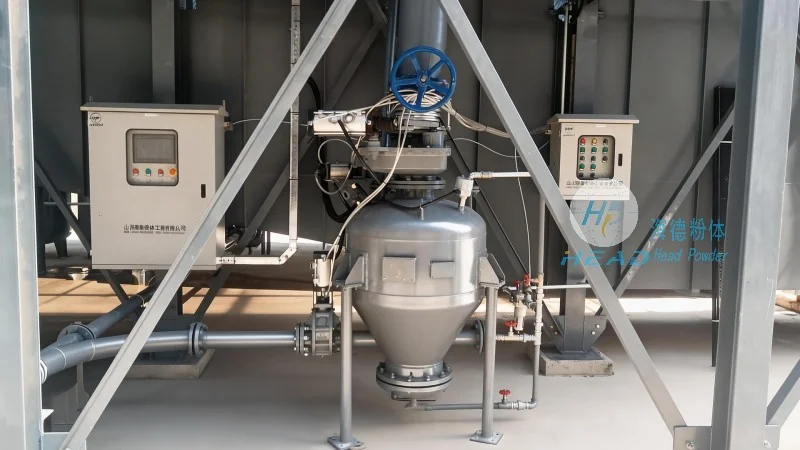
Proper material handling is essential to prevent material degradation and ensure worker safety. The conveying system should be designed to minimize material impact and abrasion, which can affect the quality of the phosphate powder. Additionally, safety measures, such as explosion-proof designs for the blower and proper ventilation, must be incorporated to comply with industrial safety regulations. The system should also include monitoring and control features to detect any abnormalities, such as pressure drops or blockages, and alert operators promptly.
Energy efficiency is a key factor in the long-term operation of a phosphate powder pneumatic conveying system. By optimizing the air velocity and pressure, the system can reduce energy consumption while maintaining the required conveying capacity. Regular maintenance and inspection of system components, such as the blower and filter, are necessary to prevent energy waste and extend the system's lifespan. Additionally, the use of efficient materials and components can contribute to cost savings over the system's operational life.
Shandong HeadPowder Engineering Co., Ltd., a leading provider of pneumatic conveying solutions, specializes in designing and manufacturing systems tailored to the unique needs of phosphate powder handling. With years of experience in the industry, the company has developed a deep understanding of the challenges associated with transporting phosphate materials and offers customized solutions to meet specific operational requirements. HeadPowder's expertise ensures that clients receive reliable, efficient, and cost-effective pneumatic conveying systems that enhance their production processes and improve overall operational performance.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top