Compound fertilizer powder conveying equipment is a specialized system designed to handle and transport bulk powder materials, particularly in the agricultural and chemical industries. These systems are crucial for efficient material handling, ensuring that fertilizer powders are moved from storage to processing or packaging areas with minimal loss and maximum efficiency. The technology behind these devices combines mechanical engineering principles with material science to address the unique challenges of handling fine, abrasive, and often hygroscopic powders like those used in compound fertilizers.
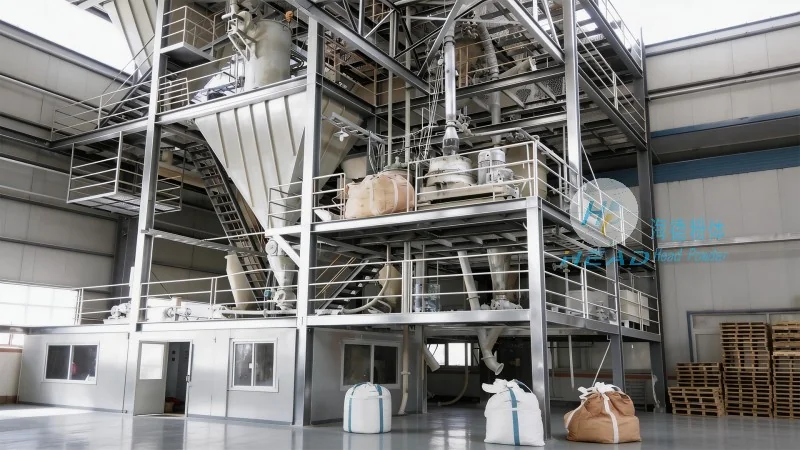
The core of compound fertilizer powder conveying equipment lies in its ability to transport bulk materials through a closed system, typically using positive pressure or negative pressure to move the powder. One common method is the use of screw conveyors or augers, which rotate to push the powder forward. Another approach involves pneumatic conveying systems, where compressed air or other gases are used to create a flow of the powder through pipes. These systems often incorporate components such as feed hoppers, rotary valves, and dust collection units to ensure smooth operation and prevent material degradation. The design of the equipment must account for the properties of the fertilizer powder, including its particle size, density, and flowability, to optimize performance and minimize wear on components.
Several critical components work together to ensure the effective operation of compound fertilizer powder conveying equipment. The feed hopper is the initial point where the powder is loaded, often equipped with a level indicator to monitor the material volume. The rotary valve, or feeder, regulates the flow rate of the powder into the conveying line, preventing overloading and ensuring a consistent feed. The conveyor itself—whether a screw, pneumatic, or belt conveyor—transports the material through the system. For pneumatic systems, the air compressor and filter system are essential to maintain air quality and pressure. Additionally, dust collection and filtration systems are integrated to control airborne particles, which is vital for maintaining a safe and clean working environment. The control panel, equipped with sensors and automation features, allows operators to monitor and adjust the system parameters in real-time, enhancing efficiency and reducing downtime.
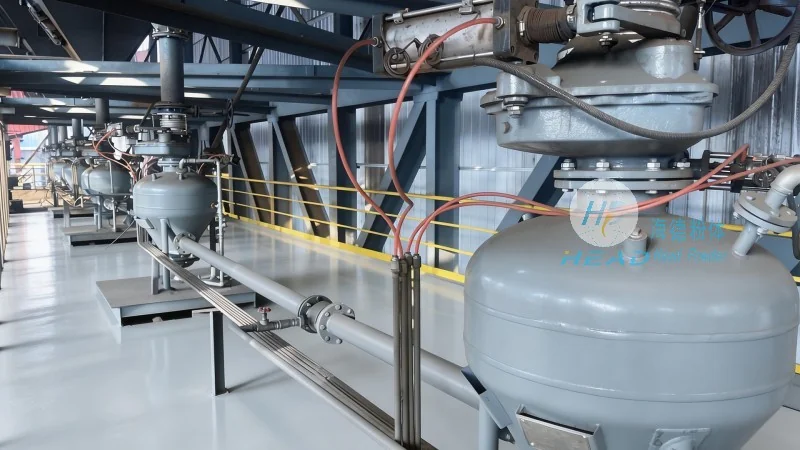
Compound fertilizer powder conveying equipment is widely used in various industrial settings, each with distinct characteristics that influence the equipment's design and operation. In fertilizer production plants, these systems are integrated into the manufacturing process, moving raw materials from storage silos to mixing and granulation units. The working environment in such plants is often characterized by high humidity and temperature, requiring equipment that is corrosion-resistant and capable of handling abrasive materials. In agricultural supply centers or distribution facilities, the equipment is used to transport bulk fertilizer to storage tanks or loading areas for delivery to farms. Here, the focus is on durability and ease of maintenance, as the equipment may be used in outdoor or semi-outdoor conditions. Additionally, in research and development laboratories, specialized conveying systems are used to handle small batches of experimental fertilizers, where precision and minimal material loss are paramount. Each working scene demands tailored solutions, from the type of conveyor (e.g., screw vs. pneumatic) to the material of construction, to ensure optimal performance and safety.
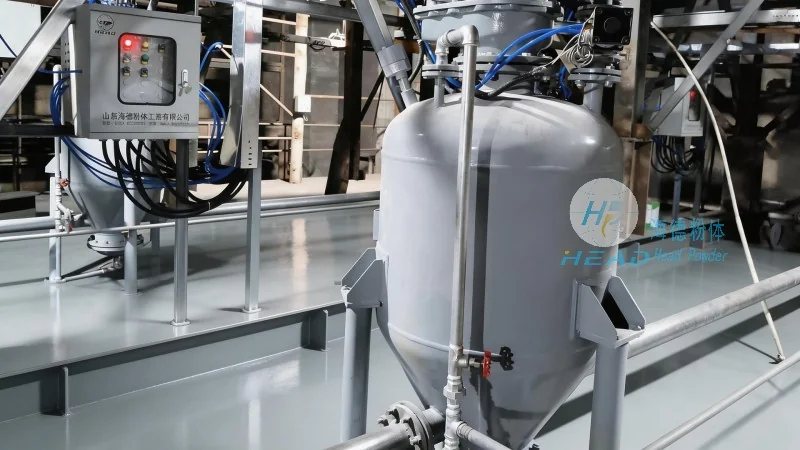
Implementing compound fertilizer powder conveying equipment offers numerous advantages for businesses in the agricultural and chemical sectors. One of the primary benefits is improved efficiency, as these systems can transport large volumes of powder at high speeds, reducing the time and labor required for material handling. This leads to increased production throughput and lower operational costs. Another key advantage is the reduction of material loss and contamination. By using a closed system, the equipment minimizes the exposure of the fertilizer to the environment, preventing caking, moisture absorption, and cross-contamination with other materials. This not only preserves the quality of the fertilizer but also reduces waste and associated costs. Furthermore, the automation and control features of modern conveying systems enhance safety by reducing the need for manual handling of bulk materials, which can be hazardous due to dust inhalation or physical injury risks. The equipment also contributes to better workplace hygiene, as the enclosed design and dust collection systems keep the working area clean and free from airborne particles. Overall, the use of compound fertilizer powder conveying equipment enhances operational reliability, product quality, and worker safety, making it a critical investment for any facility handling bulk fertilizer powders.
Compound fertilizer powder conveying equipment is a vital component in the efficient and safe handling of bulk fertilizer materials. By understanding the working principles, key components, and working scene characteristics, businesses can select and implement the most suitable system for their needs. The technology continues to evolve, with advancements in automation, material handling, and environmental control, ensuring that these systems remain effective and adaptable to changing industry demands. As a leading provider in this field, Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing high-quality conveying equipment tailored to the unique requirements of fertilizer production and distribution. With a focus on durability, efficiency, and safety, the company's solutions help clients optimize their operations and maintain the quality of their products. Based in Shandong, China, HeadPowder Engineering Co., Ltd. leverages years of experience and technical expertise to deliver reliable and innovative solutions for the agricultural and chemical industries.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top