High-pressure dilute phase powder conveying systems represent advanced industrial solutions for the efficient and reliable transport of bulk powder materials. These systems are integral to operations across diverse sectors, including chemical, pharmaceutical, food processing, and mining, where the safe and effective movement of powders is paramount to operational success. Developed by Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer based in Shandong, China, such systems exemplify cutting-edge technology in powder handling. This article provides a comprehensive overview of the operation process and working principles of high-pressure dilute phase powder conveying systems, detailing key components, operational workflow, and the engineering principles that enable efficient powder transport.
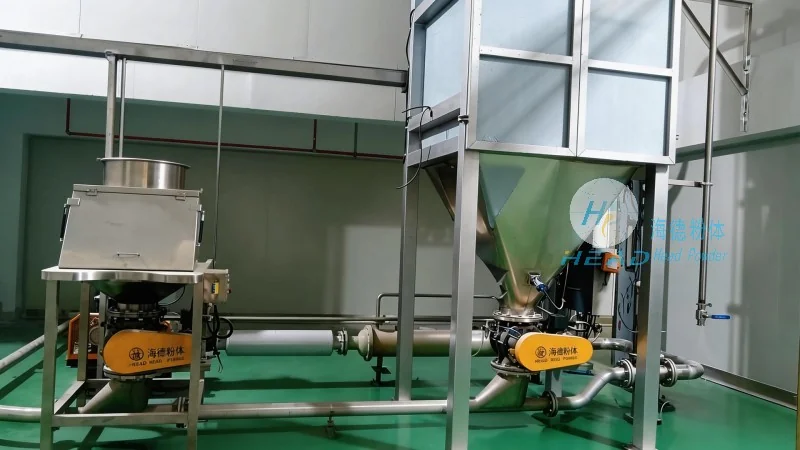
The high-pressure dilute phase powder conveying system comprises several critical components that collaborate to ensure smooth and efficient operation. These components include the material feeder, which introduces the powder into the system; the high-pressure blower or compressor, which generates the necessary airflow to transport the powder; the pipeline system, which carries the powder-air mixture; and the control system, which regulates flow and pressure. Additional features may include cyclone separators for material separation, dust collection systems for environmental compliance, and safety valves to prevent overpressure. Each component plays a vital role in maintaining system performance and ensuring the safe handling of powders.
The operation process begins with the powder material being fed into the system via the material feeder, which ensures a consistent and controlled flow. Once the powder enters, it is mixed with high-pressure air generated by the blower or compressor. The air pressure is carefully regulated to achieve the optimal dilute phase condition, where powder particles are suspended in the air stream rather than settling due to gravity. The powder-air mixture then travels through the pipeline system, which may include bends, expansions, or other fittings, all designed to maintain flow without excessive pressure loss or particle separation. At the receiving end, cyclone separators or other separation devices separate the powder from the air, allowing the powder to be deposited in the desired location while the air is either recirculated or discharged through a dust collection system. The control system continuously monitors parameters such as pressure, flow rate, and temperature, adjusting operation as needed to maintain optimal performance and prevent failures.
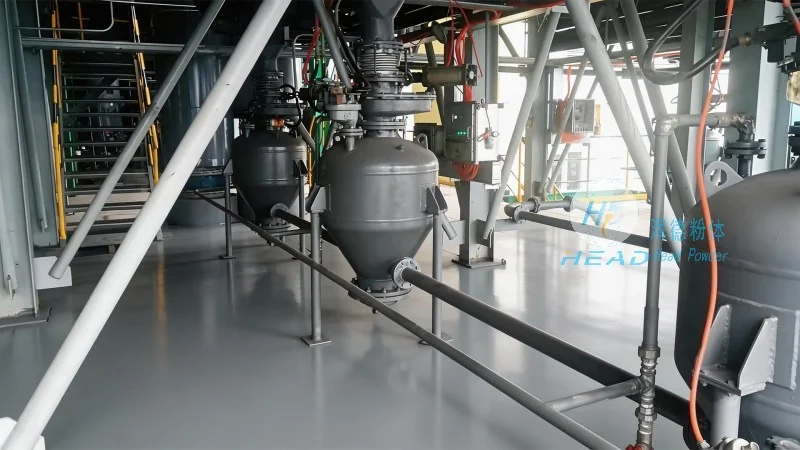
The working principle is rooted in fluid dynamics and particle mechanics. The system operates by creating a high-velocity air stream that suspends powder particles in a dilute phase, enabling transport through the pipeline. The key is maintaining the correct air-to-powder ratio to keep particles suspended without settling or clogging. The high pressure from the blower or compressor provides the kinetic energy to overcome gravitational forces and maintain flow. Pipeline design, including diameter, length, and fittings, is critical to minimize pressure losses and stay within operational parameters. Features like air recirculation or dust collection enhance efficiency and reduce environmental impact. The control system uses real-time feedback from sensors to adjust air pressure, flow rate, and other parameters, ensuring system stability.
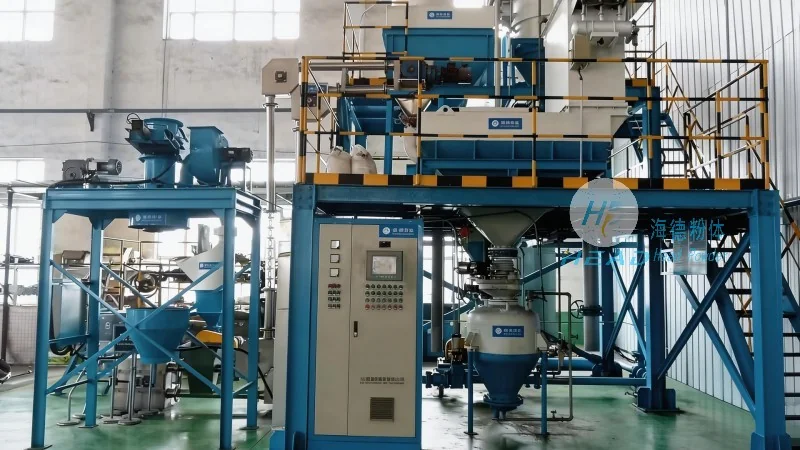
High-pressure dilute phase systems offer several advantages over traditional methods like pneumatic or mechanical conveying. They can transport powders over long distances with minimal pressure loss, making them suitable for applications requiring material movement between locations. The system provides flexibility to accommodate different powder types and flow rates. Compared to mechanical systems, they have fewer moving parts, reducing maintenance needs and increasing reliability. High-pressure air allows transport of difficult-to-handle powders like fine or cohesive materials, which may be challenging with other methods. Integration with other processing equipment (e.g., mixers, reactors) creates continuous production lines, improving efficiency and reducing downtime.
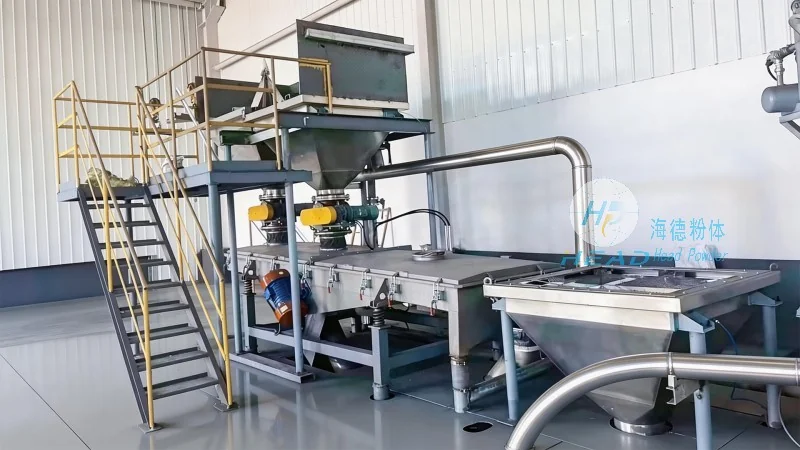
These systems are used across multiple industrial applications where bulk powder transport is essential. In the chemical industry, they transport raw materials and finished products, such as powders for pharmaceuticals or specialty chemicals. In the pharmaceutical sector, they handle active pharmaceutical ingredients (APIs) and other powders, ensuring sterile and controlled handling. The food processing industry uses them for ingredients like flour, sugar, or spices, maintaining product quality and purity. In mining, they transport ore or mineral powders from mines to processing facilities. The cement industry utilizes them for transporting raw materials like limestone or clay. Their versatility makes them valuable in modern industrial operations.
Maintaining system performance and safety is crucial for long-term operation. Regular maintenance involves cleaning pipelines and components to prevent powder residue buildup, which can cause clogging or reduced efficiency. The high-pressure blower or compressor should be inspected regularly to ensure it operates within design parameters, with wear and tear addressed promptly to avoid failures. The control system must be checked to confirm proper function and that all sensors and monitoring devices work correctly. Safety is paramount: the system should include safety valves to prevent overpressure and be installed in well-ventilated areas to avoid dust accumulation. Personnel must be trained in safety procedures and wear appropriate PPE to minimize injury risk. By following proper maintenance and safety protocols, high-pressure dilute phase powder conveying systems can provide reliable and efficient operation for extended periods.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top