Understanding the operation process and working principle of sand and gravel powder conveying systems is crucial for optimizing material handling efficiency in construction and mining industries. These systems are designed to transport bulk materials like sand, gravel, and other fine powders over long distances with minimal loss and maximum reliability. The following sections detail the key components, operational steps, and underlying principles that enable the smooth functioning of such equipment, provided by Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer of industrial conveying solutions based in China.
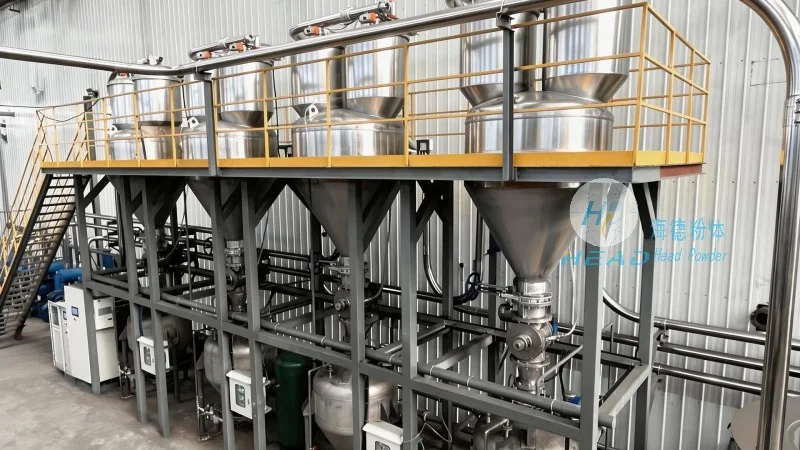
The sand and gravel powder conveying system typically consists of several critical components that work in tandem to ensure effective material transport. These include the hopper for material storage, a conveyor mechanism (such as a screw conveyor or pneumatic pipeline), control valves, and a dust collection system. Each component plays a vital role in maintaining the integrity of the material and preventing contamination or degradation during transit. The hopper is designed to hold a large volume of raw materials, ensuring a steady supply to the conveyor. The conveyor itself may vary in type depending on the material characteristics and distance requirements. For example, a screw conveyor is ideal for handling dry, free-flowing powders, while a pneumatic system is suitable for fine, dusty materials that require air pressure to move. Control valves are integrated to regulate the flow rate, preventing overloading or underflow. The dust collection system is essential for maintaining a clean and safe working environment by capturing and filtering airborne particles.
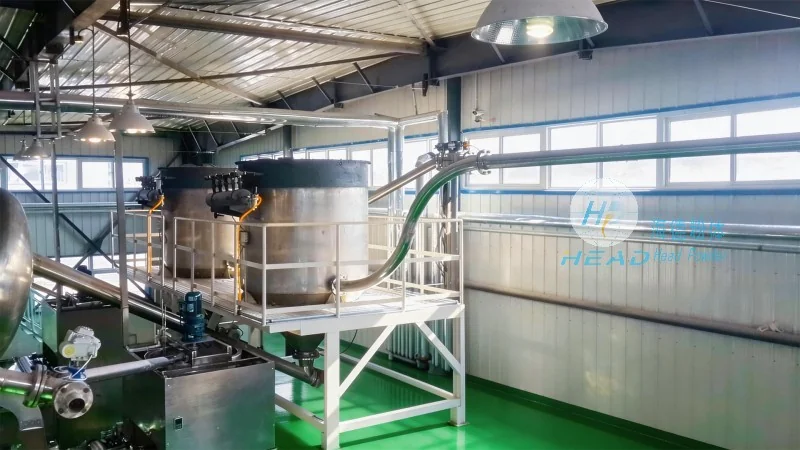
The operation of a sand and gravel powder conveying system follows a systematic sequence of steps to ensure consistent and efficient material transport. The process begins with the loading of raw materials into the hopper. Once the hopper is filled, the conveyor mechanism is activated, either by motor-driven rotation or air pressure in the case of pneumatic systems. The material is then moved through the conveyor pipeline to the discharge point. At this stage, control valves may be adjusted to regulate the flow rate, ensuring that the receiving container or processing unit is filled at an optimal pace. The system continuously monitors the material level in the hopper and conveyor, providing real-time feedback to operators for adjustments if needed. This closed-loop control helps maintain a stable flow and prevents interruptions in the production line. The entire operation is designed to be automated to a large extent, reducing the need for manual intervention and minimizing human error. Regular maintenance checks are performed to ensure all components are functioning correctly, extending the lifespan of the equipment and maintaining its performance.
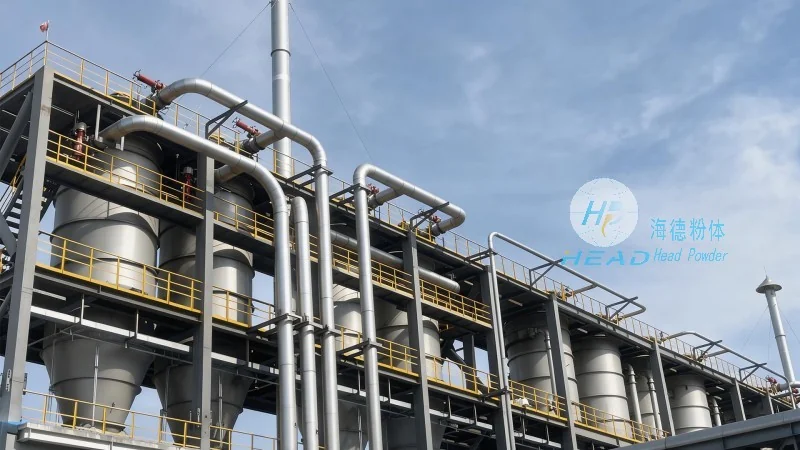
The working principle of the sand and gravel powder conveying system is based on the physics of material movement and the mechanics of the chosen conveyor type. For screw conveyors, the principle involves the rotation of a helical screw within a tube, which pushes the material forward due to friction and the design of the screw threads. The pitch and diameter of the screw are carefully selected to match the material's flow characteristics, ensuring smooth and continuous transport. The speed of the screw rotation determines the flow rate, allowing for precise control over the amount of material conveyed per unit time. In pneumatic conveying systems, the principle relies on the use of compressed air to create a flow of material through a pipeline. The material is suspended in the air stream and transported to the destination. The pressure and velocity of the air are critical factors, as they must be sufficient to overcome the material's weight and friction within the pipeline. The system may use positive or negative pressure, depending on the application, with positive pressure being more common for transporting materials over longer distances or to higher elevations. The air flow is controlled by valves and regulators to maintain a consistent pressure and flow rate, ensuring reliable material transport.
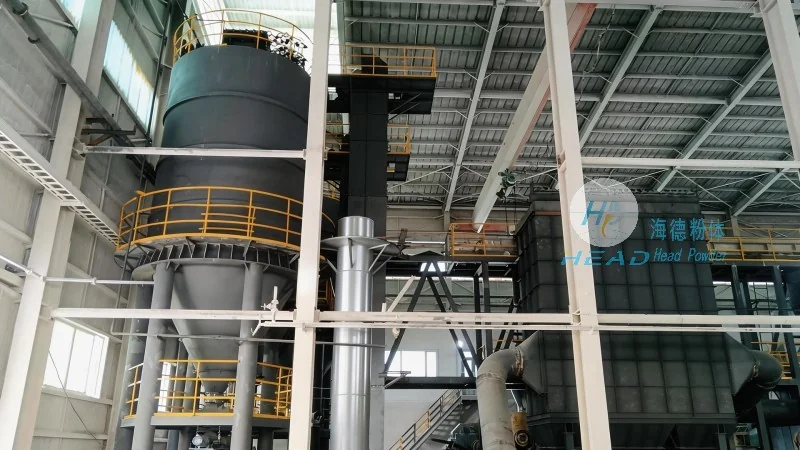
The sand and gravel powder conveying system offers numerous benefits that make it an essential component in various industrial applications. One of the primary advantages is its ability to transport large volumes of material over long distances with minimal energy consumption compared to traditional methods like trucking. This reduces transportation costs and environmental impact by minimizing the number of vehicles on the road. The system also provides a continuous and consistent flow of material, which is crucial for maintaining production efficiency in manufacturing and construction processes. Additionally, the enclosed design of the system prevents dust and contamination, ensuring that the material remains clean and free from external pollutants. This is particularly important for materials used in food processing, pharmaceuticals, or other industries where purity is paramount. The system's flexibility allows it to be adapted to different material types and processing requirements, making it suitable for a wide range of applications, from small-scale construction projects to large-scale mining operations.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top