Shandong HeadPowder Engineering Co., Ltd., a leading enterprise in the field of powder handling technology, specializes in the design, manufacturing, and supply of advanced stone coal powder conveying systems. The company, operating from Shandong, China, has established itself as a key player by delivering reliable and efficient solutions tailored to the needs of various industrial sectors. This article provides an in-depth look at the operation process and working principle of such systems, highlighting the technical aspects and practical applications that make them indispensable in modern material handling operations.
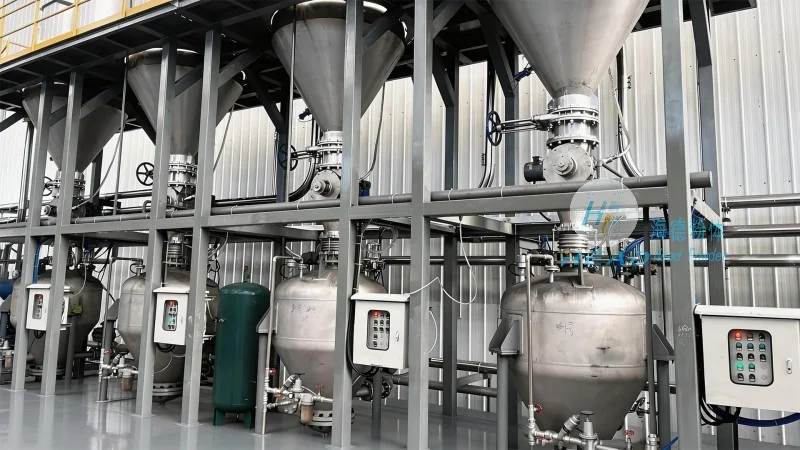
The stone coal powder conveying system typically consists of several core components that work in concert to ensure seamless material transport. These components include a hopper for material storage, a conveyor mechanism (such as screw or pneumatic conveyors), a control system for operation management, and a discharge outlet for the final delivery of the material. The system is engineered to handle a wide range of particle sizes and densities, making it suitable for diverse applications in industries like mining, power generation, and chemical processing. Each component is designed with durability and efficiency in mind, ensuring long-term performance and minimal maintenance requirements.
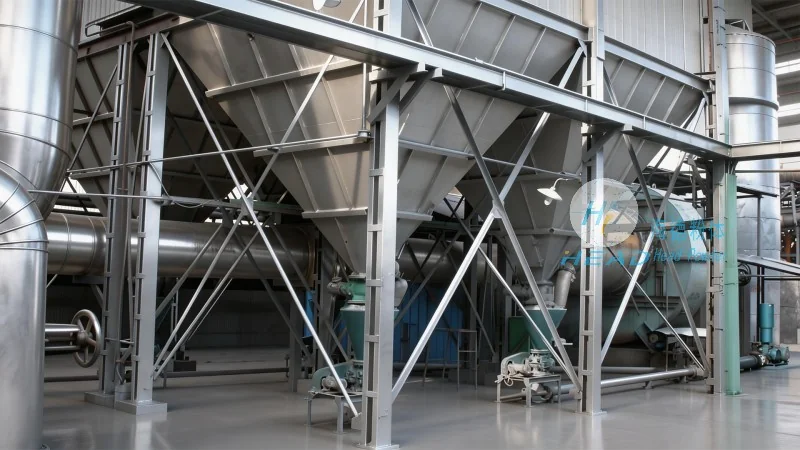
The operation of the stone coal powder conveying system is based on the principles of mechanical or pneumatic transport, depending on the specific design. In mechanical systems, a rotating screw or belt transports the material from the hopper to the discharge point, utilizing gravity and mechanical force to move the powder. The control system regulates the speed and direction of the conveyor, allowing for precise control over the material flow rate. In pneumatic systems, compressed air is used to create a flow of air and material through a pipeline, enabling the transport of fine powders over longer distances with less risk of clogging. The working principle emphasizes the integration of these components to achieve consistent and reliable material transfer, minimizing downtime and maximizing productivity.
The operation process of the stone coal powder conveying system begins with the loading of the material into the hopper. The material is fed into the system through a feeding mechanism, which may include a feeder or a hopper with a controlled opening. Once the material is in the hopper, the control system activates the conveyor, initiating the transport process. The conveyor then moves the material through the system, either by mechanical means or pneumatic pressure, until it reaches the discharge outlet. At this point, the material is released and directed to its final destination, such as a storage silo or a processing unit. The entire process is monitored by the control system, which adjusts parameters as needed to maintain optimal performance. This systematic approach ensures that the conveying operation is efficient, safe, and consistent, meeting the demands of industrial applications.
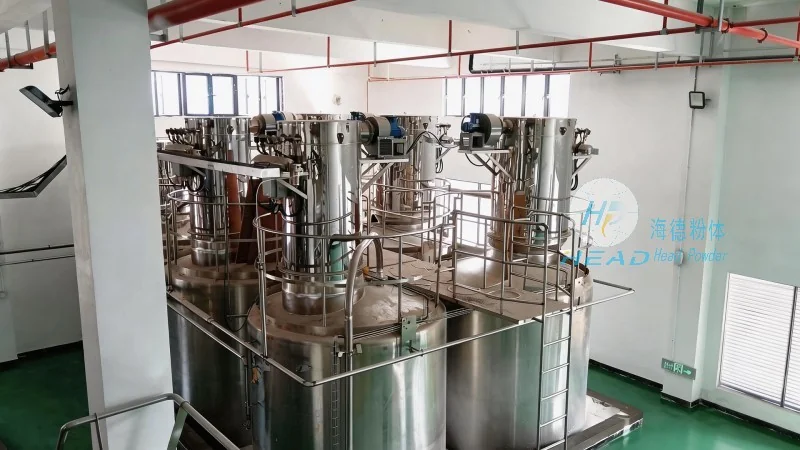
The stone coal powder conveying system offers several advantages that make it a preferred choice for industries dealing with fine powders. These include high efficiency in material transport, minimal product degradation due to gentle handling, and the ability to handle materials with varying properties. The system is particularly suitable for applications where dust control and contamination prevention are critical, such as in food processing or pharmaceutical industries. Additionally, the modular design of the system allows for easy customization and expansion, enabling it to adapt to changing production needs. The applications of this system span across various sectors, including coal handling in power plants, mineral processing in mining operations, and material transport in chemical manufacturing, demonstrating its versatility and reliability.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top