Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer based in Shandong, China, specializes in the design and production of advanced tonne bag powder handling equipment. This article explores the fundamental principles behind these systems and highlights their key working characteristics across various industrial applications.
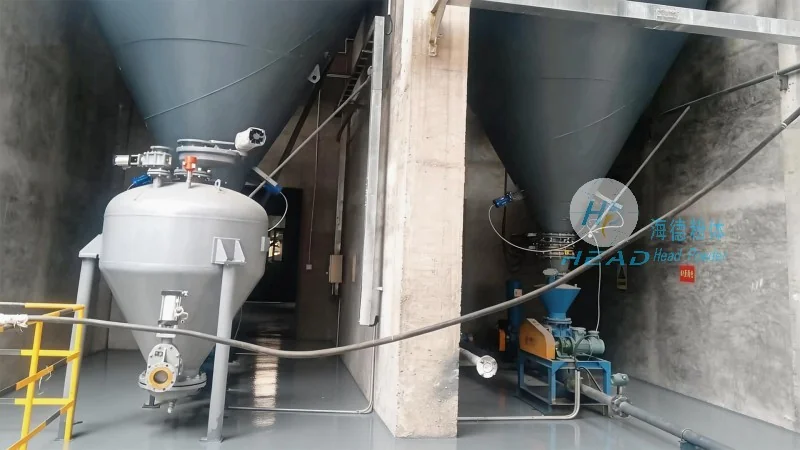
The primary function of tonne bag powder handling equipment is to efficiently transfer bulk powders from storage containers, such as tonne bags, into processing or storage systems. The core principle revolves around creating a controlled flow of material, often utilizing vacuum or pressure differential mechanisms to move the powder. These systems typically include components like vacuum pumps, air filters, and conveying lines that work in tandem to ensure smooth and consistent material transport. The design prioritizes safety, efficiency, and minimal product contamination, which are critical factors in industries where powders are sensitive or hazardous.
One of the most notable characteristics of tonne bag powder handling equipment is its ability to handle large volumes of material with minimal labor. The system automates the process of opening, emptying, and sealing tonne bags, reducing the risk of dust exposure and improving workplace safety. Additionally, the equipment is designed for versatility, accommodating a wide range of powder types, including fine powders, granules, and even sticky or cohesive materials. This adaptability makes it suitable for applications in pharmaceuticals, food processing, chemical manufacturing, and other sectors where material integrity is paramount.
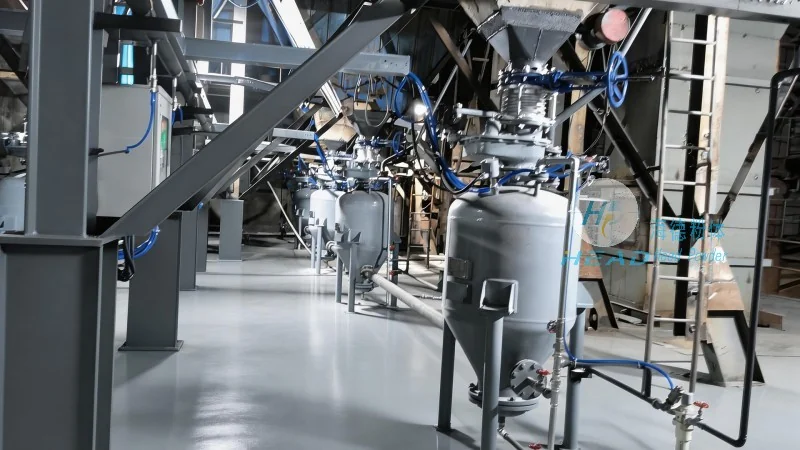
In industrial settings, tonne bag powder handling equipment is employed in several key scenarios. For instance, in pharmaceutical plants, it is used to transfer raw materials into mixing and compounding lines, ensuring precise dosing and maintaining sterile conditions. In food processing facilities, the equipment handles ingredients like flour, sugar, and spices, supporting production lines that require consistent quality and hygiene. Chemical manufacturers utilize these systems to transport bulk chemicals, which may be hazardous, by controlling the flow and minimizing exposure risks. The equipment's design also allows for integration with existing production lines, enabling seamless material transfer without disrupting workflow.
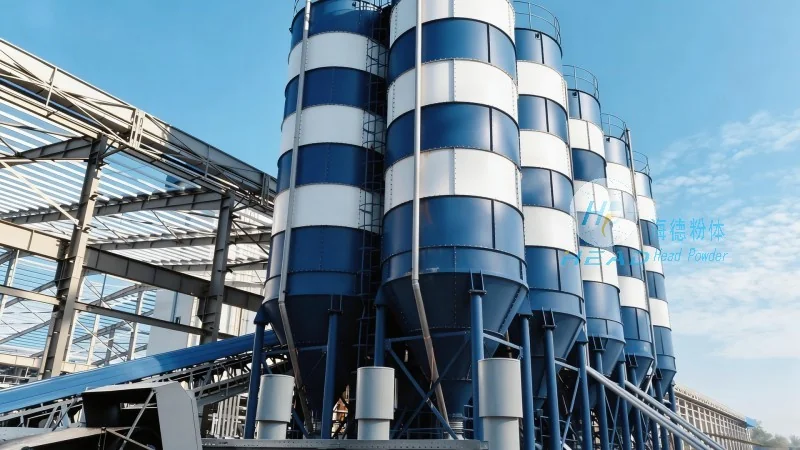
By leveraging advanced engineering and material handling technologies, tonne bag powder handling equipment significantly enhances operational efficiency. The automated process reduces downtime associated with manual handling, leading to increased productivity and lower labor costs. Moreover, the equipment's safety features, such as dust extraction systems and sealed conveying lines, help mitigate health risks and comply with regulatory standards. This combination of efficiency and safety makes it an essential asset for businesses operating in industries where powder handling is a core part of their production process.
Shandong HeadPowder Engineering Co., Ltd. continues to innovate in the field of powder handling technology, providing solutions that meet the evolving needs of modern industries. The principles and characteristics of tonne bag powder handling equipment, as outlined above, underscore its importance in ensuring reliable, safe, and efficient material transfer. For businesses seeking to optimize their powder handling processes, investing in such equipment from a reputable manufacturer like HeadPowder can lead to significant improvements in productivity, safety, and overall operational performance.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top