HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced powder handling solutions. Our flagship product, the automatic bulk bag unloading powder handling equipment, is engineered to streamline the process of transferring bulk materials from sealed bags into processing systems. This equipment integrates multiple functions, including bulk bag opening, material discharge, and optional conveying, to enhance operational efficiency and safety in various industrial applications.
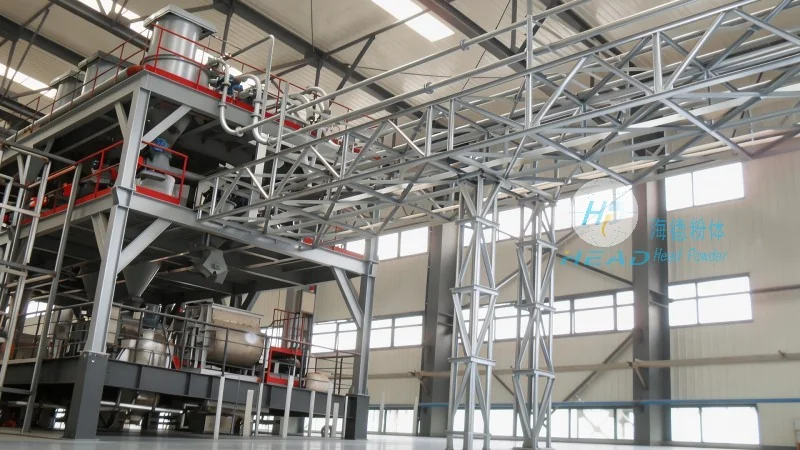
The automatic bulk bag unloading system from HeadPowder is engineered to handle a wide range of powders, including chemicals, food ingredients, and pharmaceuticals. Key features include: automated bag opening via cutting or tearing mechanisms, integrated dust collection to minimize environmental impact, and adjustable discharge rates to match downstream processing requirements. The system is constructed with high-quality materials, ensuring durability and resistance to corrosion from aggressive substances. Additionally, it incorporates safety sensors and emergency stop buttons to protect operators and prevent equipment damage during operation.
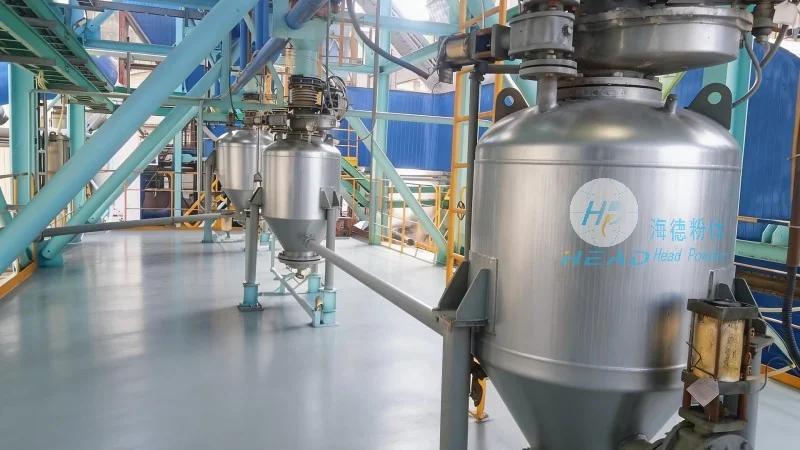
The operation of the automatic bulk bag unloading powder handling equipment follows a systematic sequence. Initially, the bulk bag is positioned on a support frame, and the system uses a mechanical or pneumatic cutter to open the top of the bag. The opened bag is then supported by a discharge chute, which allows the powder to flow into a hopper or conveyor system. The discharge rate is controlled by adjusting the opening size of the chute or using a variable-speed motor for the conveyor. A dust collection system, typically equipped with a filter and blower, captures any airborne particles, ensuring compliance with environmental regulations and maintaining a clean working environment. The entire process is automated, reducing the need for manual intervention and minimizing the risk of product contamination or operator exposure to dust.
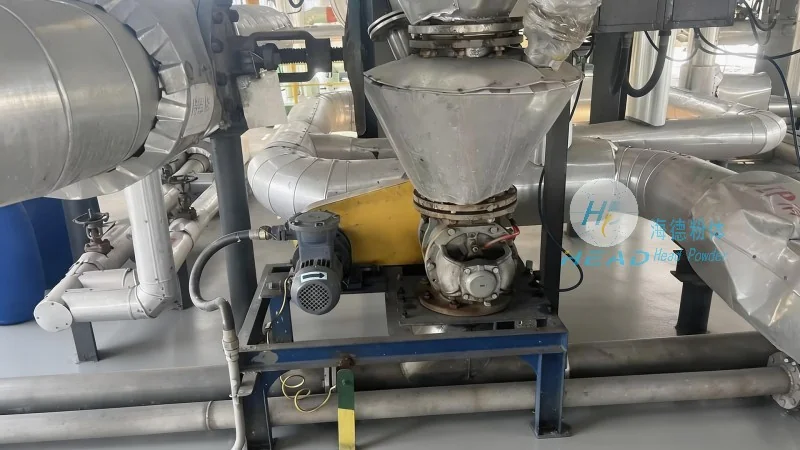
This equipment is widely used in industries such as chemical manufacturing, food processing, and pharmaceutical production, where bulk bag handling is a critical step in material supply. In chemical plants, it facilitates the safe and efficient transfer of raw materials like powders and granules, reducing the time required for manual unloading and minimizing the risk of spills or contamination. In food processing facilities, the system ensures hygienic handling of ingredients, maintaining product quality and compliance with food safety standards. For pharmaceutical manufacturers, the equipment's sterile design and contamination control features are essential for handling sensitive materials. The operational benefits include increased throughput, reduced labor costs, improved safety, and enhanced product quality due to consistent handling conditions.
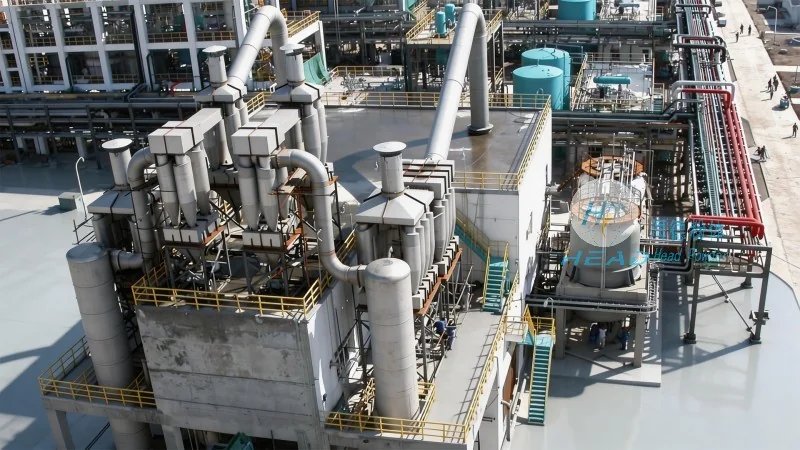
HeadPowder offers customization options to meet specific customer requirements. The equipment can be integrated with existing conveyor systems, storage silos, or processing lines, ensuring seamless operation within the production workflow. Options include different discharge capacities, material handling capacities, and compatibility with various bag sizes (e.g., 1-ton to 2.5-ton bags). Additionally, the system can be equipped with data logging and monitoring features, allowing real-time tracking of material flow and equipment performance. This flexibility enables customers to optimize their operations and adapt to changing production needs.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top