For industries dealing with powders and bulk materials, efficient and reliable conveying systems are crucial for smooth operations. The equipment designed for this purpose, such as pneumatic conveyors, screw conveyors, and bucket elevators, plays a vital role in transporting materials from one location to another within a production facility. Understanding the underlying principles and the specific characteristics of different working scenarios is essential for selecting the right equipment for a given application.
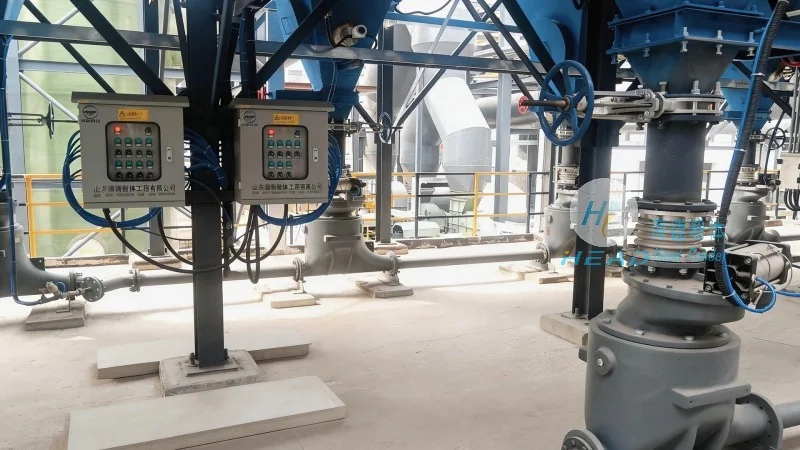
The fundamental principle behind powder and bulk material conveying is the movement of solid particles through a conveying medium, often air or a mechanical component. Pneumatic conveying systems utilize compressed air to create a flow that carries the material through a pipeline. This method is particularly effective for fine powders and granules, as it minimizes material degradation and contamination. In contrast, mechanical conveyors like screw conveyors and belt conveyors rely on mechanical force to move the material. Screw conveyors use a rotating screw to push the material forward, making them suitable for handling dry, free-flowing materials. Bucket elevators, on the other hand, use a series of buckets attached to a chain or belt to lift and transport materials vertically, which is ideal for vertical material transfer in industrial settings.
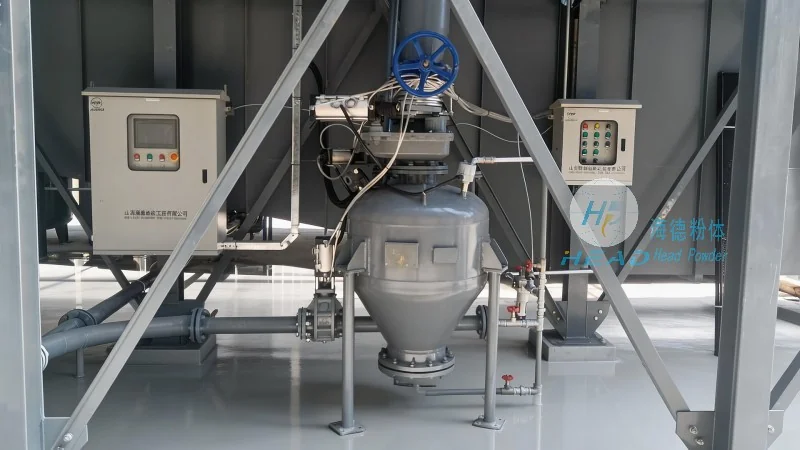
The working scene characteristics of powder and bulk material conveying equipment vary significantly based on the industry and the specific requirements of the application. In the food and pharmaceutical industries, where hygiene and product purity are paramount, dust-tight and sanitary conveyors are essential. These systems are designed to prevent cross-contamination and ensure that the material remains clean throughout the conveying process. For example, in a food processing plant, a pneumatic conveyor with a stainless steel construction and sealed components would be used to transport flour or sugar, maintaining the quality and safety standards required by regulatory bodies.
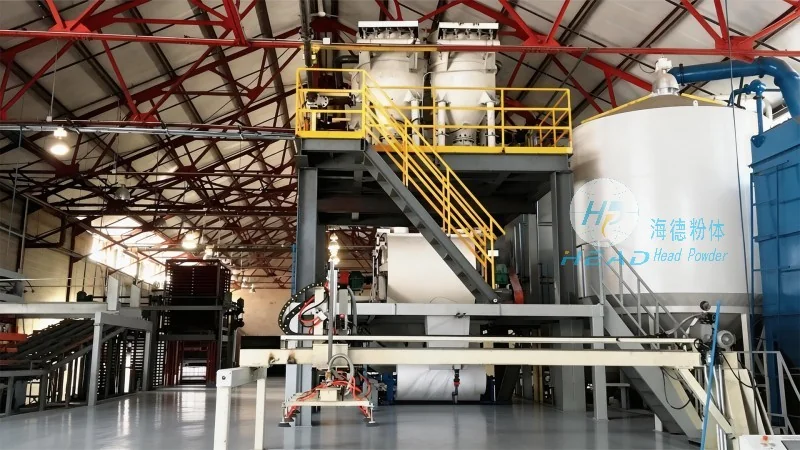
In the chemical and mining industries, where materials are often abrasive and heavy, robust and durable conveying equipment is necessary. Screw conveyors with high-strength materials, such as stainless steel or special alloys, are commonly used to handle corrosive or abrasive powders. These conveyors are designed to withstand the harsh conditions and ensure long-term operation with minimal maintenance. Similarly, bucket elevators in mining operations are built to handle large volumes of bulk materials like coal or ore, with heavy-duty components that can endure the demanding environment.
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer in the field of powder and bulk material handling, specializes in providing customized conveying solutions tailored to the unique needs of various industries. With a strong focus on innovation and quality, the company has developed a wide range of conveying equipment, including pneumatic conveyors, screw conveyors, and bucket elevators, to meet the diverse requirements of its clients. HeadPowder's products are designed to enhance operational efficiency, reduce downtime, and improve overall productivity in material handling processes.
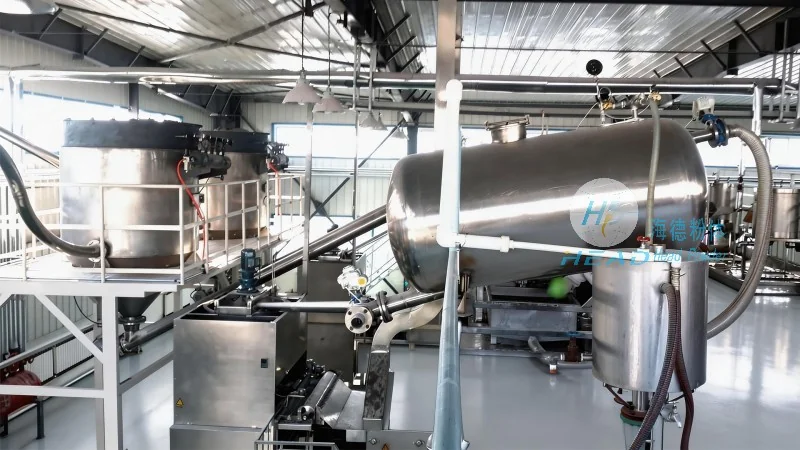
The company's headquarters is located in Shandong, China, where it operates a state-of-the-art manufacturing facility equipped with advanced technology and skilled workforce. This enables HeadPowder to produce high-quality equipment that meets international standards and customer expectations. By leveraging its expertise in material handling technology, HeadPowder continues to serve industries worldwide, helping businesses optimize their material transport processes and achieve their operational goals.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top