HeadPowder, a leading engineering company based in Shandong, China, specializes in the design and manufacturing of advanced bulk bin pneumatic conveying systems. These systems are engineered to efficiently transfer bulk materials from storage bins to processing units, offering a reliable solution for industries requiring consistent and clean material handling.
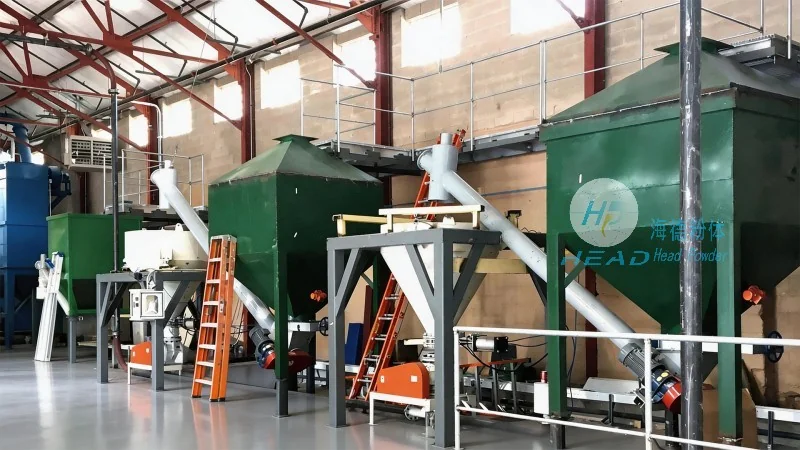
Bulk bin pneumatic conveying systems utilize air as the primary medium to transport dry bulk materials. The technology is widely adopted across various sectors due to its ability to handle a wide range of materials, including powders, granules, and fine particles. The system typically consists of a bulk bin, a conveying line, and a control unit, ensuring seamless material transfer from the storage container to the destination point.
The core principle of pneumatic conveying involves the use of air pressure to move materials through a pipeline. In positive pressure systems, air is forced into the conveying line, creating a flow that propels the material forward. Conversely, negative pressure systems draw air and material through the line using a vacuum. This method eliminates the need for mechanical components like belts or screws, reducing maintenance and increasing operational efficiency. The system's flexibility allows for both horizontal and vertical transport, adapting to the layout of industrial facilities.
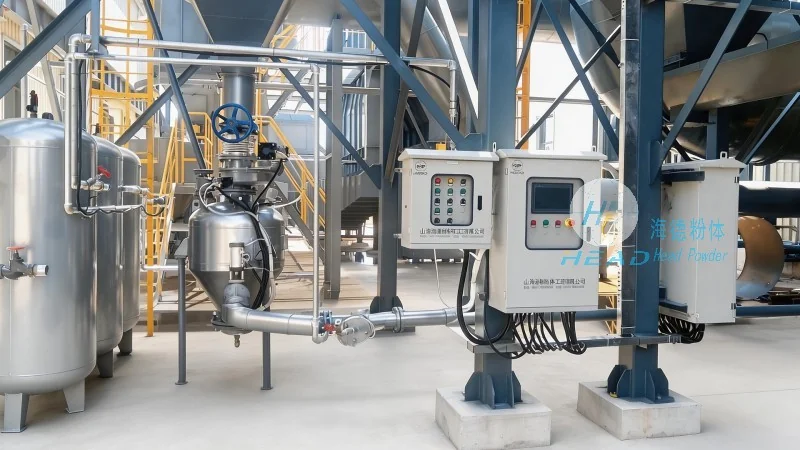
Bulk bin pneumatic conveying systems offer several advantages that make them ideal for modern industrial applications. One of the most significant benefits is the ability to maintain a clean and dust-free environment, as the enclosed pipeline prevents material spillage and contamination. Additionally, these systems provide high transfer rates, enabling continuous operation and minimizing downtime. The modular design allows for easy integration with existing infrastructure, and the low maintenance requirements contribute to long-term cost savings. Furthermore, the systems are capable of handling materials with varying moisture content and particle sizes, making them versatile for diverse industrial needs.
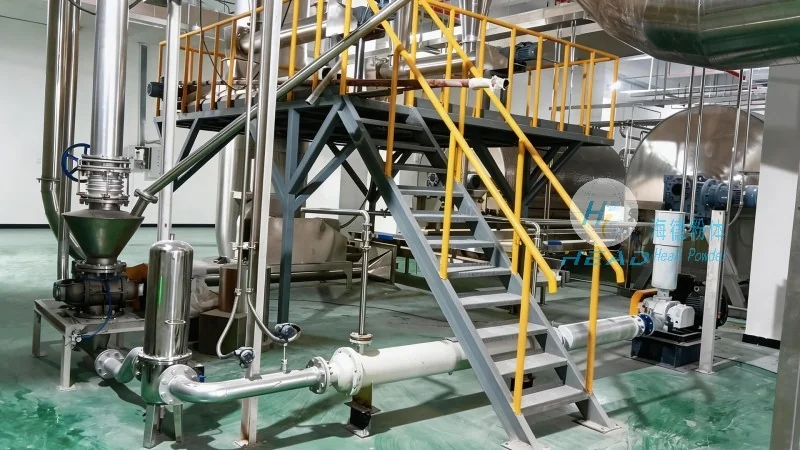
The application of bulk bin pneumatic conveying systems spans multiple industries, each benefiting from the technology's efficiency and reliability. In the chemical industry, these systems are used to transport raw materials and finished products, ensuring safe and controlled handling of hazardous substances. The food and pharmaceutical sectors rely on the systems' hygienic design to maintain product purity and compliance with regulatory standards. Manufacturing plants utilize the technology for in-plant material transfer, streamlining production processes and improving overall workflow. Even in the agricultural sector, bulk bin pneumatic conveyors are employed to move grain and other agricultural products from storage to processing facilities, enhancing operational efficiency.
HeadPowder understands that each industrial environment has unique requirements. Therefore, the company offers customized bulk bin pneumatic conveying solutions tailored to specific operational needs. Engineers at HeadPowder work closely with clients to assess material characteristics, facility layout, and production goals, ensuring the system is optimized for maximum performance. The integration of advanced control systems allows for real-time monitoring and adjustment of conveying parameters, enhancing process control and reducing waste. Additionally, the company provides comprehensive after-sales support, including maintenance services and technical assistance, to ensure the longevity and reliability of the installed systems.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top