HeadPowder, a leading manufacturer based in Shandong, China, specializes in advanced pneumatic conveying systems tailored for the cocoa processing industry. This article explores the fundamental principles behind cocoa pneumatic conveying machines and highlights their key working scene characteristics, providing insights into how these systems enhance operational efficiency and product quality in cocoa handling applications.
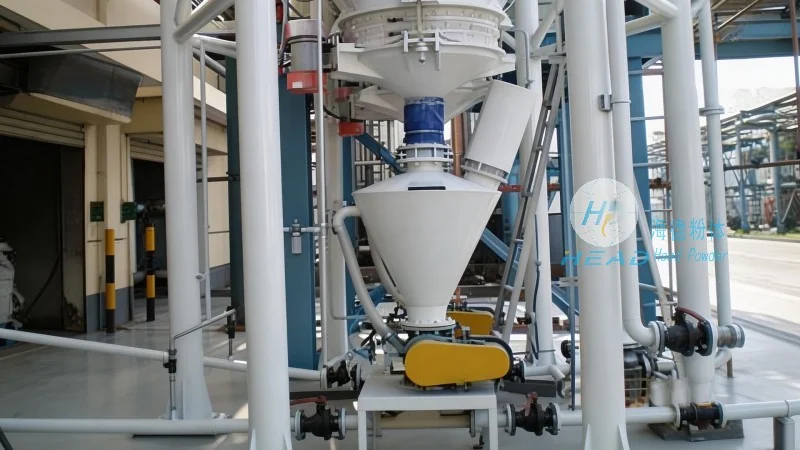
Cocoa pneumatic conveying machines are sophisticated equipment designed to transport cocoa powders, nibs, and other cocoa-related materials through a pressurized or vacuum system. Unlike traditional mechanical conveyors, these systems utilize air or gas to move bulk materials, offering advantages such as reduced contamination, improved hygiene, and the ability to handle sensitive products without mechanical contact. HeadPowder's expertise in engineering custom solutions ensures that these machines are optimized for the unique demands of cocoa processing, from raw material handling to finished product packaging.
The fundamental principle of cocoa pneumatic conveying involves the use of a pressure differential to move materials through a pipeline. In a typical system, a fan or blower generates airflow that propels the cocoa particles. The system can operate in either positive pressure (where air is forced into the pipeline) or negative pressure (where air is drawn out, creating a vacuum). The choice between these modes depends on the specific application, material characteristics, and system layout. For cocoa, which is often fine and abrasive, positive pressure systems are commonly preferred as they provide better control over particle flow and reduce the risk of blockages. HeadPowder's engineers carefully select the appropriate air velocity and pressure levels to ensure efficient and reliable transport while minimizing wear on components.
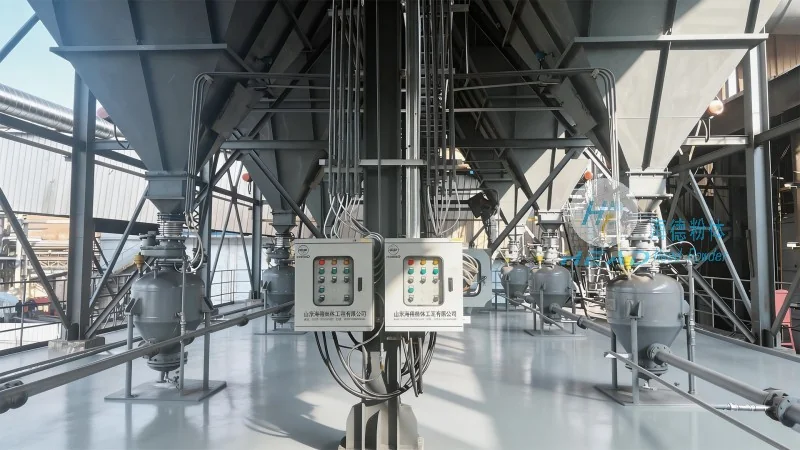
The working scene characteristics of cocoa pneumatic conveying machines are tailored to meet the diverse needs of cocoa processing facilities. These systems are typically deployed in scenarios where materials need to be moved over long distances, through multiple processing stages, or between different areas of a facility. For instance, in a cocoa processing plant, a pneumatic conveyor might be used to transport freshly ground cocoa powder from the grinding department to the packaging line, or to move cocoa nibs from storage silos to the roasting equipment. The flexibility of these systems allows for integration with existing infrastructure, reducing the need for extensive site modifications. Additionally, HeadPowder's designs prioritize space efficiency, making them suitable for both large-scale industrial operations and smaller processing facilities.
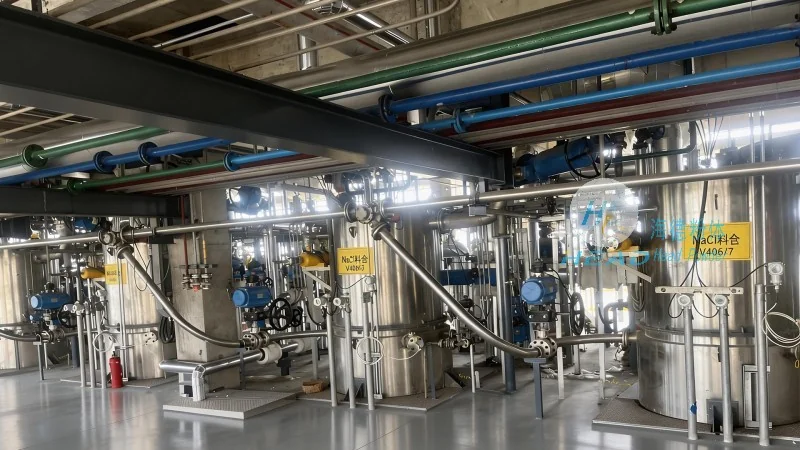
Implementing cocoa pneumatic conveying machines in processing environments offers several key advantages. Firstly, the hygienic design of these systems minimizes the risk of product contamination, which is critical in food processing industries. The enclosed pipelines and controlled airflow prevent exposure to dust, moisture, and external contaminants, ensuring that the cocoa remains in pristine condition. Secondly, the systems enhance operational efficiency by automating material transport, reducing labor costs, and improving throughput. Unlike manual or mechanical conveyors, pneumatic systems can operate continuously without the need for frequent maintenance or adjustments. Thirdly, the ability to handle fine and abrasive materials without causing degradation makes these machines ideal for cocoa, which can be easily damaged by mechanical friction. HeadPowder's solutions are engineered to withstand the abrasive nature of cocoa particles, extending the lifespan of components and reducing downtime.
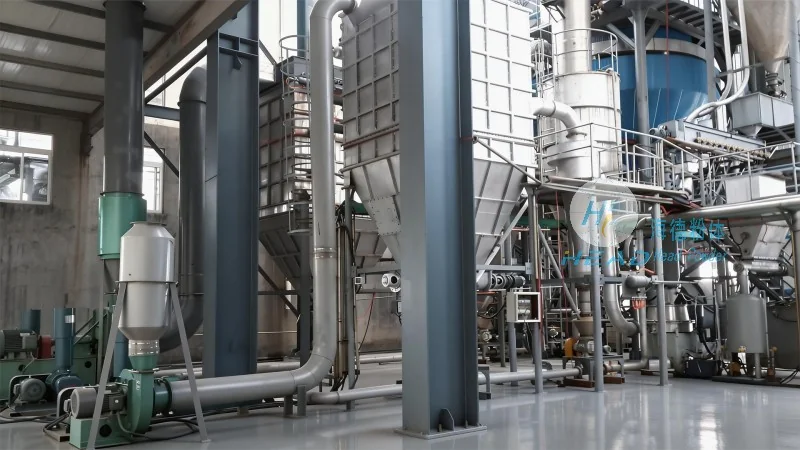
HeadPowder understands that each cocoa processing facility has unique requirements. Therefore, their pneumatic conveying systems are highly customizable to fit specific operational needs. The company offers a range of options, including different pipeline materials (such as stainless steel or plastic), control systems, and integration with other processing equipment. For example, a facility might require a system that connects to existing silos and packaging lines, or one that handles high-volume production with minimal downtime. HeadPowder's engineering team works closely with clients to design systems that meet their exact specifications, ensuring seamless integration and optimal performance. The company also provides comprehensive support, including installation, training, and maintenance services, to help clients maximize the benefits of their investment.
In conclusion, cocoa pneumatic conveying machines represent a sophisticated solution for efficient and hygienic material transport in the cocoa processing industry. By leveraging the principles of pneumatic conveying, these systems enhance operational efficiency, maintain product quality, and reduce the risk of contamination. HeadPowder's expertise in designing and manufacturing custom solutions ensures that clients receive equipment tailored to their specific needs, whether for large-scale industrial operations or smaller processing facilities. With their focus on quality, customization, and customer support, HeadPowder continues to be a trusted partner in the cocoa processing sector, helping facilities optimize their operations and improve overall productivity.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top