Calcium oxide, or quicklime, is a critical chemical compound widely utilized in industries such as construction, steel manufacturing, and chemical processing. The efficient and safe transportation of calcium oxide from production sites to processing units is essential for maintaining production continuity and ensuring product quality. Pneumatic conveying systems have become a preferred method for handling calcium oxide due to their ability to transport bulk materials without direct contact with mechanical components, thereby reducing material loss and contamination risks. This article explores the operational principle of calcium oxide pneumatic conveying machines and outlines the key working scene characteristics that define their effectiveness in industrial applications.
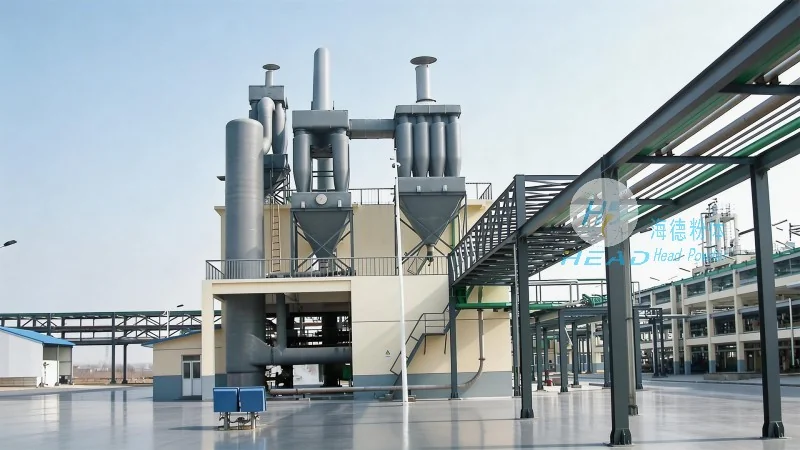
Calcium oxide pneumatic conveying machines operate based on the fundamental principle of transporting bulk solids through a pipeline using air or other gases as the conveying medium. The system typically consists of a material hopper for storage, a rotary airlock valve to control material discharge, a conveying pipeline, and a receiver for material collection. The process begins with calcium oxide being fed into the hopper. The rotary valve then regulates the flow of material into the conveying line, ensuring a consistent and controlled discharge rate. Compressed air is introduced into the pipeline, creating a high-velocity air stream that entrains the calcium oxide particles and propels them toward the receiver. The velocity of the air and the design of the pipeline—including bends, elbows, and expansion joints—are critical factors that determine the efficiency and effectiveness of the conveying process. By maintaining the air velocity above the material's terminal velocity, the system ensures that calcium oxide particles remain suspended and transported smoothly without clogging or deposition. This principle allows for the reliable and continuous movement of calcium oxide, even over long distances and in varying environmental conditions.
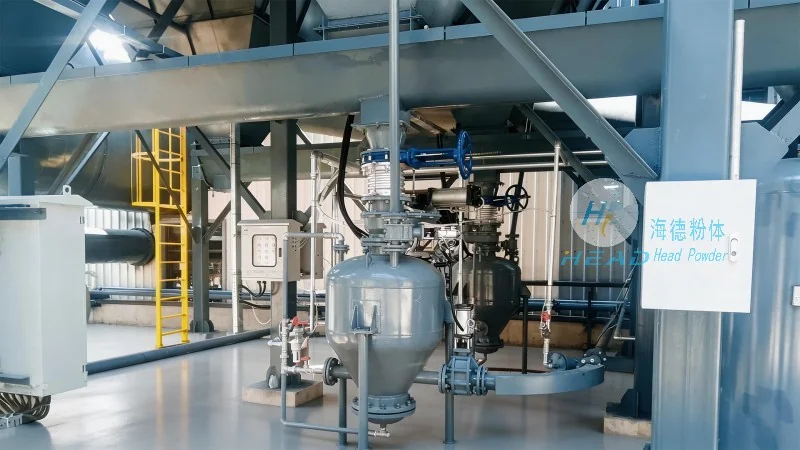
The working scene characteristics of calcium oxide pneumatic conveying machines are specifically tailored to meet the unique demands of industrial environments. These characteristics include: dust-free operation, which minimizes environmental impact and health risks associated with calcium oxide dust; reduced material loss, as the system prevents spillage and leakage during transportation; and improved safety, as there is no direct human contact with the material during the conveying process. Additionally, the system offers flexibility in terms of layout and integration with existing production lines, allowing for seamless incorporation into various industrial workflows. The ability to transport calcium oxide over long distances without the need for intermediate storage or handling points enhances operational efficiency and reduces downtime. The working scene characteristics also encompass the system's adaptability to different calcium oxide particle sizes and moisture content, ensuring consistent performance regardless of material variations. This adaptability makes calcium oxide pneumatic conveying machines suitable for a wide range of industrial applications, from small-scale laboratory use to large-scale industrial production.
Calcium oxide pneumatic conveying machines are widely adopted in various industrial sectors due to their versatility and efficiency. In the construction industry, they are used to transport calcium oxide for cement production and concrete mixing, where consistent material quality is critical. In steel manufacturing, calcium oxide is used as a flux in the steelmaking process, and pneumatic conveying ensures that the material is delivered to the furnace without contamination. The chemical processing industry also relies on these systems for transporting calcium oxide in the production of calcium-based chemicals, such as calcium chloride and calcium carbonate. The working scene characteristics of the machines, such as their ability to handle high volumes and long distances, make them ideal for large-scale production facilities. Furthermore, the dust-free operation of the system aligns with modern industrial standards for environmental compliance and occupational health, making it a preferred choice for companies operating in regulated environments.
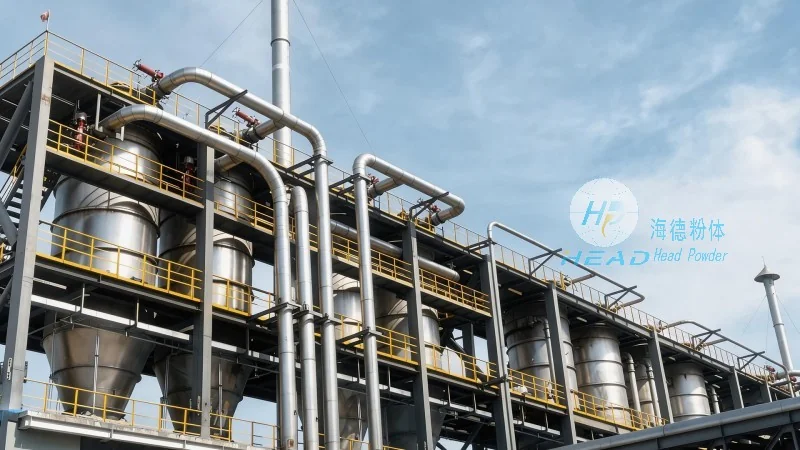
When evaluating calcium oxide pneumatic conveying machines for industrial use, several advantages and considerations must be taken into account. The primary advantage is the dust-free operation, which not only improves workplace safety but also reduces the need for additional dust control measures. The system also minimizes material loss, as the enclosed pipeline prevents spillage and leakage, ensuring that the entire batch of calcium oxide is delivered to the receiver. Another key advantage is the reduced maintenance requirements compared to traditional mechanical conveying systems, as there are fewer moving parts and less wear and tear on components. However, there are also considerations to keep in mind, such as the need for a reliable compressed air supply, as the performance of the system is directly dependent on the air pressure and flow rate. Additionally, the design of the conveying line must be optimized to prevent material buildup and clogging, especially when handling calcium oxide with high moisture content or fine particle sizes. Proper maintenance, including regular cleaning of the pipeline and rotary valve, is essential to ensure the long-term efficiency and reliability of the system.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top