Food processing industries increasingly rely on efficient and hygienic material handling solutions to maintain product quality and operational efficiency. Among the advanced technologies available, food pneumatic conveying systems stand out as a versatile and effective method for transporting bulk materials. This article explores the fundamental principles behind these systems and highlights their key application scenarios, with a focus on the expertise of Shandong HeadPowder Engineering Co., Ltd., a leading provider in the field.
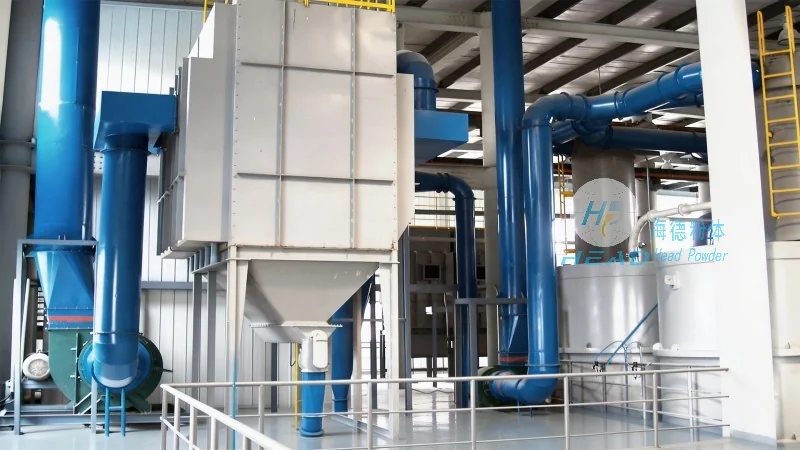
Food pneumatic conveying systems utilize air or gas to transport bulk materials such as powders, granules, and other food products through a pipeline network. Unlike traditional mechanical conveyors, these systems offer advantages like minimal product contamination, reduced risk of cross-contamination, and the ability to handle sensitive or hygienically sensitive materials. The core of a pneumatic conveying system lies in its ability to create a flow of material by generating pressure differentials or using vacuum to move the product through the system.
At the heart of food pneumatic conveying is the principle of fluidization and transport. The system typically consists of a hopper, a conveying line, a control unit, and a discharge point. The process begins when material is fed into the hopper. A fan or blower then generates airflow, either by creating a vacuum (suction system) or pressure (pressure system), to move the material along the pipeline. The choice between suction and pressure systems depends on the application requirements, including the distance, material characteristics, and desired flow rate.
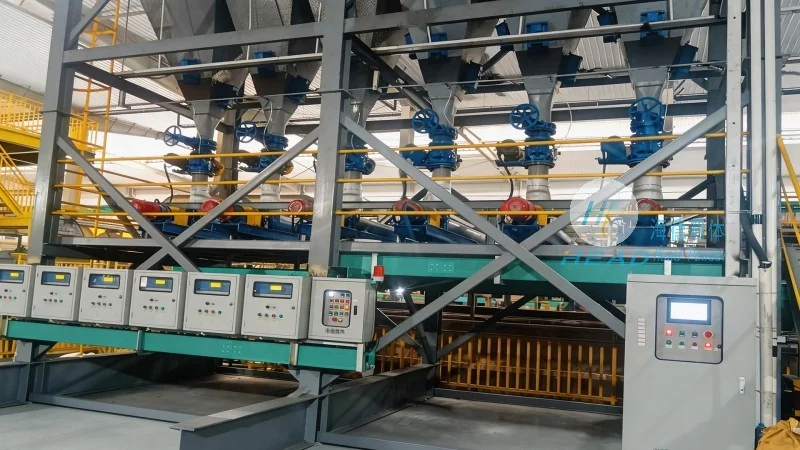
There are two primary types of pneumatic conveying systems used in food processing: suction (or vacuum) systems and pressure systems. Suction systems operate by creating a negative pressure in the pipeline, drawing material from the source. These systems are ideal for short to medium distances and are commonly used for transferring materials from a single source to a single destination. Pressure systems, on the other hand, use positive pressure to push material through the pipeline. They are suitable for longer distances and can handle more material at higher speeds. Both systems can be further classified into dilute-phase and dense-phase conveying, each offering different flow characteristics and efficiency levels.
Food pneumatic conveying systems find extensive applications across various stages of food production. In the initial processing stage, these systems are used to transport raw materials from storage silos to processing lines. For example, in flour mills, pneumatic conveyors efficiently move wheat or other grains from storage to grinding equipment, ensuring a continuous and clean flow. During the processing stage, they are employed to transfer intermediate products, such as ground powders or mixed ingredients, between different processing units. This is crucial in maintaining the quality and consistency of the final product.
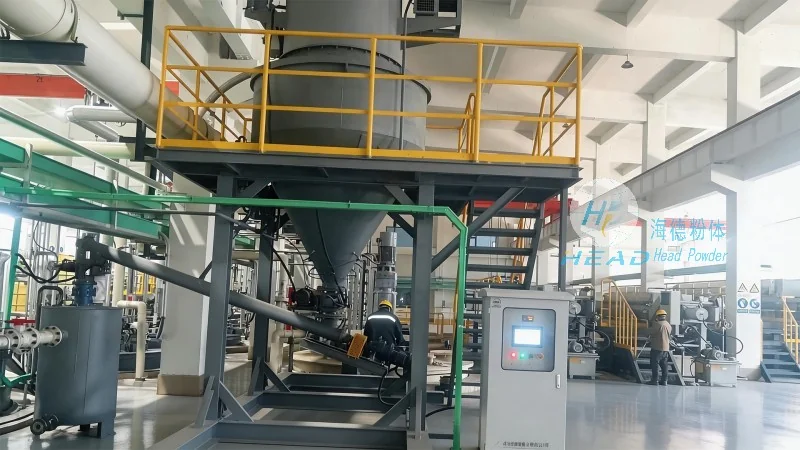
One of the most significant advantages of food pneumatic conveying is its hygienic design. The enclosed pipeline system minimizes exposure to contaminants, ensuring that the product remains clean and safe for consumption. Additionally, these systems are easy to clean and maintain, which is essential for compliance with food safety regulations. Another key benefit is the flexibility in system design. Pneumatic conveyors can be easily integrated with existing production lines, allowing for modifications and expansions as needed. They also offer high efficiency in material transport, reducing labor costs and improving overall productivity.
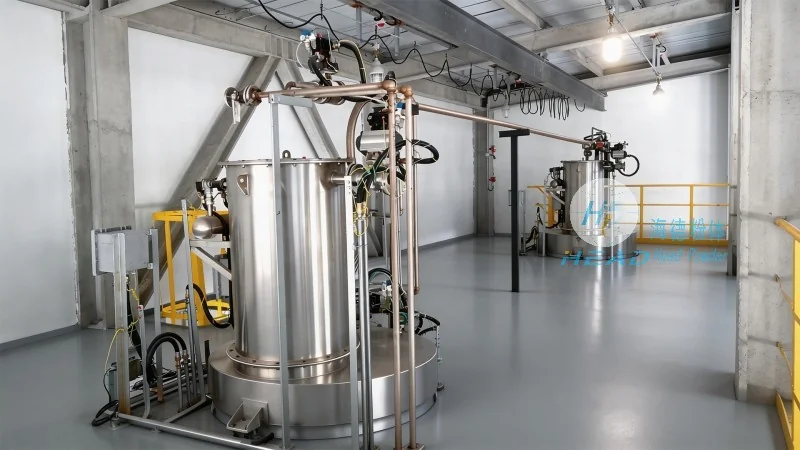
Consider a large-scale bakery that produces various baked goods. The facility uses a food pneumatic conveying system to transport flour from storage silos to the mixing and baking areas. The suction system, equipped with a hopper and a fan, efficiently draws flour from the silos and delivers it to the mixing tanks. This setup ensures a consistent supply of flour, reducing downtime and improving the quality of the baked products. The system’s hygienic design also helps maintain the cleanliness of the bakery, adhering to strict food safety standards.
Food pneumatic conveying systems represent a sophisticated solution for the efficient and hygienic handling of bulk food materials. Their ability to maintain product integrity, reduce contamination risks, and adapt to various production needs makes them indispensable in modern food processing. Shandong HeadPowder Engineering Co., Ltd., with its expertise in designing and manufacturing these systems, plays a vital role in supporting the food industry’s operational efficiency and safety standards. By leveraging advanced technology and adhering to strict quality control, the company ensures that its pneumatic conveying solutions meet the highest industry requirements, providing reliable and effective material handling for food processing facilities worldwide.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top