Malt is a vital ingredient in the brewing industry, and efficient handling of this raw material is essential for maintaining production quality and operational efficiency. Pneumatic conveying machines offer a reliable solution for transporting malt from storage to processing areas. This article explores the fundamental principles behind malt pneumatic conveying technology and highlights key working scene characteristics that make such systems effective in industrial settings. The insights shared here are based on the expertise of Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer specializing in bulk material handling solutions for the food and beverage industry.
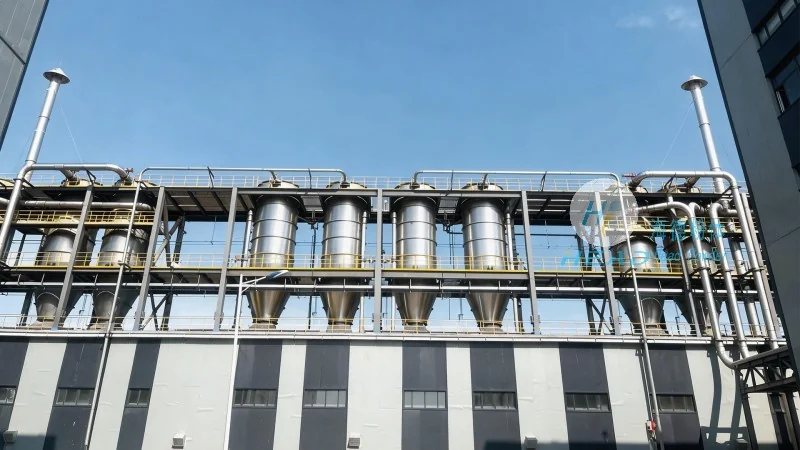
The principle of pneumatic conveying involves the use of air or gas to transport bulk materials like malt through a pipeline system. In the case of malt, which is typically dry and granular, the conveying process relies on creating a flow of air that carries the material particles. This method eliminates the need for mechanical components such as belts or buckets, reducing maintenance requirements and enhancing safety. The system operates by generating a pressure differential, either through positive pressure (where air is forced into the line) or negative pressure (where air is drawn out), to move the malt from the source to the destination. The air flow is carefully controlled to ensure consistent particle suspension and prevent material settling or blockages.
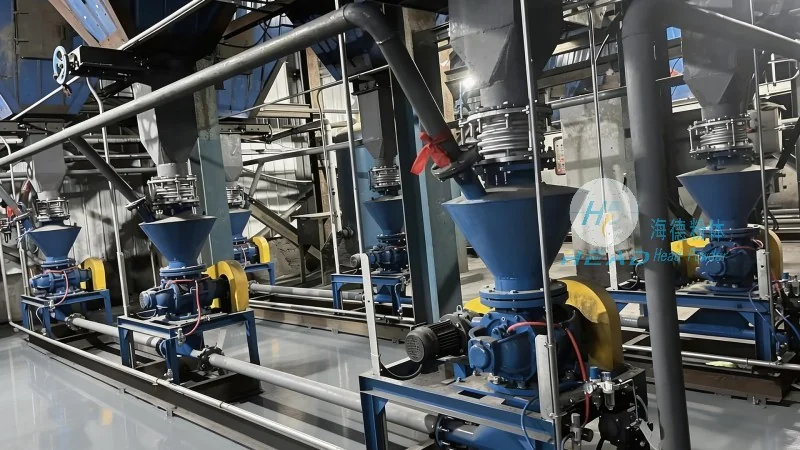
Several distinct characteristics define the effectiveness of malt pneumatic conveying systems in real-world applications. First, the system's ability to handle abrasive materials without significant wear on components is critical, as malt can be somewhat abrasive. The design of the conveying line, including the use of appropriate materials like stainless steel or specialized coatings, ensures longevity and minimal maintenance. Second, the flexibility of pneumatic systems allows for easy integration into existing production lines, enabling manufacturers to adapt to changing production needs without major infrastructure changes. Third, the system's capacity to transport malt over long distances with minimal loss of material quality is a significant advantage, as it maintains the integrity of the grain during transit. Additionally, the ability to handle varying malt types, such as different varieties or moisture contents, without adjusting the system significantly makes these machines versatile for diverse brewing operations. The enclosed pipeline design also minimizes dust and contamination, which is vital for maintaining hygiene standards in food processing environments.
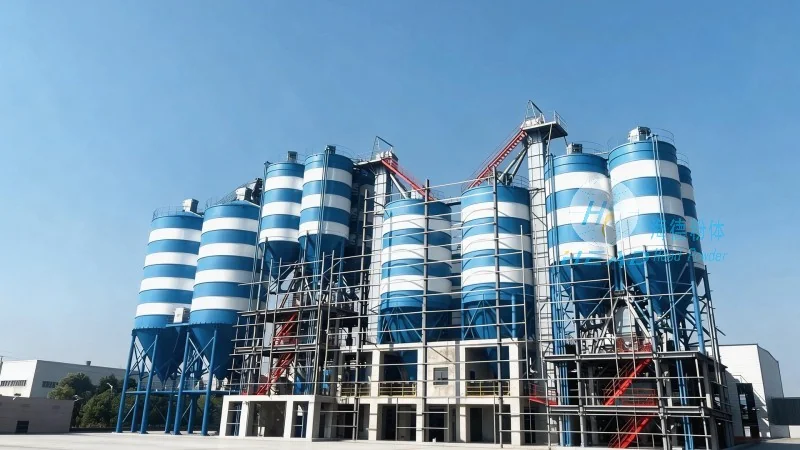
Malt pneumatic conveying machines are widely used in various stages of the brewing process. In storage facilities, these systems efficiently move malt from silos or bulk containers to the mashing or grinding areas. During the production phase, they can transport malt from the grinding mill to the mash tun, ensuring a steady supply of raw material. The systems are also employed in quality control areas, where malt is transferred for testing or sorting. The adaptability of the technology allows it to be used in both large-scale commercial breweries and smaller craft breweries, making it a versatile solution for different production scales. For example, in a large-scale brewery, a pneumatic conveying system might handle thousands of tons of malt annually, while in a craft brewery, a smaller, more compact system can efficiently manage the volume of malt required for daily production.
Implementing a malt pneumatic conveying system offers several advantages. The primary benefit is the reduction in labor costs associated with manual handling of malt, as the system automates the transport process. Additionally, the enclosed pipeline system minimizes dust and contamination, which is crucial for maintaining hygiene standards in food processing environments. The system also allows for better control over the moisture content of the malt during transport, preventing issues like clumping or spoilage. However, there are considerations to keep in mind, such as the initial investment cost, which may be higher than traditional mechanical conveyors. Maintenance requirements, particularly for the air filtration and pressure control systems, also need to be factored into the operational budget. Furthermore, the system's performance can be affected by factors like the moisture content of the malt and the air pressure, requiring regular monitoring and adjustments to ensure optimal operation. Proper sizing of the air compressor and pipeline diameter is essential to prevent excessive energy consumption or material degradation.
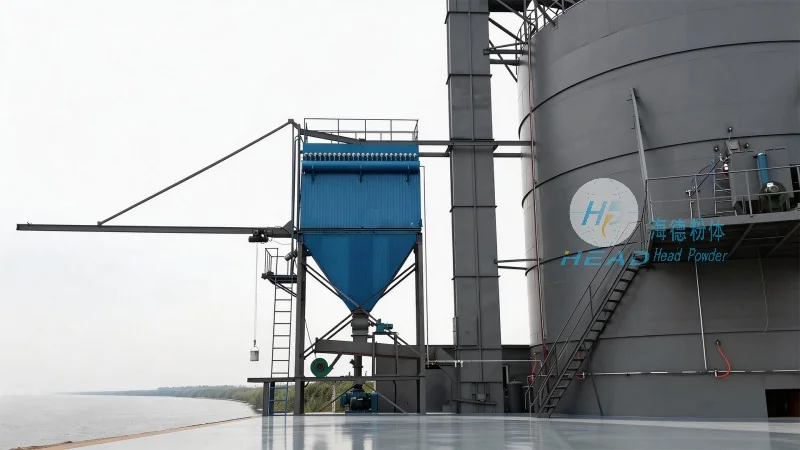
Malt pneumatic conveying machines represent a sophisticated and efficient solution for handling malt in the brewing industry. By leveraging the principles of pneumatic transport, these systems provide reliable, flexible, and hygienic material handling capabilities. The working scene characteristics, including durability, adaptability, and long-distance transport, make them suitable for diverse industrial applications. As the brewing industry continues to evolve, the adoption of such advanced conveying technologies ensures that manufacturers can maintain high production standards while optimizing operational efficiency. Shandong HeadPowder Engineering Co., Ltd. continues to lead in providing tailored solutions for breweries, delivering high-quality equipment that enhances the overall efficiency of malt handling processes and supports the growth of the brewing industry. With a focus on innovation and customer satisfaction, the company ensures that its pneumatic conveying systems meet the specific needs of each client, contributing to the success of their brewing operations.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top