HeadPowder, a leading engineering firm based in Shandong, China, specializes in the design and implementation of advanced material handling solutions. Among their portfolio is the ammonium nitrate pneumatic conveying system, a critical technology for efficiently transporting this vital industrial chemical. This article delves into the fundamental principles behind such systems and highlights the key characteristics of their operational environments.
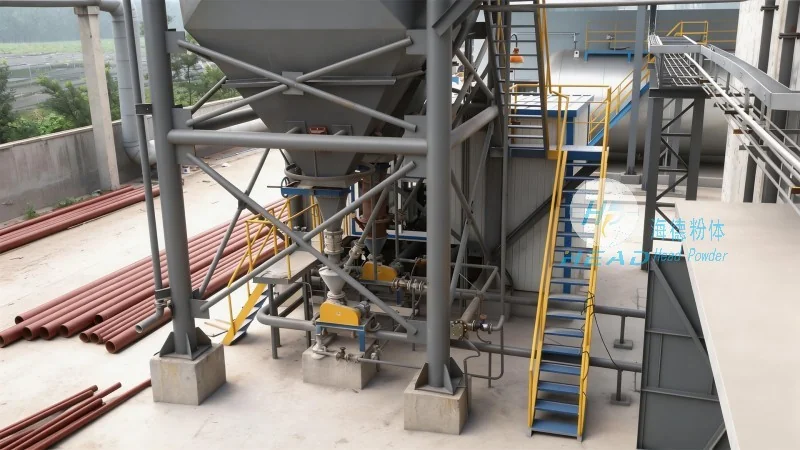
The pneumatic conveying system operates on the principle of using compressed air to move solid materials through a pipeline. In the case of ammonium nitrate, a fine, granular chemical, the system relies on a combination of air pressure and velocity to create a flow that transports the material from the source to the destination. The process typically involves a hopper or feeder that feeds the ammonium nitrate into a duct, where high-pressure air is introduced. This air, moving at sufficient velocity, lifts and propels the particles through the pipeline. The system may use either positive pressure (where air is forced into the system) or negative pressure (where air is drawn out), depending on the specific application and layout. The design of the system, including the size of the duct, the air velocity, and the pressure differentials, is crucial for ensuring efficient and reliable transport without causing material degradation or system blockages.
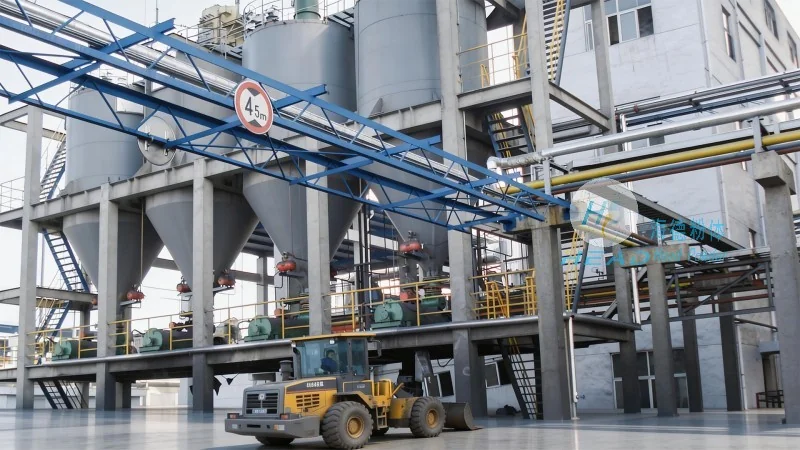
The operational environments for ammonium nitrate pneumatic conveying systems are characterized by several distinct features that impact their design and performance. First, the material itself—ammonium nitrate—is a highly sensitive chemical, requiring careful handling to prevent caking, agglomeration, or degradation. The system must be designed to maintain the material's granular structure and prevent moisture absorption, which can affect its flow properties and stability. Second, the systems are often integrated into large-scale industrial facilities, such as fertilizer plants or chemical processing plants, where space constraints and the need for continuous operation are paramount. This necessitates robust, durable equipment that can withstand heavy usage and potential environmental factors like temperature fluctuations or dust exposure. Third, safety is a critical consideration due to the explosive nature of ammonium nitrate under certain conditions. The systems incorporate safety features, including explosion-proof components, pressure relief valves, and monitoring systems, to mitigate risks and ensure compliance with industrial safety standards. Additionally, the systems are designed for scalability, allowing for adjustments in capacity based on production needs, and often include automation features to enhance operational efficiency and reduce human error.
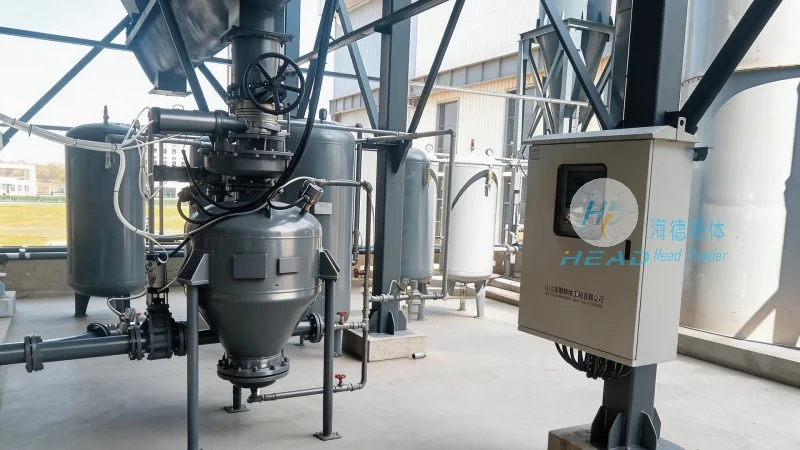
Ammonium nitrate pneumatic conveying systems are widely used in various industrial applications, particularly in the fertilizer industry, where they play a vital role in the production and distribution of nitrogen-based fertilizers. The systems enable the efficient transport of ammonium nitrate from storage silos to processing units, mixing equipment, or packaging lines. In such scenarios, the ability to handle large volumes of material with minimal downtime is essential for maintaining production schedules and meeting market demands. The operational advantages of these systems include reduced labor costs, as automated feeding and conveying eliminate the need for manual handling of heavy or hazardous materials. Additionally, the systems offer improved safety by minimizing human exposure to the chemical and reducing the risk of accidents associated with manual handling. From a maintenance perspective, pneumatic conveying systems are generally more compact and require less space compared to traditional belt or bucket elevators, making them suitable for facilities with limited floor space. The systems also provide better control over material flow, allowing for precise dosing and mixing, which is critical in chemical manufacturing processes.
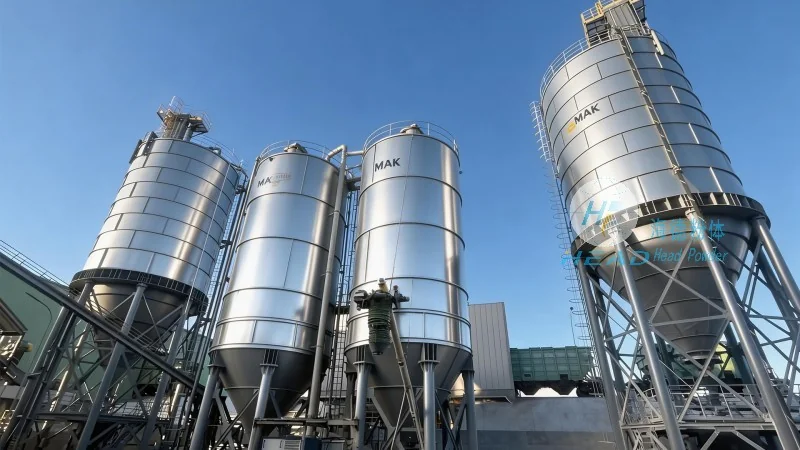
For industrial facilities dealing with ammonium nitrate, the pneumatic conveying system represents a sophisticated solution that balances efficiency, safety, and reliability. By understanding the core principles of air-based transport and the specific characteristics of the working environment, engineers at HeadPowder can design systems tailored to the unique needs of each client. The integration of robust components, safety features, and automation ensures that these systems operate effectively in demanding industrial settings. As a company based in Shandong, China, HeadPowder leverages its expertise in engineering to provide customized solutions that enhance productivity and safety in the handling of critical materials like ammonium nitrate. The continued development and application of such advanced material handling technologies are essential for meeting the evolving demands of the industrial sector and ensuring the safe and efficient operation of chemical processing facilities.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top