Microsphere powder pneumatic conveying systems represent a sophisticated technology designed to transport fine powders efficiently through an air-based medium. This method is particularly advantageous for materials like microsphere powders, which require precise handling to maintain quality and consistency. The system operates by using compressed air to create a flow that carries the powder particles through a pipeline network, ensuring minimal degradation and loss during transport.
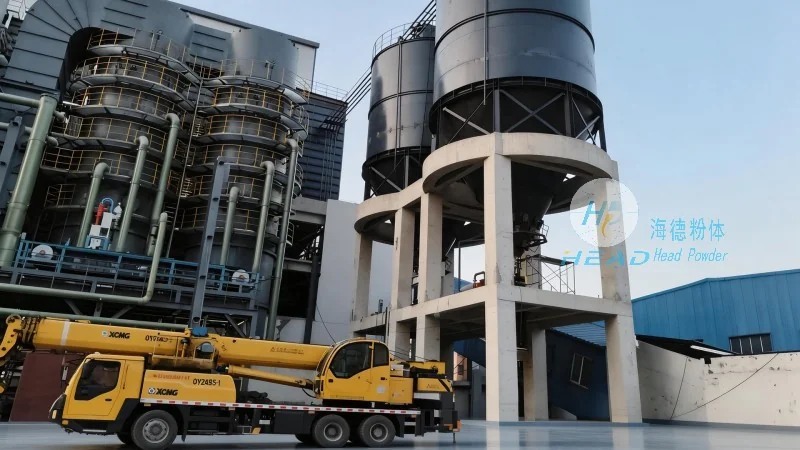
At the heart of microsphere powder pneumatic conveying is the principle of fluidization and suspension. Compressed air is introduced into the conveying line, creating a turbulent flow that lifts and transports the powder particles. This process relies on the balance between the air velocity and the particle size, density, and shape. For microsphere powders, which often have uniform particle sizes and specific physical properties, the system is optimized to maintain a stable suspension, preventing clogging or deposition in the pipeline. The design typically includes components such as a feeder, a conveying line, and a receiver, each playing a critical role in the overall operation.
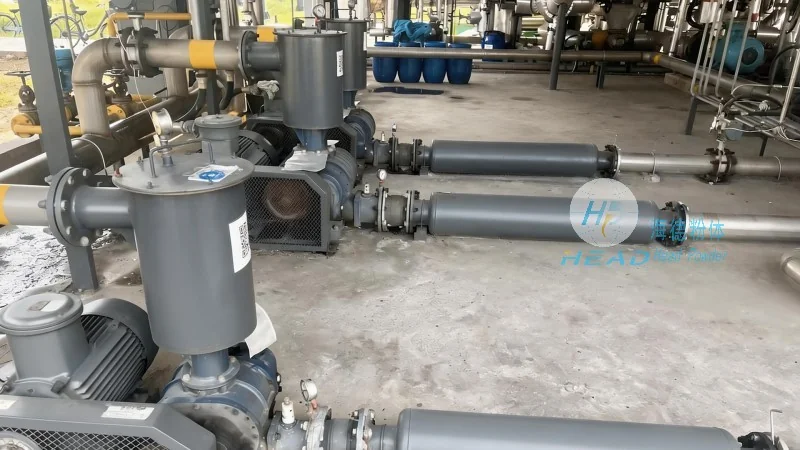
The effectiveness of a microsphere powder pneumatic conveying system hinges on its key components. The feeder is responsible for accurately metering the powder and introducing it into the conveying line. This component must handle the specific characteristics of microsphere powders, such as their fine particle size and potential for static charge, to ensure consistent flow. The conveying line itself is constructed from materials resistant to corrosion and abrasion, as microsphere powders can be abrasive and may cause wear over time. The receiver, or discharge unit, collects the transported powder and separates it from the air, often using filters or cyclones to maintain purity. Each component is carefully engineered to work in harmony, ensuring the system operates reliably and efficiently.
Microsphere powder pneumatic conveying systems are widely used in various industrial applications, including pharmaceuticals, food processing, and chemical manufacturing. Their working scene characteristics are tailored to the specific demands of each industry. For example, in pharmaceutical applications, the system must meet stringent hygiene and contamination control standards, with components designed to be easily cleaned and sterilized. In food processing, the system is often used to transport ingredients like microsphere powders for confectionery or nutritional products, where product purity and safety are paramount. The benefits of this technology include reduced labor costs, improved material handling efficiency, and enhanced product quality due to minimal exposure to external contaminants. Additionally, the system allows for flexible and scalable operations, adapting to varying production volumes and process requirements.
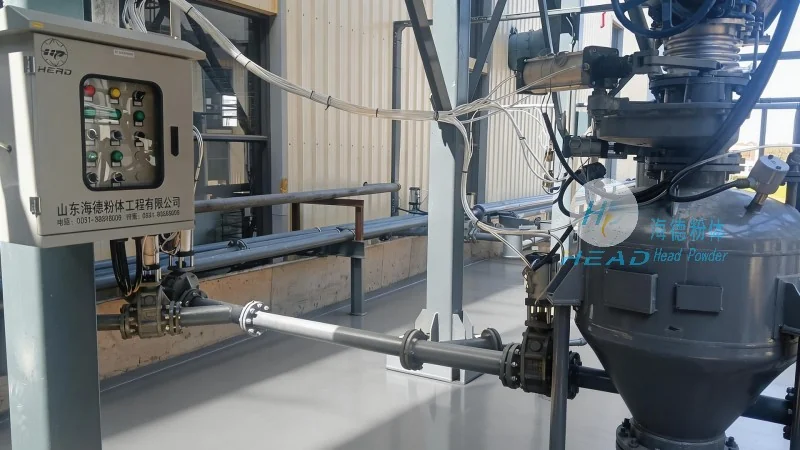
HeadPowder, a leading provider of pneumatic conveying solutions, specializes in designing and manufacturing systems tailored to the unique needs of microsphere powder applications. With a focus on innovation and quality, the company has established itself as a trusted partner in the industry. HeadPowder's systems are engineered to deliver reliable performance, ensuring that clients can meet their production targets while maintaining the highest standards of product integrity. The company's commitment to customer satisfaction and technical excellence has made it a preferred choice for businesses seeking advanced powder handling solutions. Based in Shandong, China, HeadPowder leverages its local expertise and resources to provide comprehensive support and service to its global clientele.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top