When it comes to efficiently transporting fine sand and stone materials, air-pneumatic conveying equipment has emerged as a highly effective solution in modern material handling. This technology offers a reliable and flexible method for moving bulk materials over short to medium distances, providing significant advantages over traditional mechanical conveying systems. Understanding the working principle and key features of such equipment is crucial for industries dealing with these materials, as it ensures optimal performance and operational efficiency.
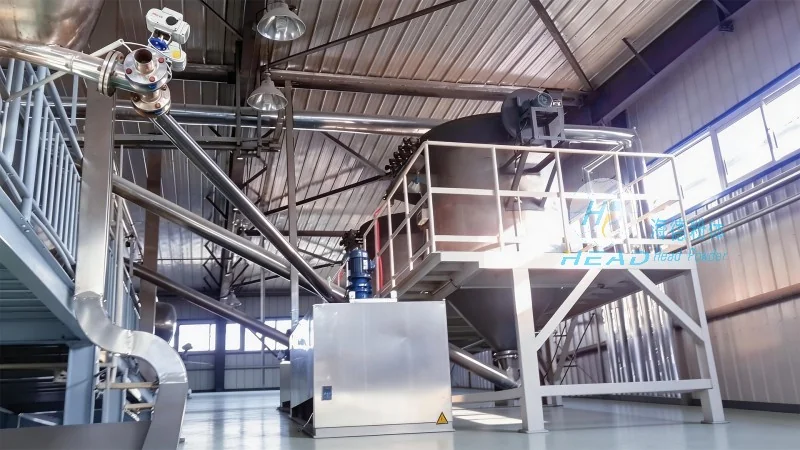
The core of air-pneumatic conveying systems lies in the use of compressed air to transport materials through a pipeline. The process typically involves several key components and steps. First, the material to be conveyed is fed into a hopper or feeder, where it is then drawn into the conveying line by the suction or pressure created by the air flow. The compressed air, often generated by a blower or fan, creates a flow that carries the particles along the pipeline. As the material travels through the system, it may encounter various components such as bends, filters, and separation units, which help maintain the integrity of the material and ensure smooth operation. The air-pneumatic system can operate under either positive pressure (where air is forced into the line) or negative pressure (where air is drawn out), depending on the specific requirements of the application. This flexibility allows for the adaptation of the system to different material types and operational conditions.
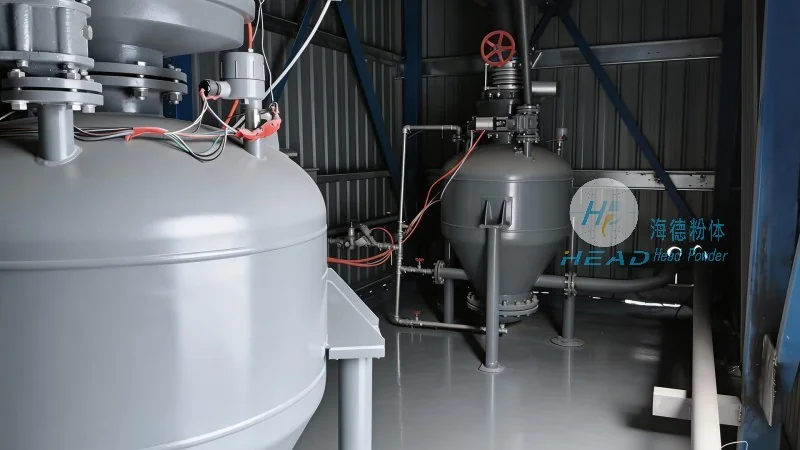
One of the primary advantages of air-pneumatic conveying equipment is its ability to handle fine and abrasive materials like sand and stone without causing excessive wear or damage. The smooth interior surfaces of the conveying pipes, often made from materials such as stainless steel or polyethylene, minimize friction and abrasion, extending the lifespan of the equipment. Additionally, the system provides excellent control over the flow rate and direction of the material, allowing for precise and consistent delivery to the destination. This is particularly important in applications where uniform material distribution is critical, such as in construction, mining, and manufacturing processes. Another notable feature is the hygienic and clean operation of the system. Unlike mechanical conveyors that may introduce contaminants or require frequent cleaning, air-pneumatic systems keep the material enclosed within the pipeline, reducing the risk of cross-contamination and ensuring compliance with health and safety regulations. Furthermore, the system is highly adaptable to different operational environments, including dusty or hazardous areas, as the material is contained within the air stream, preventing dust emissions and improving workplace safety.
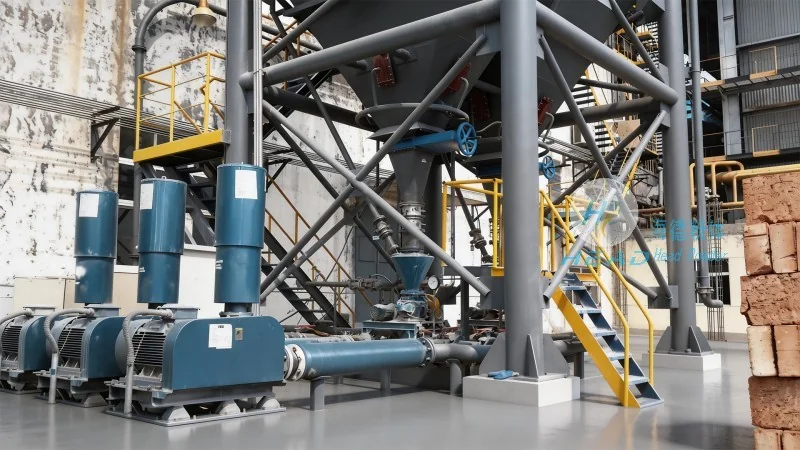
The adoption of air-pneumatic conveying equipment for fine sand and stone materials brings numerous operational benefits. Firstly, it significantly reduces labor costs by automating the material handling process, eliminating the need for manual loading and unloading. This not only increases productivity but also enhances workplace safety by minimizing human exposure to heavy or hazardous materials. Secondly, the system offers high efficiency in terms of energy consumption and material throughput. By using compressed air as the primary driving force, the equipment can transport large volumes of material over considerable distances with minimal energy input. This efficiency translates into lower operational costs and a faster return on investment. In terms of applications, air-pneumatic conveying is widely used in the construction industry for transporting sand, gravel, and other aggregates to job sites. It is also prevalent in mining operations for moving crushed stone and ore from processing plants to storage areas. Additionally, the system is utilized in manufacturing facilities for conveying raw materials to production lines and finished products to packaging areas. The versatility of the equipment makes it suitable for a wide range of industries, including chemical processing, food processing, and pharmaceuticals, where the handling of fine and sensitive materials is required.
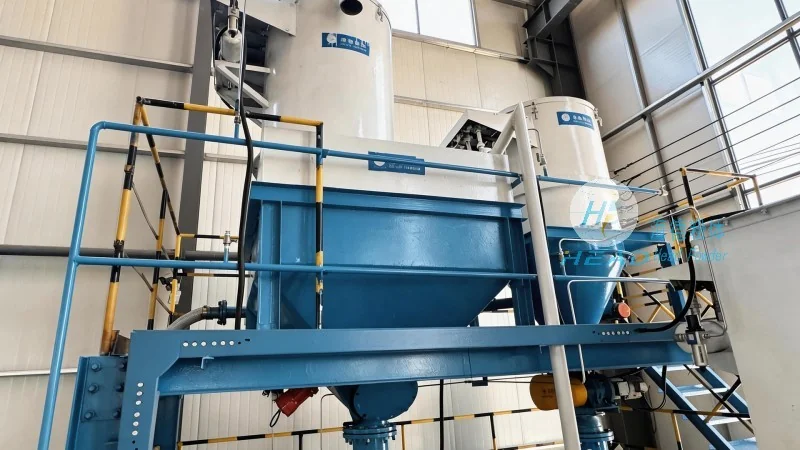
In conclusion, air-pneumatic conveying equipment for fine sand and stone materials is a sophisticated and efficient solution for modern material handling needs. Its working principle, based on compressed air to transport materials through a pipeline, offers a flexible and reliable method for moving bulk materials. The key features, including low wear, precise control, hygienic operation, and adaptability, make it an ideal choice for various industrial applications. The operational benefits, such as reduced labor costs, high efficiency, and improved safety, further enhance its appeal. As a leading provider in this field, Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing high-quality air-pneumatic conveying systems tailored to the specific needs of clients. With a focus on innovation and quality, the company ensures that its equipment meets the highest standards of performance and durability, providing long-term value to its customers. Based in Shandong, China, HeadPowder Engineering Co., Ltd. leverages its expertise and advanced technology to deliver cutting-edge solutions for material handling challenges, supporting industries in achieving their operational goals with efficiency and reliability.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top