For industrial applications involving sulfur pellets, efficient material handling is crucial. Pneumatic conveying systems offer a reliable solution for transporting these materials with precision and minimal maintenance. This article explores the working principle and key features of sulfur pellet pneumatic conveying equipment, highlighting how such systems enhance operational efficiency in processing facilities.
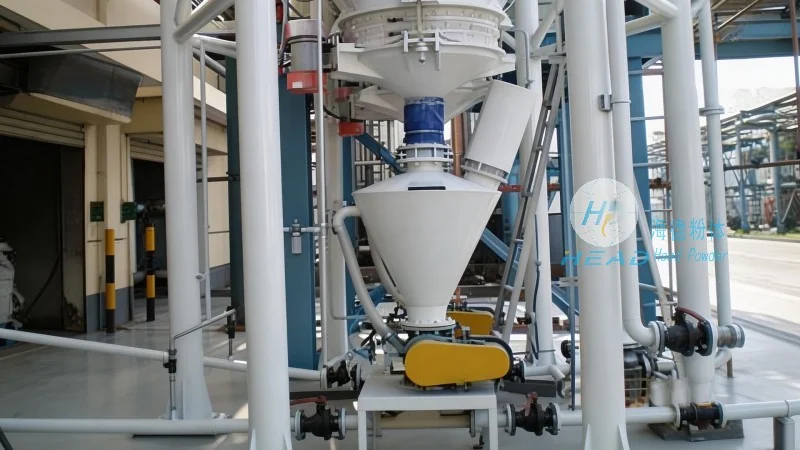
Pneumatic conveying, also known as air conveying, is a method of transporting bulk materials like sulfur pellets through a pipeline using air or gas as the conveying medium. Unlike mechanical systems that rely on belts, screws, or buckets, pneumatic systems utilize pressure differentials to move materials, making them ideal for applications where dust control, hygiene, and flexibility are priorities. The equipment typically consists of a feeding hopper, a conveyor line, and a discharge mechanism, all designed to handle the specific characteristics of sulfur pellets, which include their density, size, and potential for dust generation.
The core of a sulfur pellet pneumatic conveying system is its ability to create a consistent flow of material through the pipeline. The process begins with the material being fed into a hopper, where it is then introduced into the conveying line under controlled conditions. Air is then introduced into the system, either by a blower or a compressor, creating a pressure differential that propels the sulfur pellets forward. The velocity of the air and the design of the pipeline determine the efficiency of the conveying process. In positive pressure systems, air is blown into the pipeline, pushing the material along, while negative pressure systems draw material into the line using a vacuum. The choice between these systems depends on factors such as the distance to be covered and the material's properties. For sulfur pellets, positive pressure systems are often preferred due to their ability to handle longer distances and prevent material backflow.
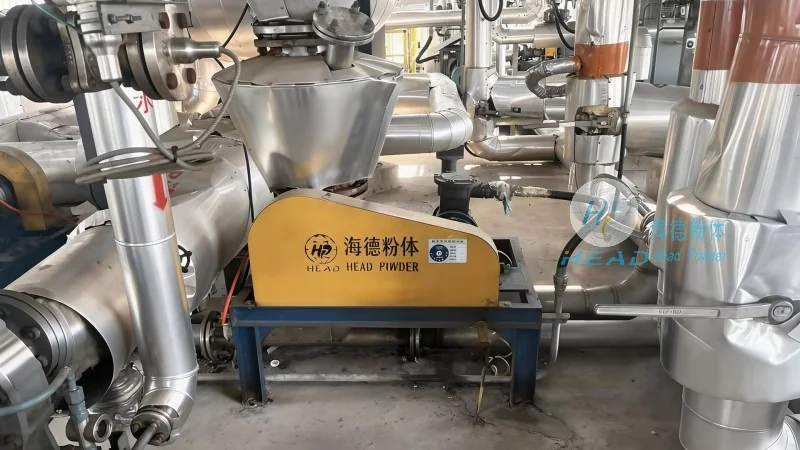
Several key features distinguish high-quality sulfur pellet pneumatic conveying equipment. First, the system's design must accommodate the abrasive nature of sulfur pellets, which can cause wear on components like the hopper and pipeline. Materials such as stainless steel or specialized coatings are commonly used to extend the lifespan of the equipment. Second, the system should incorporate effective dust control measures, as sulfur pellets can generate significant dust during handling. This includes features like cyclone separators and filtration systems that capture and remove dust particles, ensuring compliance with environmental regulations and maintaining a safe working environment. Third, the equipment must offer flexibility in terms of layout and material handling. Modular designs allow for easy integration into existing processing lines, and adjustable conveying rates enable operators to match the system's output to production demands. Additionally, advanced control systems provide real-time monitoring of pressure, flow, and material levels, allowing for immediate adjustments to optimize performance.
Implementing a pneumatic conveying system for sulfur pellets offers numerous benefits. One of the primary advantages is the reduction in labor costs associated with manual handling. The automated process minimizes the need for workers to handle heavy or dusty materials, improving workplace safety. Additionally, pneumatic systems can significantly reduce material loss and contamination, as the enclosed pipeline prevents exposure to external elements and reduces the risk of spillage. The efficiency of the system also leads to lower energy consumption compared to traditional mechanical conveying methods, resulting in cost savings over time. Furthermore, the flexibility of pneumatic systems allows for easy expansion or reconfiguration of the processing line as production needs change, providing long-term value to the facility.
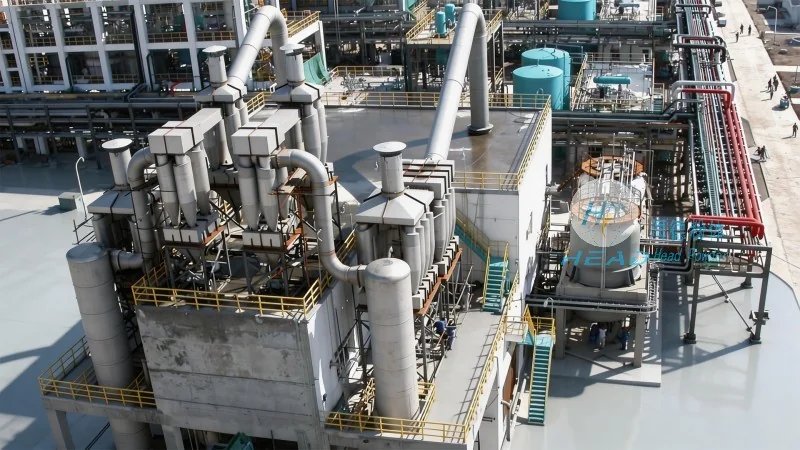
Sulfur pellet pneumatic conveying equipment is widely used in various industrial sectors, including chemical manufacturing, fertilizer production, and petrochemical processing. In chemical plants, these systems are essential for transporting sulfur pellets to reactors or storage tanks, ensuring a continuous supply of raw materials. In fertilizer production, the equipment is used to move sulfur pellets from storage to mixing and packaging units, maintaining consistent quality and reducing downtime. The petrochemical industry also relies on pneumatic conveying systems to transport sulfur pellets to sulfur recovery units, where they are processed into valuable byproducts. Each application benefits from the system's ability to handle the specific challenges of sulfur pellets, such as their tendency to clump or generate dust, while maintaining high efficiency and reliability.
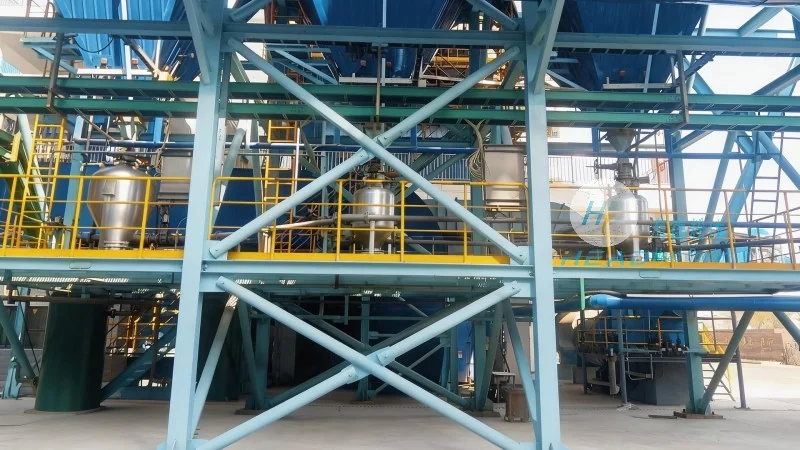
Proper maintenance is critical to ensuring the longevity and performance of sulfur pellet pneumatic conveying equipment. Regular inspections of the pipeline and components for signs of wear or damage are essential. The hopper and feeding mechanisms should be checked for blockages or material buildup, which can impede the flow of pellets. Additionally, the air filtration system must be maintained to prevent clogging, as dust accumulation can reduce the efficiency of the conveying process. Operators should also monitor the pressure and flow rates during operation, as fluctuations may indicate issues with the system. By following a regular maintenance schedule, facilities can minimize downtime and maximize the lifespan of their pneumatic conveying equipment.
When selecting a sulfur pellet pneumatic conveying system, it is important to consider the specific requirements of the application, including the material's properties, the distance to be covered, and the desired level of automation. The working principle and key features of the equipment, as outlined in this article, provide a solid foundation for making an informed decision. By investing in a high-quality system from a reputable manufacturer like Shandong HeadPowder Engineering Co., Ltd., facilities can enhance their operational efficiency, improve workplace safety, and reduce long-term costs. The flexibility and reliability of pneumatic conveying systems make them an ideal choice for handling sulfur pellets, ensuring consistent performance in demanding industrial environments.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top