For industries dealing with dry stone powder materials, efficient and reliable material handling solutions are crucial for maintaining production efficiency and ensuring product quality. Pneumatic conveying equipment, particularly designed for dry stone powders, offers a sophisticated method to transport these materials from one location to another without the need for mechanical components like belts or buckets. This article explores the working principle and key features of such equipment, highlighting how it meets the specific demands of handling dry stone powders.
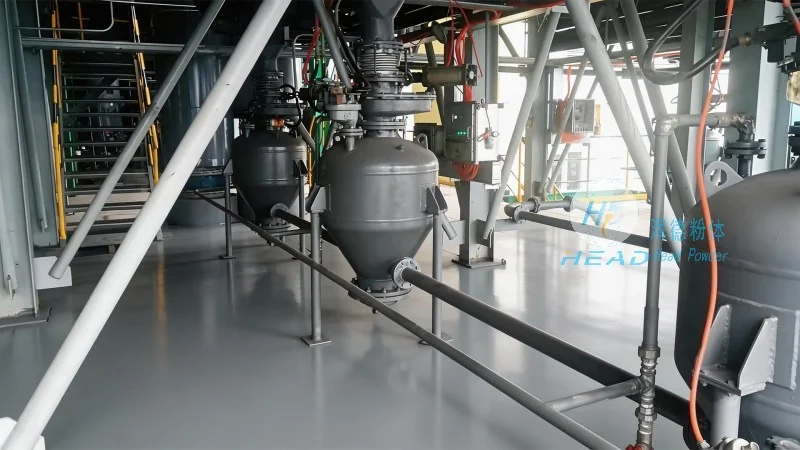
Pneumatic conveying systems are designed to transport dry bulk materials, including dry stone powders, using a stream of air or gas. Unlike traditional mechanical conveyors, these systems rely on the principles of fluid dynamics to move materials through a pipeline. The equipment is engineered to handle materials with varying particle sizes and moisture content, making it versatile for different industrial applications. The primary goal of pneumatic conveying is to provide a clean, dust-free, and efficient method of material transport, which is especially important for dry stone powders that may be sensitive to contamination or degradation during handling.
The operation of pneumatic conveying equipment for dry stone powders involves several key steps that work in tandem to ensure smooth material transport. The process typically begins with the material being fed into a hopper or feeder, where it is then introduced into a pipeline. A fan or blower creates a flow of air within the pipeline, generating a pressure differential that propels the material forward. The air velocity is carefully controlled to ensure that the material particles are suspended and carried along the pipeline without settling or causing blockages. The equipment may include components such as inlets, outlets, and filters to manage the flow and prevent material loss or contamination. The entire system is designed to maintain a consistent flow rate, ensuring that the dry stone powder is transported efficiently and safely to its destination.
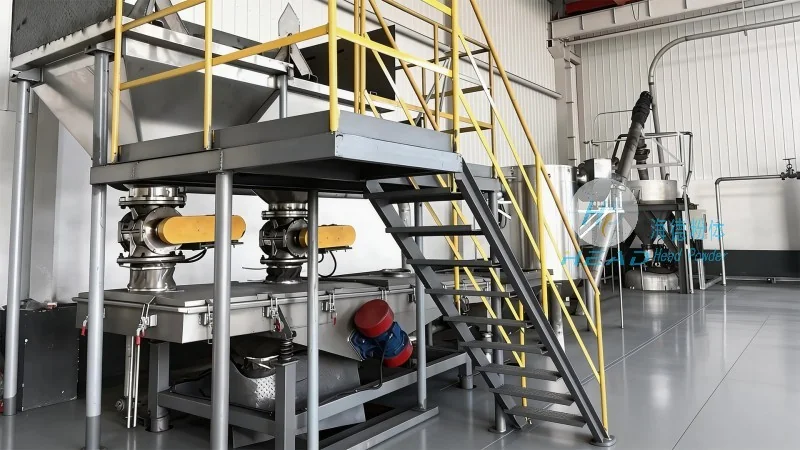
Several features make pneumatic conveying equipment ideal for handling dry stone powders. Firstly, the system provides a dust-free environment, which is critical for maintaining product purity and preventing respiratory hazards associated with dry stone powders. The enclosed pipeline design minimizes material exposure to the environment, reducing the risk of contamination and ensuring that the product remains in its original state. Secondly, the equipment offers high flexibility in terms of layout and installation, allowing it to be adapted to various plant configurations and space constraints. This flexibility is particularly beneficial for industries where space is limited or where the material handling system needs to be integrated with existing infrastructure. Thirdly, the system is capable of handling materials with varying particle sizes and moisture content, making it suitable for a wide range of dry stone powder applications. The ability to transport materials over long distances without the need for intermediate storage or transfer points also enhances operational efficiency. Additionally, the equipment is designed for low maintenance, with components that are easy to access and replace, reducing downtime and operational costs. The use of advanced materials and engineering in the construction of the equipment ensures durability and longevity, providing a reliable solution for long-term material handling needs.
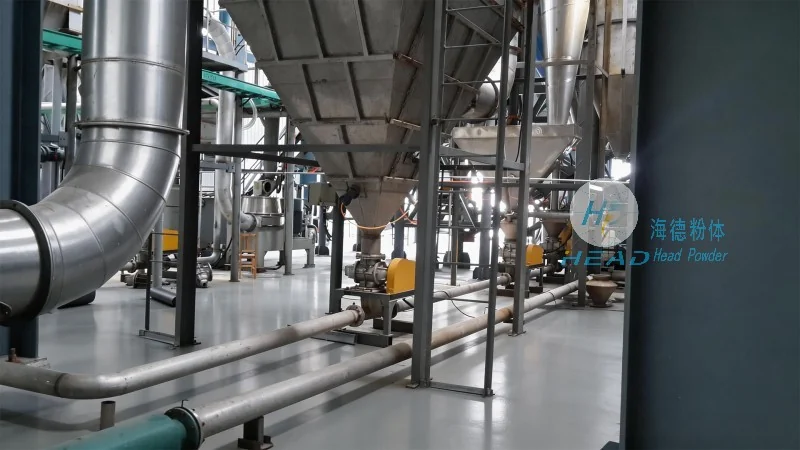
Pneumatic conveying equipment for dry stone powders finds applications in various industries, including construction, mining, and chemical processing. In the construction industry, it is used to transport dry stone powders for concrete production, ensuring a consistent and high-quality mix. In mining operations, the equipment is used to transport raw materials from storage to processing facilities, improving the overall efficiency of the mining process. The benefits of using pneumatic conveying in these applications include improved product quality, reduced labor costs, and enhanced safety due to the enclosed system design. The system also minimizes material waste by reducing spillage and loss during transport, contributing to cost savings and environmental sustainability. The ability to handle large volumes of material quickly and efficiently makes it an essential component in high-volume production environments.
Pneumatic conveying equipment for dry stone powders is a highly effective and versatile solution for material handling in various industrial applications. By understanding its working principle and key features, industries can make informed decisions about implementing this technology to improve their operational efficiency and product quality. The equipment, manufactured by companies like Shandong HeadPowder Engineering Co., Ltd. based in China, offers reliable and durable solutions tailored to the specific needs of handling dry stone powders. With its ability to provide a dust-free, efficient, and flexible material transport system, pneumatic conveying equipment continues to be a preferred choice for industries dealing with dry bulk materials.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top