Chocolate powder pneumatic conveying equipment is a specialized system designed to transport chocolate powder efficiently and reliably in industrial settings. This equipment plays a crucial role in the chocolate manufacturing process, ensuring that the powder is moved from storage to processing areas without degradation or contamination. The following sections will explore the working principle and key features of such equipment, providing insights into its functionality and benefits.
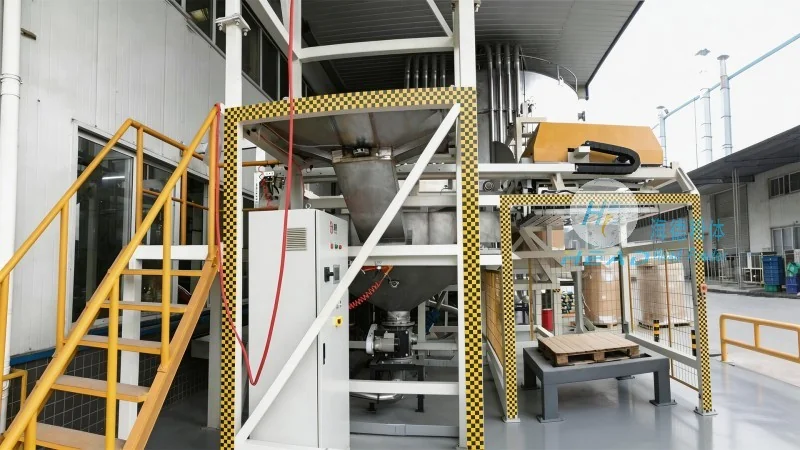
The core of chocolate powder pneumatic conveying equipment lies in the use of air to transport the powder. The system typically operates by creating a pressure differential between the inlet and outlet of the conveying line. A blower or compressor generates the necessary airflow, which is then directed through a pipeline. As the air flows, it draws the chocolate powder into the system via a hopper or inlet port. The powder is then carried along the pipeline by the air stream, moving to the desired destination. The process can be either positive pressure or negative pressure, depending on the specific design and application requirements. Positive pressure systems use a blower to push the air and powder mixture, while negative pressure systems use a vacuum to pull the material. This flexibility allows the equipment to be adapted to various production environments and material handling needs.
Chocolate powder pneumatic conveying equipment offers several advantages that make it an ideal choice for handling delicate and sensitive materials like chocolate powder. One of the primary features is its ability to maintain product integrity. The enclosed system prevents exposure to air, moisture, and contaminants, which can affect the quality and flavor of the chocolate powder. This is particularly important in food processing, where product safety and consistency are paramount. Additionally, the equipment is designed to minimize product degradation, such as caking or agglomeration, which can occur during traditional bulk handling methods. The smooth, continuous flow of the powder reduces the risk of breakage or damage, ensuring that the final product meets high standards.
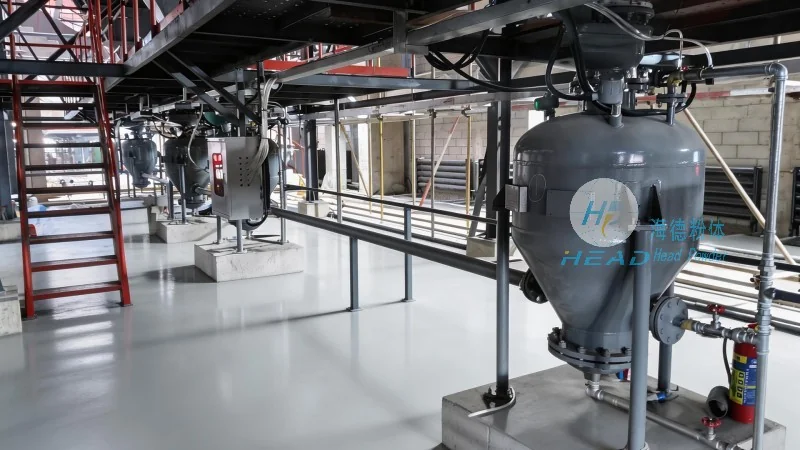
Another significant feature is the system's efficiency and versatility. Pneumatic conveying allows for the transport of chocolate powder over long distances and through multiple points of use, without the need for manual handling or intermediate storage. This streamlines the production process and improves overall operational efficiency. The equipment can be integrated with other processing machinery, such as mixers, ovens, or packaging lines, creating a seamless workflow. Furthermore, the system is easy to clean and maintain, which is essential for compliance with food safety regulations. The modular design enables quick disassembly and reassembly for cleaning, reducing downtime and ensuring consistent hygiene standards.
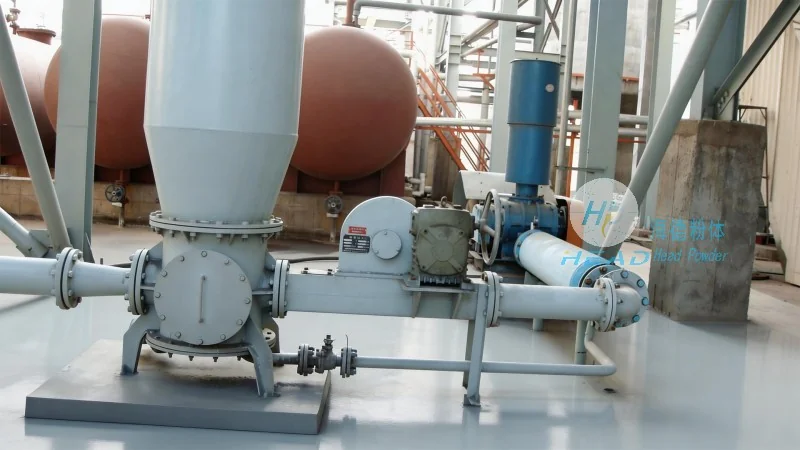
When selecting chocolate powder pneumatic conveying equipment, several factors must be considered to ensure optimal performance. The type of chocolate powder being handled—whether it is a fine powder, a coarse powder, or a mix with other ingredients—will influence the choice of equipment. For example, fine chocolate powders may require a higher air velocity to prevent clogging, while coarse powders might need a larger hopper and different nozzle designs. The system's capacity and flow rate must also be matched to the production volume. Overloading the system can lead to reduced efficiency and increased wear on components. Additionally, the environment where the equipment is installed, such as temperature and humidity levels, can impact the performance of the conveying system. Proper ventilation and temperature control are essential to maintain the quality of the chocolate powder during transport.
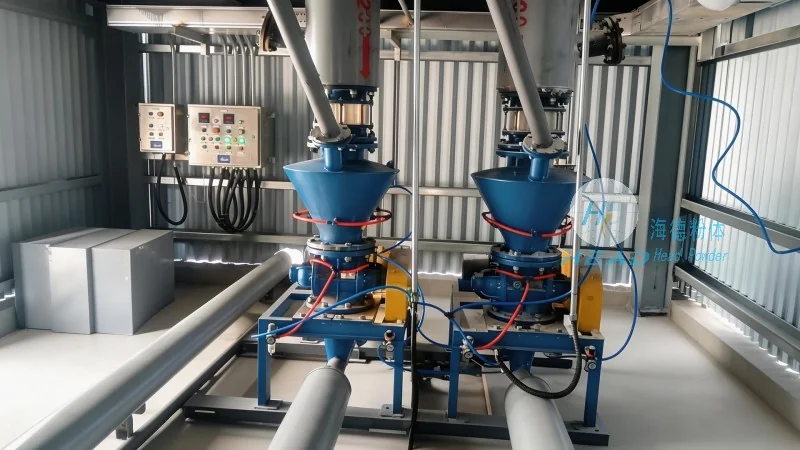
HeadPowder, a leading manufacturer of pneumatic conveying systems, specializes in providing customized solutions for chocolate powder handling. With over [years] of experience in the industry, HeadPowder understands the unique challenges of transporting delicate food products. The company's engineers work closely with clients to design systems that meet specific production requirements, ensuring that the equipment is both efficient and reliable. HeadPowder's products are known for their durability and low maintenance, which helps reduce operational costs over the long term. The company also offers comprehensive support, including installation, training, and after-sales service, to ensure that clients can maximize the benefits of their investment. By choosing HeadPowder, manufacturers can enhance their production processes, improve product quality, and maintain compliance with industry standards.
In conclusion, chocolate powder pneumatic conveying equipment is a vital component in modern chocolate manufacturing. Its ability to transport delicate materials efficiently while maintaining product integrity makes it an indispensable tool for food processors. The working principle, which relies on air to move the powder, and the key features, such as enclosed systems and easy maintenance, contribute to its effectiveness. When selecting a system, it is essential to consider the specific characteristics of the chocolate powder and the production environment. By partnering with a reputable manufacturer like HeadPowder, companies can ensure that they have the right equipment to meet their needs and achieve optimal performance. The investment in a reliable pneumatic conveying system not only improves operational efficiency but also enhances the quality of the final chocolate products, contributing to the success of the business.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top