HeadPowder Engineering Co., Ltd., a leading manufacturer in the field of material handling solutions, specializes in the design, development, and implementation of advanced pneumatic conveying systems tailored for the sugar industry. This article explores the fundamental principles behind these systems and highlights key application scenarios that demonstrate their efficiency and versatility in handling sugar materials.
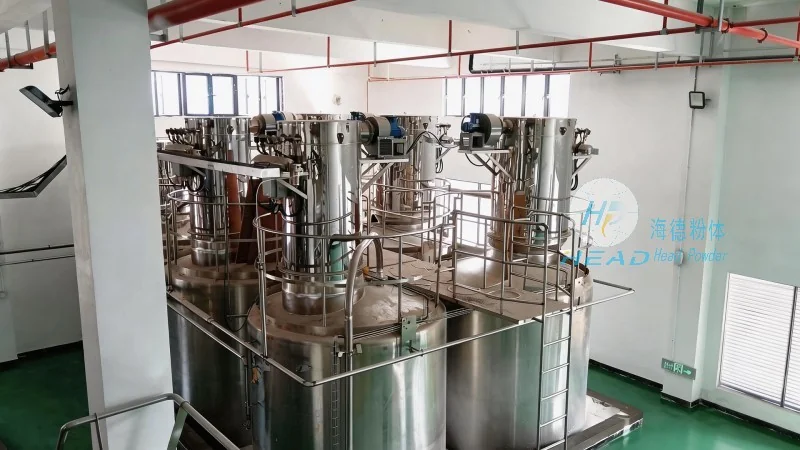
Pneumatic conveying systems operate by transporting bulk materials, such as sugar, through a pipeline using air or gas as the conveying medium. The technology leverages the principles of fluid dynamics to move materials from one location to another without the need for mechanical components like belts or buckets. There are primarily two types of pneumatic conveying systems: pressure and vacuum systems. Pressure systems use compressed air to push material through the pipeline, while vacuum systems create a negative pressure to draw material into the system. For sugar applications, the choice of system depends on factors like material characteristics, distance, and the need for gentle handling to prevent product degradation.
Effective pneumatic conveying for sugar materials relies on several critical components that work in tandem to ensure smooth operation. The main components include the hopper or feeder, which feeds the sugar into the system; the conveyor line, which transports the material; the air compressor or vacuum pump, which provides the necessary pressure or vacuum; and the discharge device, which releases the sugar at the destination. Each component is designed to handle the specific properties of sugar, such as its granular structure and potential for caking, ensuring minimal product loss and maximum efficiency. For instance, the feeder may use a rotary valve or a screw feeder to maintain a consistent flow rate, preventing blockages and ensuring the air flow remains stable. The pipeline itself is typically made of stainless steel or other corrosion-resistant materials to withstand the acidic or sugary environment and to maintain hygiene standards required in food processing.
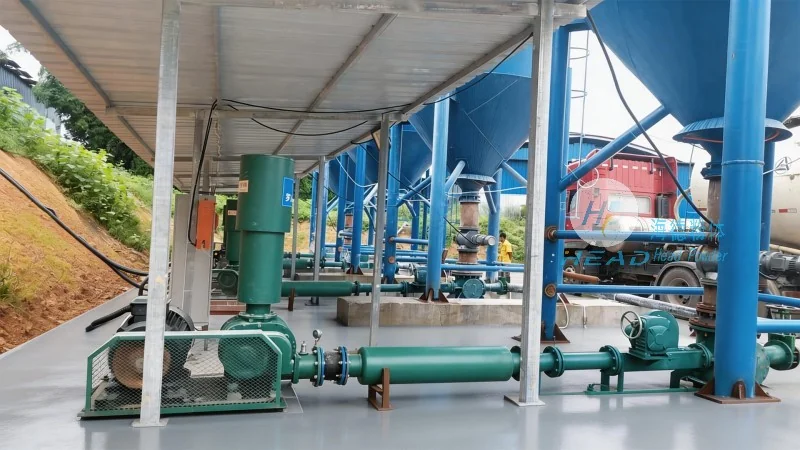
The versatility of pneumatic conveying systems makes them suitable for a wide range of applications within the sugar industry. One common scenario is the transfer of raw sugar from storage silos to processing equipment, such as crushers or mills. In this case, a pressure system is often used to move the sugar efficiently over short to medium distances, with the system designed to handle the high volume and density of raw sugar. Another application is the conveying of refined sugar from the refining process to packaging lines. Here, the system must maintain the purity of the sugar, which requires gentle handling and minimal exposure to contaminants. Pneumatic conveying is also used in the transportation of sugar from production facilities to storage or distribution centers, allowing for seamless integration with existing logistics networks.
Compared to traditional material handling methods like belt conveyors or bucket elevators, pneumatic conveying offers several advantages when handling sugar materials. One of the most significant benefits is the ability to handle sugar in a closed system, which helps maintain hygiene and prevents contamination from external sources. This is particularly important in food processing industries where product quality and safety are paramount. Additionally, pneumatic systems are more flexible in terms of layout, as they can be installed in various configurations, including vertical, horizontal, or inclined lines, to suit the specific layout of a facility. They also require less space compared to traditional conveyors, making them ideal for facilities with limited floor space. Furthermore, pneumatic conveying can reduce product degradation by minimizing friction and impact during transport, which is crucial for maintaining the quality of sugar products. The systems are also more energy-efficient in some cases, as they can optimize air pressure and flow rates to match the material handling requirements, leading to lower operational costs over time.
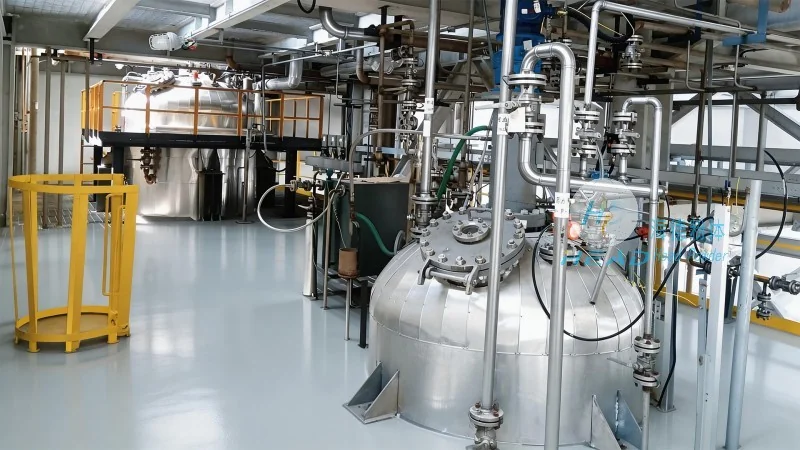
HeadPowder Engineering Co., Ltd. understands that each sugar processing facility has unique requirements. Therefore, they offer customized pneumatic conveying solutions tailored to specific needs. Whether a facility needs to handle a small volume of specialty sugars or a large-scale production of raw sugar, the company can design a system that meets the exact specifications. The systems can be scaled up or down to accommodate changes in production capacity, and they can be integrated with existing equipment or processes without major disruptions. This flexibility ensures that clients can adapt to changing market demands or production needs without the need for extensive system overhauls. The company also provides ongoing support and maintenance services to ensure the longevity and optimal performance of the conveying systems, providing peace of mind to their clients.
In conclusion, pneumatic conveying systems for sugar materials represent a sophisticated and efficient solution for material handling in the sugar industry. By leveraging the principles of fluid dynamics and utilizing advanced components, these systems offer numerous benefits, including improved hygiene, flexibility, and product quality. As a leading provider in the field, HeadPowder Engineering Co., Ltd. continues to innovate and provide tailored solutions that meet the evolving needs of the sugar industry, ensuring that their clients can operate efficiently and maintain high standards of product quality. The adoption of such systems not only enhances operational efficiency but also contributes to the overall sustainability and competitiveness of sugar processing facilities.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top