Understanding the working principle and characteristics of dilute phase pneumatic conveying is crucial for industries that rely on efficient material handling solutions. This article, presented by Shandong HeadPowder Engineering Co., Ltd. (headpowder), provides an in-depth look at how dilute phase systems operate and the key attributes that define their performance. With operations based in Shandong, China, headpowder specializes in providing advanced material handling solutions tailored to the needs of various industrial sectors.
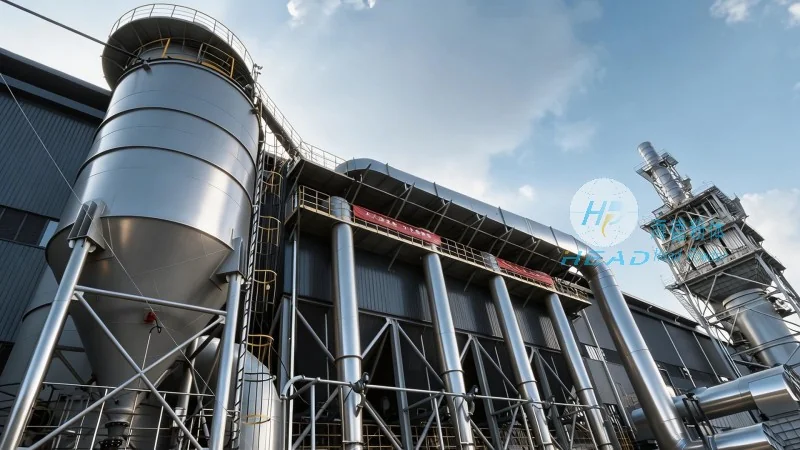
Dilute phase pneumatic conveying systems utilize a high-velocity air stream to transport particulate materials through a pipeline. The process begins with the material being fed into a hopper or feeder, where it is then introduced into the conveying line. As the air flows at a velocity sufficient to overcome the gravitational and frictional forces acting on the particles, the material becomes suspended in the air stream and is carried to the destination point. This method is particularly effective for transporting materials over moderate distances, typically ranging from several hundred meters to a few kilometers. The key components of a dilute phase system include the feeder, the conveying line, the air source (usually a blower or compressor), and the receiver where the material is deposited. The air velocity is maintained at a level that ensures the particles remain in suspension, preventing settling or blockages in the pipeline. This principle allows for a continuous, low-maintenance operation that is well-suited for various industrial applications.
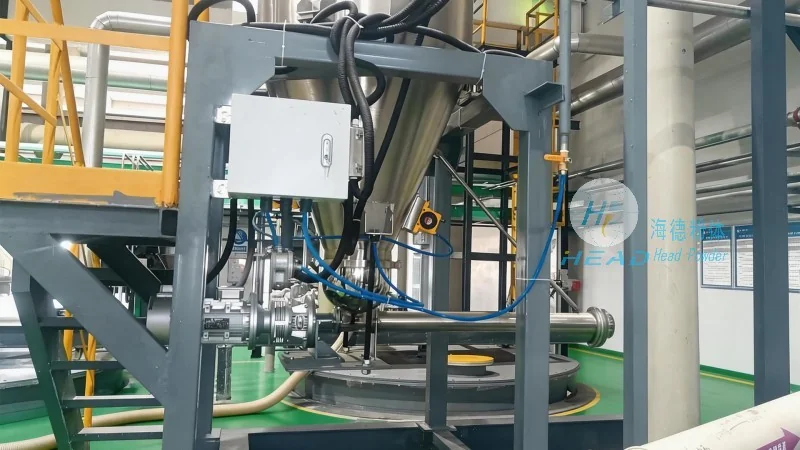
Several distinct characteristics define dilute phase pneumatic conveying systems, making them a preferred choice in many industries. First, the system operates with a relatively low pressure, typically ranging from 0.5 to 2 bar, which reduces the risk of equipment damage and simplifies the overall design. This lower pressure requirement also translates to lower energy consumption compared to dense phase systems, making it more cost-effective for certain applications. Second, the high air velocity ensures that the material is fully suspended, minimizing the risk of particle agglomeration or blockages that can occur in other conveying methods. This characteristic is particularly beneficial for handling fine or abrasive materials, as it prevents wear and tear on the pipeline and associated components. Third, dilute phase systems offer excellent flexibility in terms of material handling. They can transport a wide variety of particulate materials, including powders, granules, and small pellets, without the need for significant modifications to the system. This versatility makes them suitable for diverse industrial processes, from pharmaceuticals to food processing. Fourth, the system provides a clean and dust-free operation, as the material is enclosed within the pipeline and the air stream is filtered to remove any particulate matter. This feature is critical for industries where product contamination or environmental regulations are a concern. Finally, dilute phase pneumatic conveying allows for a continuous and automated operation, reducing the need for manual intervention and improving overall productivity. The system can be integrated with other process equipment, such as mixers or reactors, to create a seamless material handling workflow.
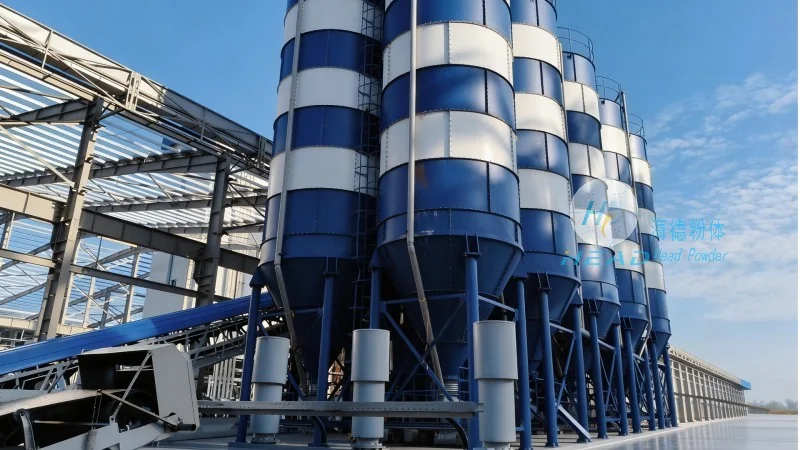
The advantages of dilute phase pneumatic conveying make it an ideal solution for a wide range of industrial applications. In the chemical industry, for example, dilute phase systems are used to transport powders and granules between processing units, ensuring a consistent and efficient flow of materials. The low pressure and high velocity characteristics of the system help maintain the quality of the materials, preventing degradation or contamination. In the food and beverage industry, dilute phase conveying is commonly used to handle ingredients such as flour, sugar, and spices. The clean and dust-free operation of the system ensures that the final products meet strict quality and safety standards. The pharmaceutical industry also benefits from dilute phase pneumatic conveying, as it allows for the transport of active pharmaceutical ingredients (APIs) and other sensitive materials without the risk of cross-contamination. The system's ability to maintain a sterile environment and prevent particle agglomeration is particularly important in this sector. Additionally, the system's low energy consumption and low maintenance requirements make it a cost-effective solution for industries looking to optimize their material handling processes. By reducing downtime and improving overall efficiency, dilute phase pneumatic conveying helps companies save on operational costs and increase their profitability.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top