Camellia seed material conveying lines are essential equipment in the processing industry, particularly for enterprises engaged in the processing of camellia seeds. These systems are designed to efficiently transport camellia seeds from one processing stage to another, ensuring smooth workflow and optimal operational efficiency. The following sections will delve into the working principle and key features of such conveying lines, providing a comprehensive understanding of their functionality and benefits.
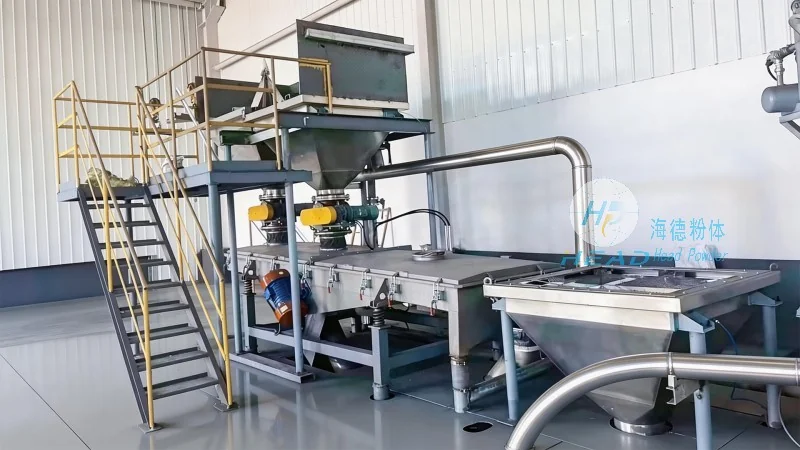
The core working principle of camellia seed material conveying lines revolves around the integration of various mechanical components and control systems to achieve continuous material transport. Typically, these systems start with the intake of raw camellia seeds, which are then fed into the primary processing units. The conveying mechanism, often utilizing screw conveyors, belt conveyors, or pneumatic systems, moves the seeds through different stages such as cleaning, sorting, and crushing. Each component is synchronized by a control system that monitors flow rates, pressure, and other critical parameters to maintain consistent performance. The entire process is automated, reducing manual intervention and enhancing operational reliability. For instance, the screw conveyor, a common component, uses rotating screws to push the seeds forward, while the belt conveyor utilizes a moving belt to transport larger quantities of material over longer distances. Pneumatic conveying systems, on the other hand, employ air pressure to move seeds through pipes, which is particularly effective for handling fine or dusty materials. The combination of these technologies ensures that camellia seeds are transported safely and efficiently, minimizing material loss and degradation.
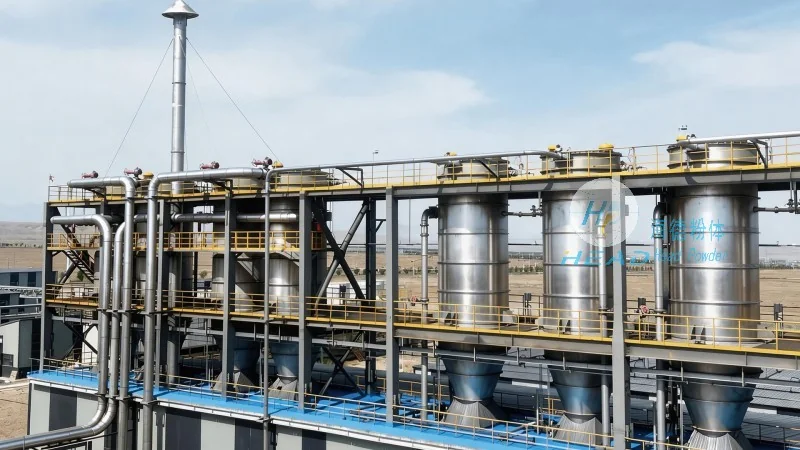
Camellia seed material conveying lines are characterized by several key features that enhance their performance and adaptability in industrial settings. Firstly, they are designed for high efficiency, with the ability to handle large volumes of camellia seeds at a consistent rate. This is achieved through optimized conveyor speeds and capacity adjustments, which can be tailored to the specific processing needs of the enterprise. Secondly, these systems prioritize material integrity, employing gentle handling mechanisms to prevent damage to the seeds during transport. This is crucial for maintaining the quality of the final product, as damaged seeds can affect the oil extraction process and overall yield. Thirdly, the conveying lines are equipped with advanced monitoring and control systems, allowing operators to track real-time data such as flow rates, temperature, and pressure. This enables proactive maintenance and quick troubleshooting, reducing downtime and increasing overall productivity. Additionally, the modular design of these systems allows for easy integration with other processing equipment, such as cleaning machines, sorters, and crushers, creating a seamless production line. The modularity also facilitates scalability, enabling businesses to expand their processing capacity as demand grows. Furthermore, the materials used in the construction of the conveying components, such as stainless steel and corrosion-resistant alloys, ensure durability and longevity, even in harsh processing environments. These features collectively contribute to the reliability and effectiveness of camellia seed material conveying lines, making them a preferred choice for modern processing facilities.
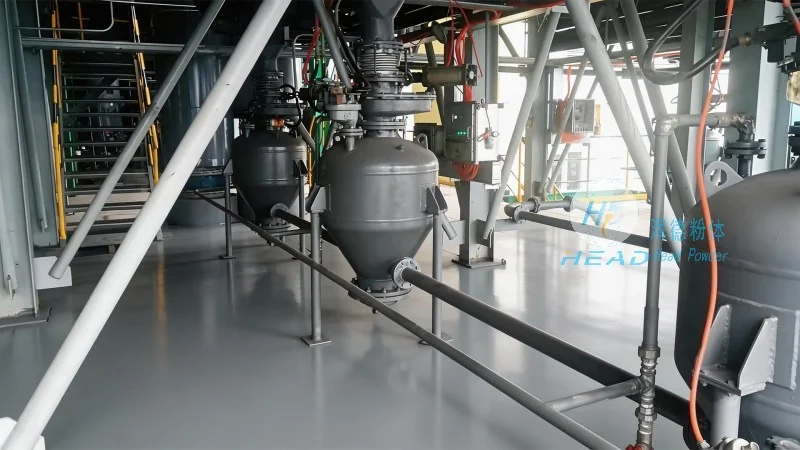
The application of camellia seed material conveying lines is widespread in the camellia seed processing industry, where they play a vital role in streamlining operations and improving product quality. By efficiently transporting raw materials through various processing stages, these systems help reduce processing time and labor costs. The consistent flow of seeds ensures that downstream equipment operates at optimal capacity, minimizing bottlenecks and enhancing overall throughput. Moreover, the gentle handling of seeds preserves their natural properties, leading to higher oil yields and better product quality. This is particularly important for enterprises that aim to produce high-quality camellia oil, as the quality of the raw material directly impacts the final product's purity and nutritional value. The advanced control systems also contribute to energy efficiency, as they optimize power usage based on the volume of material being transported. This not only reduces operational costs but also aligns with sustainability goals by minimizing energy consumption. In addition, the modular design allows for flexibility in adapting to different processing requirements, such as handling varying seed sizes or processing different batches. This adaptability makes the conveying lines suitable for both small-scale and large-scale processing operations. Overall, the benefits of camellia seed material conveying lines extend beyond mere material transport, contributing to improved operational efficiency, product quality, and cost-effectiveness in camellia seed processing.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top