Activated carbon material conveying lines are essential equipment in industrial processes, particularly in the production and handling of activated carbon. These systems are designed to efficiently transport activated carbon, a critical adsorbent used in various applications such as water treatment, air purification, and chemical processing. The effectiveness of these conveying lines directly impacts the overall efficiency and quality of the production line.
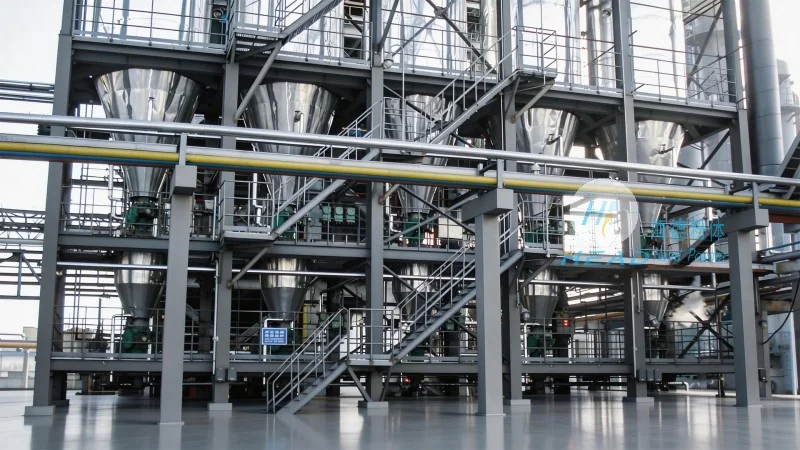
The operation of an activated carbon material conveying line typically involves several key components and mechanisms. The process begins with the loading of raw activated carbon into a hopper or storage silo. From there, the material is fed into a conveyor system, which may include screw conveyors, belt conveyors, or pneumatic conveying systems, depending on the specific requirements of the application. Screw conveyors are commonly used for horizontal or slight incline transport, while belt conveyors are suitable for longer distances and higher material volumes. Pneumatic conveying systems, on the other hand, use air pressure to move the material through pipes, which is ideal for dust-free and hygienic environments.
Once the material is conveyed to the processing or packaging area, it may undergo additional steps such as screening, drying, or blending. The conveying line ensures that the activated carbon is moved in a controlled manner, minimizing material loss and ensuring consistent flow rates. The system is often equipped with sensors and control panels to monitor the flow and adjust the speed or pressure as needed, maintaining optimal performance throughout the operation.
Activated carbon material conveying lines are characterized by several notable features that enhance their functionality and reliability. One of the primary features is their ability to handle abrasive and fine materials without causing excessive wear or blockages. The design of the conveying components, such as the screw flights or belt material, is tailored to withstand the mechanical stress of activated carbon, which can be hard and prone to dust generation. Additionally, these systems are often equipped with dust suppression mechanisms, such as enclosed conveyor housings and air filtration systems, to maintain a clean and safe working environment.
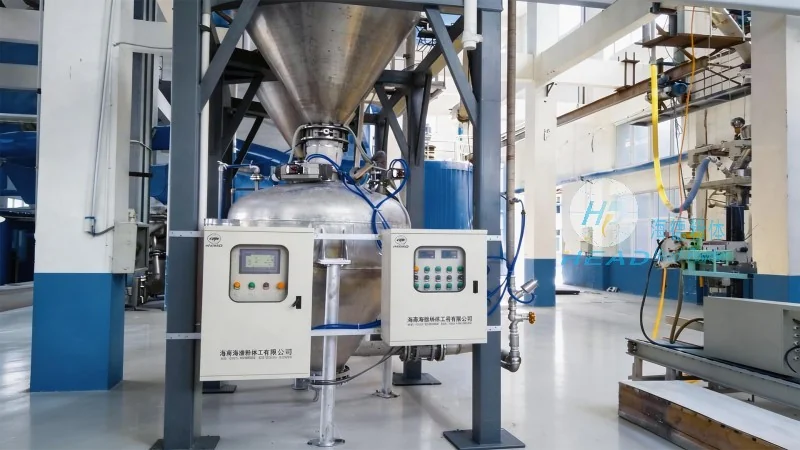
Another important feature is the flexibility and adaptability of the conveying lines. They can be customized to accommodate different particle sizes and moisture contents of the activated carbon, making them suitable for a wide range of industrial applications. The modular design allows for easy integration with existing production lines and future expansion, providing a cost-effective solution for manufacturers. Furthermore, the systems are designed for low maintenance, with easy access to components for inspection and replacement, reducing downtime and operational costs.
Implementing an activated carbon material conveying line offers several advantages for industrial operations. Firstly, it improves the efficiency of material handling by automating the transport process, reducing the need for manual labor and minimizing the risk of human error. The consistent flow of activated carbon ensures that production processes run smoothly, leading to higher output and better product quality. Secondly, the systems enhance safety by minimizing exposure to dust and other airborne particles, which can be hazardous to workers. The enclosed design and filtration systems help maintain a healthy working environment, complying with occupational health and safety regulations.
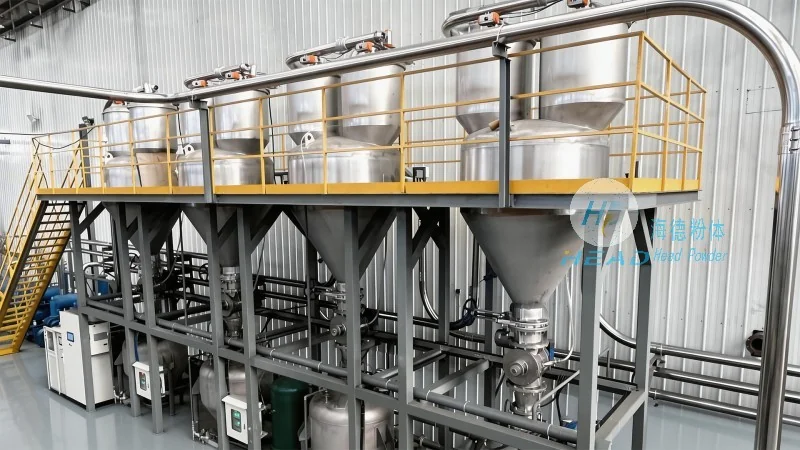
Thirdly, the conveying lines contribute to cost savings by reducing material waste and optimizing the use of resources. By ensuring that the activated carbon is transported without spillage or loss, manufacturers can lower their operational costs and improve their bottom line. Additionally, the energy-efficient design of modern conveying systems helps reduce electricity consumption, further contributing to cost savings and environmental sustainability.
Activated carbon material conveying lines are widely used in various industries that rely on activated carbon for their processes. In the water treatment industry, these systems are used to transport activated carbon to filtration plants, where it is used to remove impurities and contaminants from water. In the air purification sector, the conveying lines deliver activated carbon to industrial air filters, helping to remove pollutants and odors from industrial exhaust. The chemical processing industry also utilizes these systems to transport activated carbon for use in chemical adsorption and separation processes. Additionally, in the pharmaceutical and food industries, the conveying lines ensure the safe and hygienic handling of activated carbon, which is used in filtration and purification processes.
Activated carbon material conveying lines are a critical component of modern industrial operations, providing efficient and reliable transport of activated carbon. The working principle and features of these systems are designed to meet the specific needs of various applications, ensuring optimal performance and safety. As a leading manufacturer in the field, Shandong HeadPowder Engineering Co., Ltd. specializes in providing high-quality conveying solutions tailored to the requirements of different industries. With a focus on innovation and customer satisfaction, the company offers customized solutions that enhance the efficiency and productivity of its clients' operations. The company's commitment to quality and reliability has made it a trusted partner for businesses worldwide, helping them achieve their production goals while maintaining safety and environmental standards.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top