The fertilizer granule material conveying line is a critical component in modern agricultural and chemical processing facilities. Designed to efficiently transport granular fertilizers from storage silos or production areas to processing units or packaging stations, this system ensures seamless material flow and operational efficiency. As a leading manufacturer in the industry, Shandong HeadPowder Engineering Co., Ltd. specializes in developing customized conveying solutions tailored to the specific needs of fertilizer manufacturers.
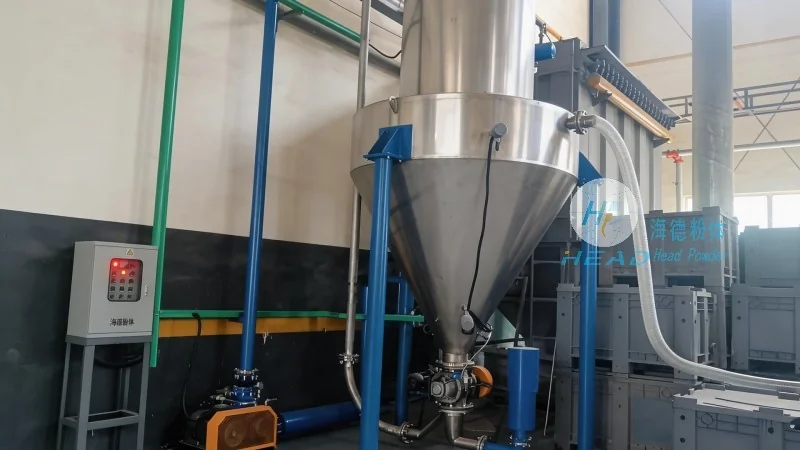
The core mechanism of the fertilizer granule material conveying line operates on principles of mechanical transport, typically utilizing screw conveyors, belt conveyors, or pneumatic systems. The process begins with the granular fertilizer being fed into the inlet of the conveyor system. Depending on the chosen technology, the material is then moved through a series of components, including hoppers, chutes, and drive mechanisms. For screw conveyors, a rotating helical screw pushes the granules forward, while belt conveyors rely on motor-driven belts to transport the material. Pneumatic systems, on the other hand, use compressed air to create a flow of air and fertilizer particles, enabling efficient transport over longer distances. The system is equipped with control panels that allow operators to monitor and adjust the speed and direction of material movement, ensuring precise and reliable operation.
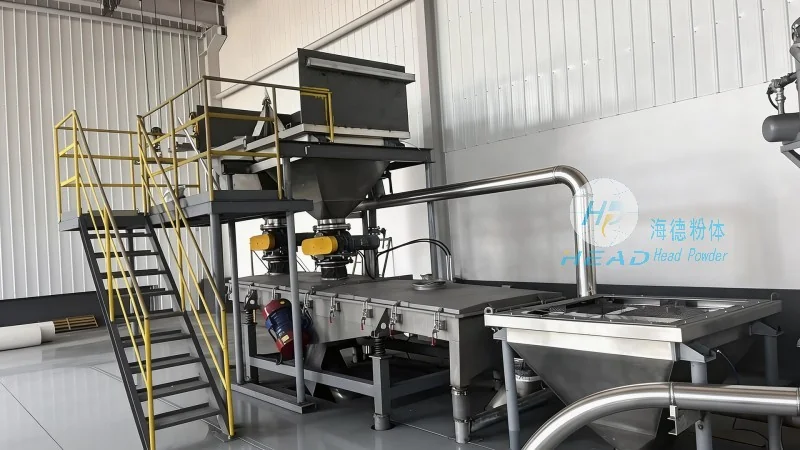
The fertilizer granule material conveying line from Shandong HeadPowder Engineering Co., Ltd. is engineered with several key features that enhance performance and durability. One of the primary advantages is its high efficiency in material handling, capable of transporting large volumes of granular fertilizer with minimal energy consumption. The system is also designed for low maintenance, featuring robust components that resist wear and tear from abrasive granules. Additionally, the conveying line is equipped with safety features, such as overload protection and emergency stop buttons, to ensure operational safety. The modular design allows for easy installation and integration into existing production lines, reducing downtime during setup. Another notable feature is the system's adaptability, which enables it to handle various types of granular fertilizers, including nitrogen, phosphorus, and potassium compounds, without compromising performance.
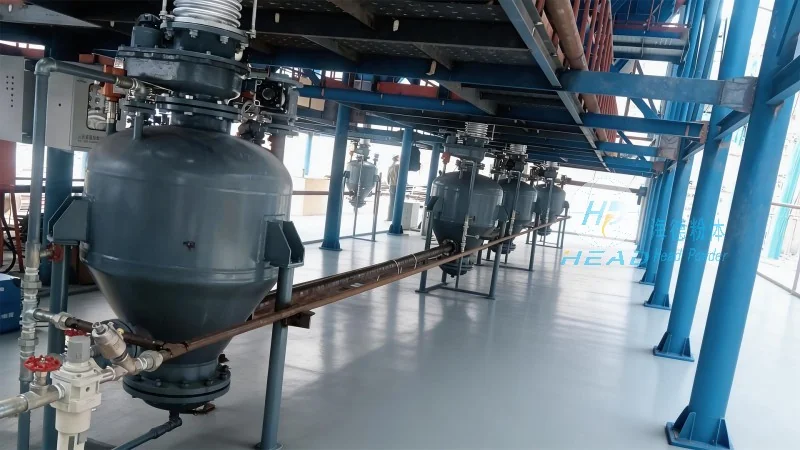
When designing the fertilizer granule material conveying line, several technical specifications and design considerations are critical to ensure optimal performance. The system's capacity is determined by factors such as the type of fertilizer, particle size, and required throughput. For example, a line designed for high-density nitrogen fertilizers may have a higher capacity than one for lighter, more porous materials. The conveyor's speed and power requirements are calculated based on the material's bulk density and the desired transport distance. The material of construction is also a key consideration, as it must withstand the corrosive and abrasive nature of fertilizers. Stainless steel or corrosion-resistant alloys are commonly used for components that come into direct contact with the material. The system's layout is optimized to minimize material degradation and ensure consistent product quality. Additionally, the design incorporates features like dust collection and sealing to prevent environmental contamination and maintain a clean working environment.
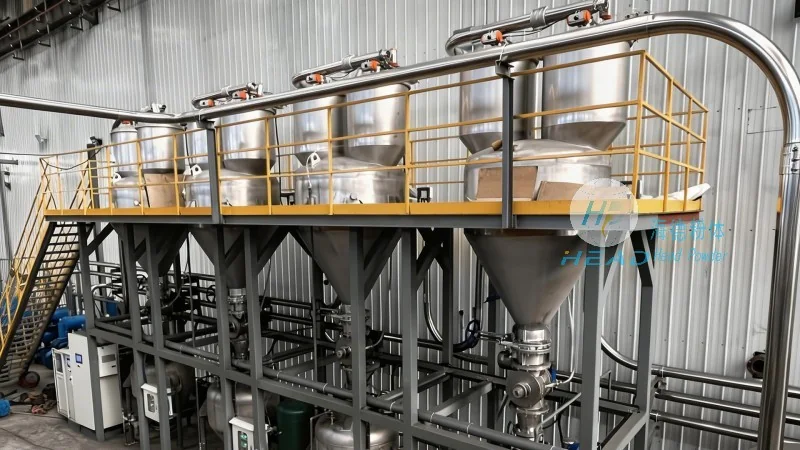
The fertilizer granule material conveying line finds extensive application in various sectors of the agricultural and chemical industries. In fertilizer production plants, it is used to transport raw materials from storage to processing units, ensuring a continuous supply of granules for manufacturing. In packaging facilities, the line efficiently moves finished granular fertilizers to packaging machines, streamlining the production process. The system is also utilized in bulk handling operations, where it facilitates the transfer of large quantities of fertilizer between storage silos and distribution centers. The impact of this technology on the industry is significant, as it improves operational efficiency, reduces labor costs, and enhances product quality. By providing a reliable and efficient means of material transport, the conveying line contributes to the overall productivity and competitiveness of fertilizer manufacturers. The system's adaptability and customization options allow it to meet the specific requirements of different production scales and operational environments, making it a versatile solution for modern fertilizer processing facilities.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top