Stone material conveying lines are essential in various industrial applications, particularly in the construction and mining sectors. These systems are designed to efficiently transport aggregates, such as gravel, crushed stone, and other bulk materials over long distances with minimal effort. The effectiveness of these lines directly impacts production efficiency and operational costs, making them a critical component in material handling processes.
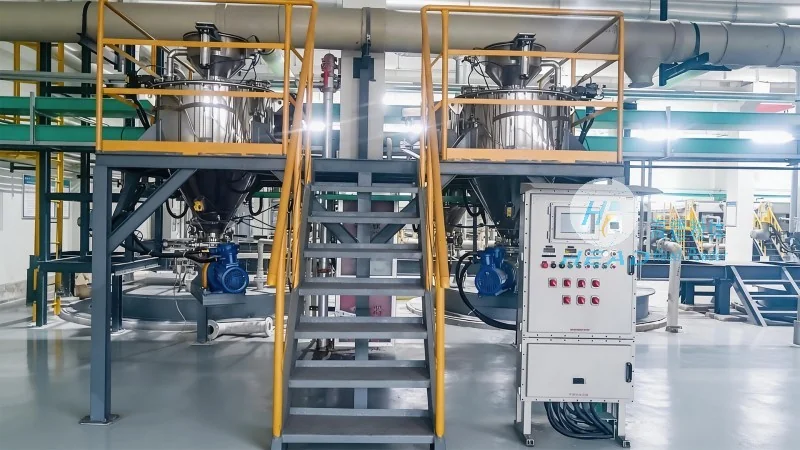
The core working principle of stone material conveying lines revolves around the use of mechanical components to move bulk materials from a loading point to a discharge point. Typically, these systems employ a combination of rollers, belts, or chains to transport the material. The process begins with the material being loaded into the conveyor at the inlet. As the conveyor belt or chain moves, the material is carried along the path, often elevated or inclined to facilitate movement. The speed and tension of the conveyor are carefully controlled to ensure smooth and consistent material flow. This mechanical operation eliminates the need for manual labor in transporting heavy and bulky stone materials, significantly enhancing operational efficiency.
Stone material conveying lines offer several key features that make them ideal for industrial use. First, they provide high throughput capacity, allowing for the continuous movement of large volumes of material. This is crucial in high-production environments where consistent material supply is necessary. Second, these systems are designed for durability and reliability, capable of handling abrasive stone materials without significant wear or breakdown. The robust construction, often made from heavy-duty materials like steel and reinforced components, ensures long service life and minimal maintenance. Third, the flexibility in design allows for customization based on the specific requirements of the application. Whether it's a horizontal or inclined setup, the conveying line can be adapted to fit the layout of the facility. Additionally, modern stone material conveying lines often incorporate advanced control systems that allow for real-time monitoring and adjustment of the conveying process, optimizing performance and reducing downtime.
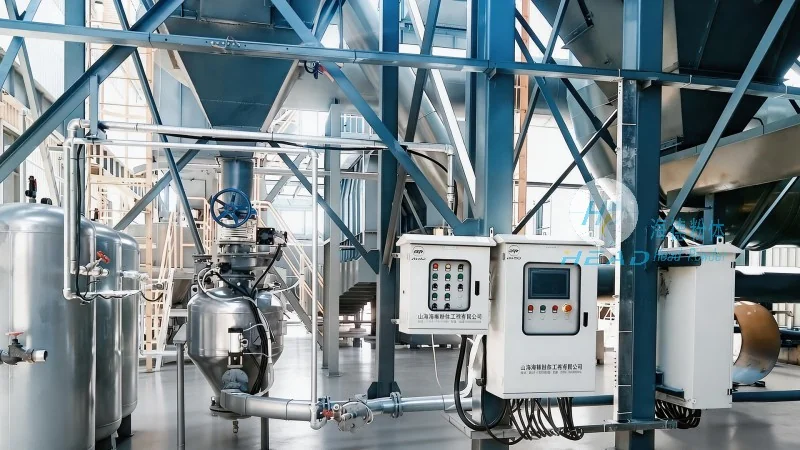
Stone material conveying lines are widely used in applications such as concrete production, road construction, and mining operations. In concrete plants, these systems efficiently transport aggregates from storage to mixing stations, ensuring a steady supply of raw materials. In road construction, they help move crushed stone and gravel to the construction site, supporting the laying of foundations and road surfaces. The benefits of using these conveying lines include reduced labor costs, improved safety by minimizing manual handling of heavy materials, and increased productivity due to consistent material flow. Furthermore, the ability to handle abrasive materials without frequent maintenance reduces operational expenses and enhances overall profitability for industrial operations.
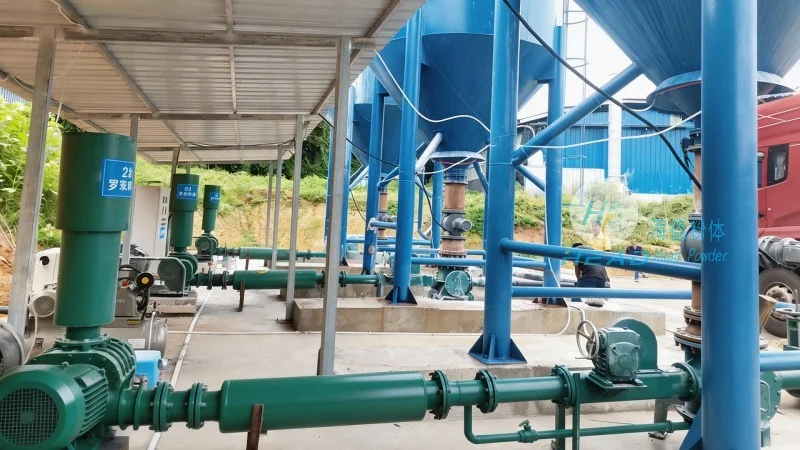
Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing customized stone material conveying lines tailored to the specific needs of clients. The company, known as HeadPowder, leverages advanced engineering and manufacturing capabilities to produce high-quality conveying systems. Their expertise in material handling solutions ensures that the conveying lines are not only efficient but also durable and reliable. The company's products are designed to integrate seamlessly with other industrial equipment, such as crushers, screens, and storage silos, creating a cohesive material handling system. This integration allows for a streamlined workflow, where materials move from one process to another without interruption. The customization options include different conveyor types (belt, chain, roller), material handling capacities, and dimensions, ensuring that the system meets the exact requirements of the application. HeadPowder's commitment to quality and customer satisfaction is reflected in their rigorous testing and quality control processes, which guarantee that each conveying line meets or exceeds industry standards.
Stone material conveying lines are indispensable in modern industrial operations, offering efficient and reliable solutions for transporting bulk materials. The working principle, which relies on mechanical movement, combined with key features like high capacity, durability, and flexibility, makes these systems a preferred choice for various applications. Companies like Shandong HeadPowder Engineering Co., Ltd. play a vital role in providing these essential equipment, ensuring that industrial processes run smoothly and efficiently. With their expertise in engineering and manufacturing, HeadPowder continues to deliver high-quality stone material conveying lines that meet the evolving needs of the industry.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top