Material conveying lines in dust collection stations are critical components of industrial dust control systems, designed to transport bulk materials efficiently while maintaining air quality and operational safety. These systems integrate with dust collection equipment to ensure that materials are moved from processing points to storage or further processing stages without releasing dust into the environment. Understanding the working principle and key features of such lines is essential for optimizing industrial operations and compliance with environmental regulations.
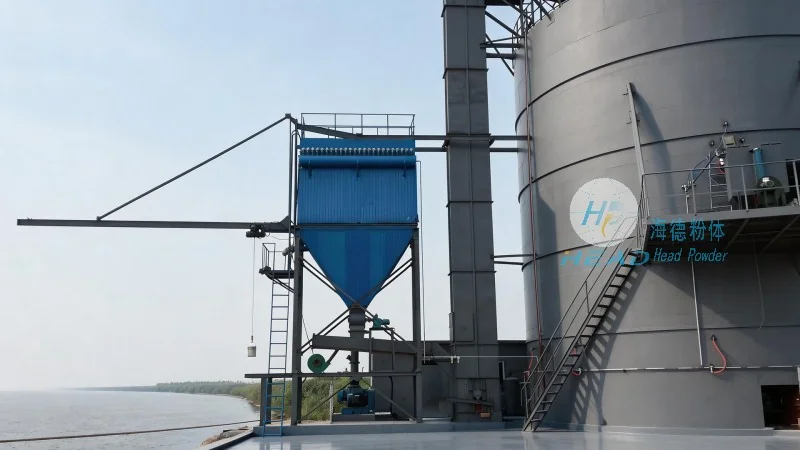
Shandong HeadPowder Engineering Co., Ltd., based in Shandong, China, specializes in the design, manufacturing, and installation of advanced material handling and dust control solutions. With a focus on precision engineering and customer-centric service, the company provides tailored conveying systems that meet the specific requirements of various industrial applications, including mining, cement production, and chemical processing.
The core working principle of material conveying lines in dust collection stations involves the integration of dust collection equipment with material handling mechanisms. Typically, the process begins with the material being collected from a processing point, such as a crusher or mixer, by a dust collector. The collected material is then transferred to a conveying system, which may include screw conveyors, belt conveyors, or pneumatic conveyors, depending on the material properties and operational conditions. The conveying system transports the material to a designated storage or processing location, while the dust collector simultaneously captures and filters airborne particles to maintain clean air in the facility. This integrated approach ensures that material handling and dust control are performed concurrently, enhancing overall operational efficiency and environmental compliance.
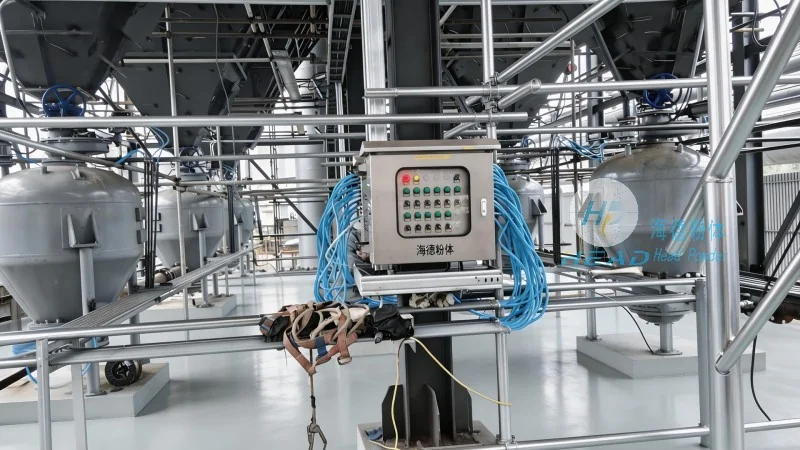
Material conveying lines in dust collection stations are characterized by several key features that enhance their performance and reliability. First, they are designed to operate in conjunction with dust collection systems, ensuring that dust is contained and filtered during material transport. This feature is crucial for maintaining air quality and preventing dust-related health hazards in industrial environments. Second, these lines often incorporate dust-tight seals and enclosed structures to minimize dust leakage and improve safety. Third, they are engineered to handle a wide range of material types, including powders, granules, and bulk solids, with adjustable speed and capacity settings to accommodate varying production demands. Additionally, many systems feature automated controls and monitoring capabilities, allowing for real-time adjustments and maintenance alerts to optimize performance and reduce downtime. The robust construction and corrosion-resistant materials used in these lines further enhance their durability and longevity, making them suitable for long-term industrial use.
Implementing material conveying lines in dust collection stations offers several significant advantages for industrial operations. One of the primary benefits is the reduction of dust emissions, which not only improves air quality but also helps companies comply with environmental regulations and avoid penalties. By containing dust within the system, these lines minimize the risk of dust-related accidents and health issues among workers. Another advantage is the increased efficiency in material handling, as the integrated system allows for seamless transfer of materials from one stage to another without manual intervention. This automation reduces labor costs and improves production throughput. Furthermore, the enclosed design of these lines prevents material spillage and contamination, maintaining product quality and reducing waste. The flexibility of these systems also allows for easy integration with existing dust collection equipment, making them a cost-effective solution for upgrading or expanding industrial facilities.
Material conveying lines in dust collection stations are widely used across various industries that handle bulk materials and generate dust. Common applications include the mining industry, where they transport ore and rock from crushing and grinding operations to storage or processing facilities. In the cement industry, these lines are used to convey raw materials, clinker, and finished cement products, ensuring efficient production and dust control. The chemical industry also benefits from these systems, as they handle powders and granules during mixing, processing, and packaging stages. Additionally, in the food and pharmaceutical industries, specialized conveying lines are used to transport raw materials and finished products while maintaining strict hygiene standards and preventing contamination.
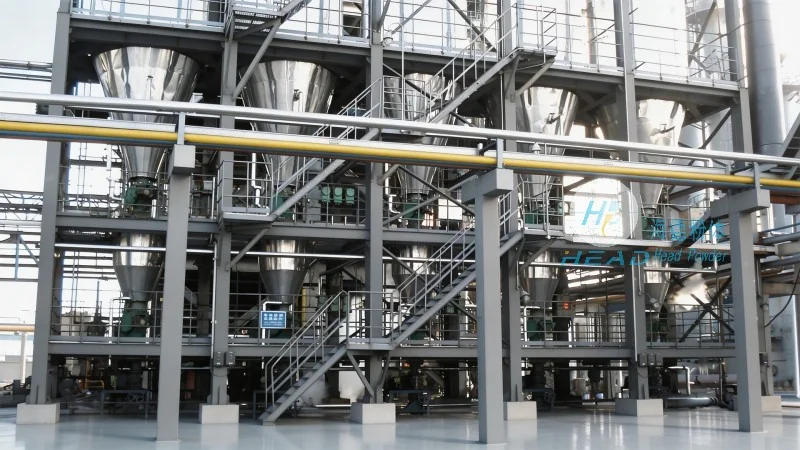
Proper maintenance is essential to ensure the optimal performance and longevity of material conveying lines in dust collection stations. Regular inspections should be conducted to check for wear and tear on components such as belts, screws, and seals. Lubrication of moving parts is crucial to prevent friction and reduce the risk of breakdowns. Cleaning of dust collection filters and conveying components is also necessary to maintain efficiency and prevent clogging. Operational considerations include monitoring system performance, such as conveyor speed and material flow, to detect any abnormalities early. Additionally, training operators on proper system operation and safety procedures is vital to prevent accidents and ensure smooth operation. By adhering to regular maintenance schedules and operational guidelines, companies can maximize the lifespan of their conveying lines and minimize downtime.
Material conveying lines in dust collection stations are sophisticated systems that play a vital role in modern industrial operations. By integrating dust control with material handling, these lines enhance efficiency, improve safety, and ensure compliance with environmental regulations. The working principle and key features of such systems, as explained above, highlight their importance in various industries. With advancements in technology, these systems continue to evolve, offering more efficient and sustainable solutions for material transport and dust management. For companies seeking reliable and effective conveying solutions, Shandong HeadPowder Engineering Co., Ltd. provides expert design and implementation services to meet their specific needs.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top